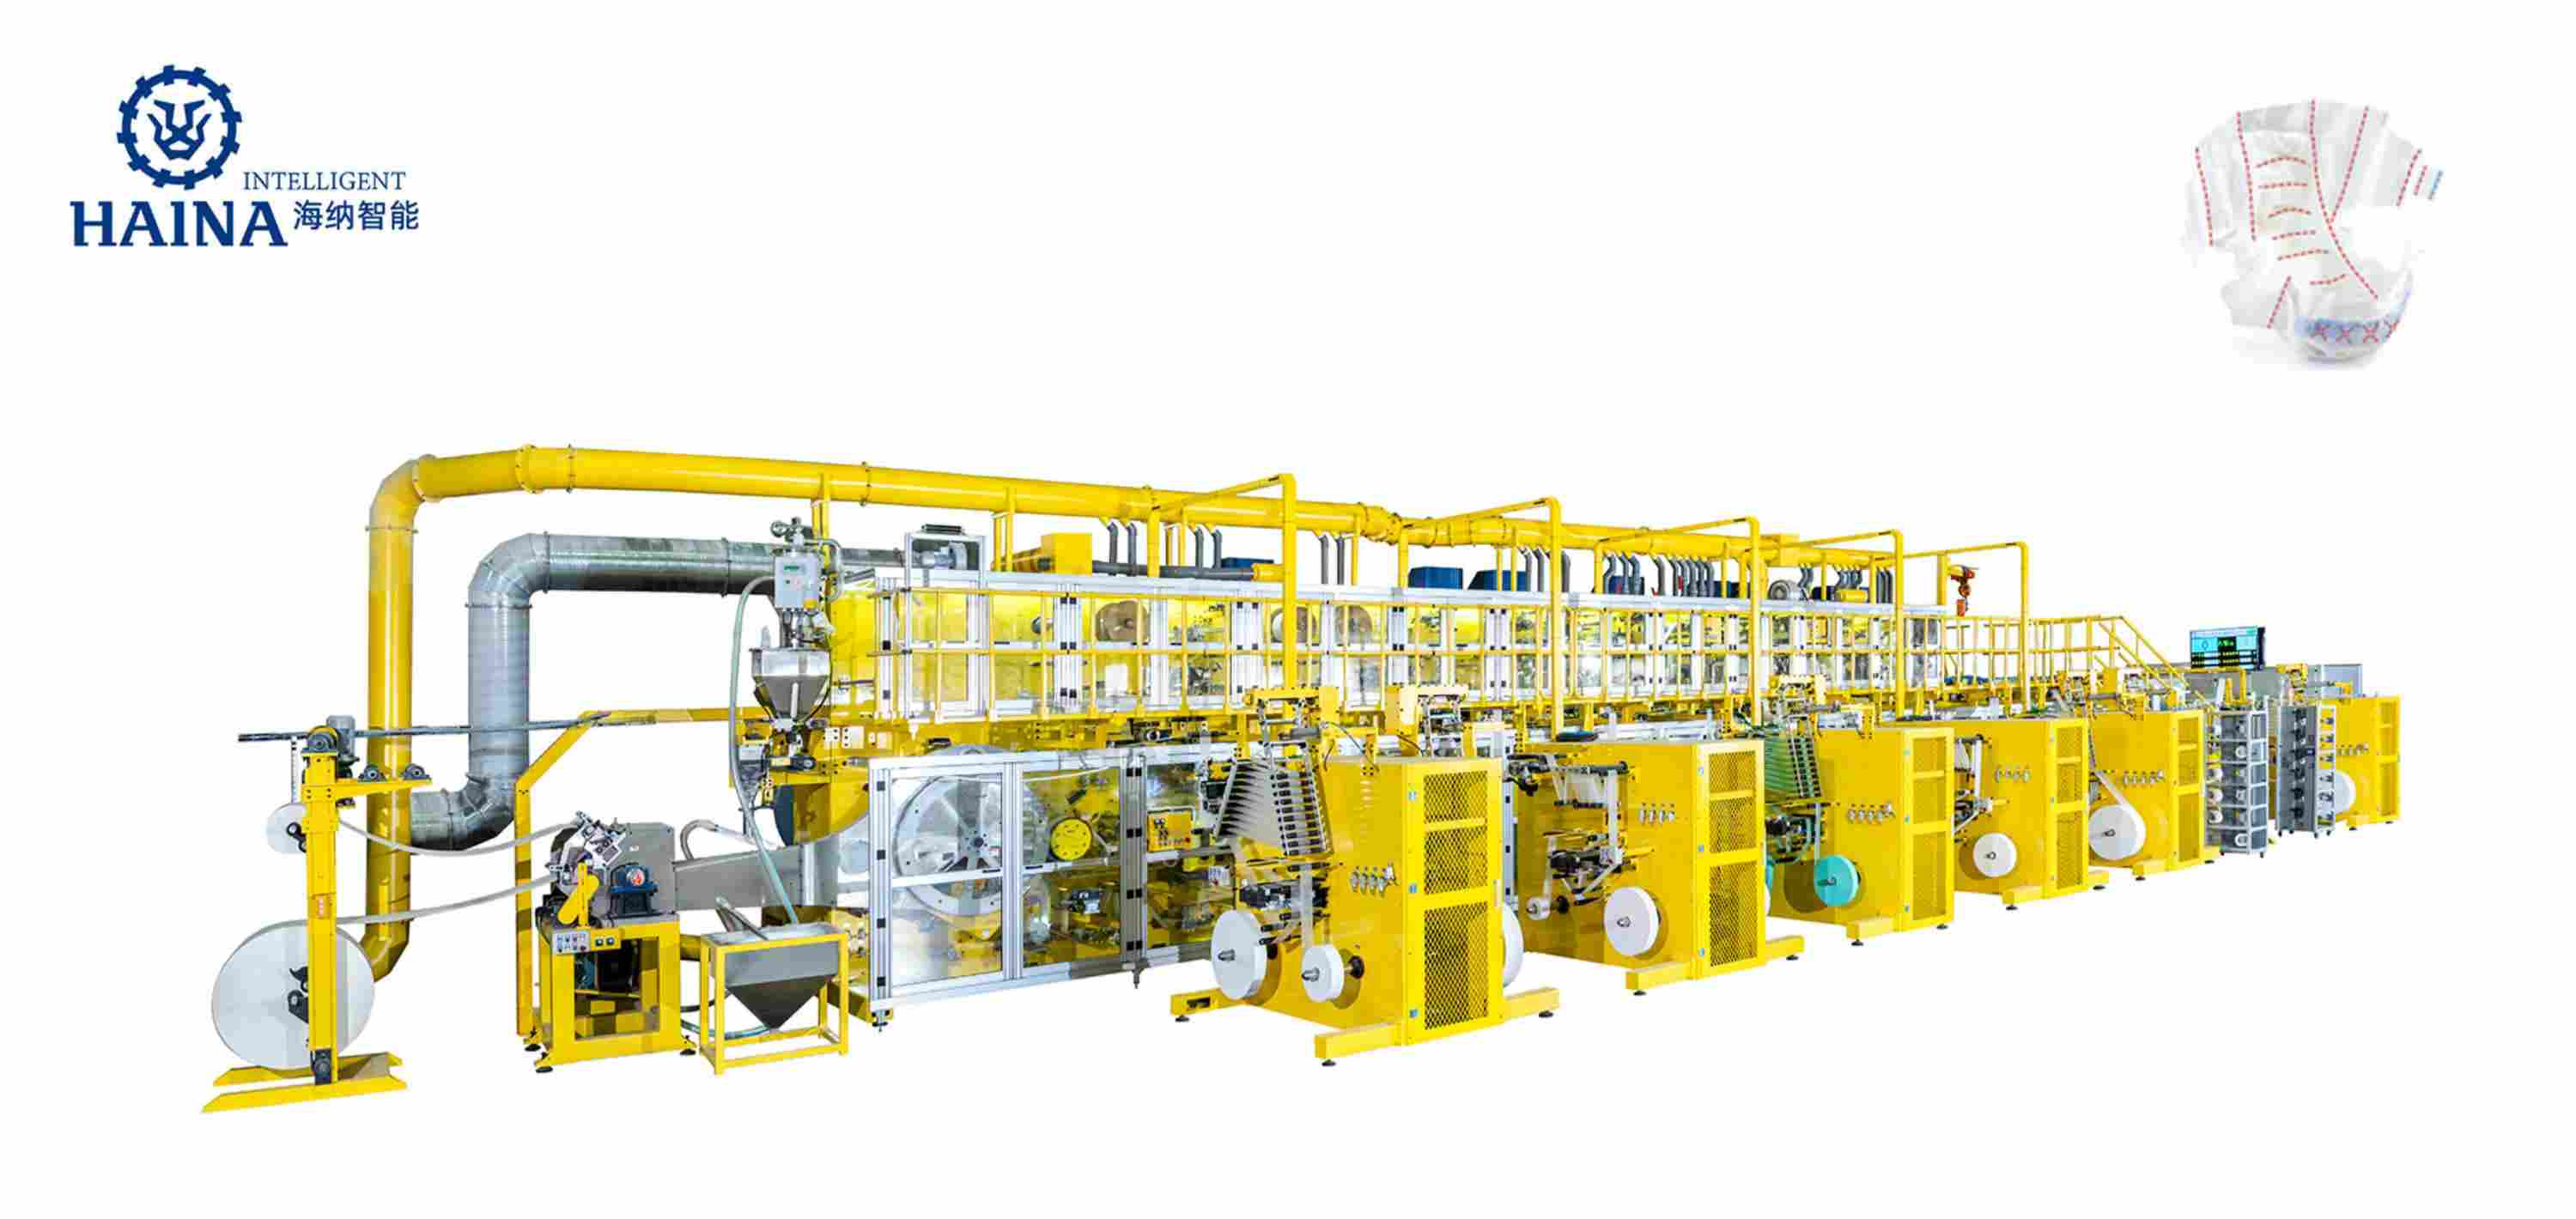
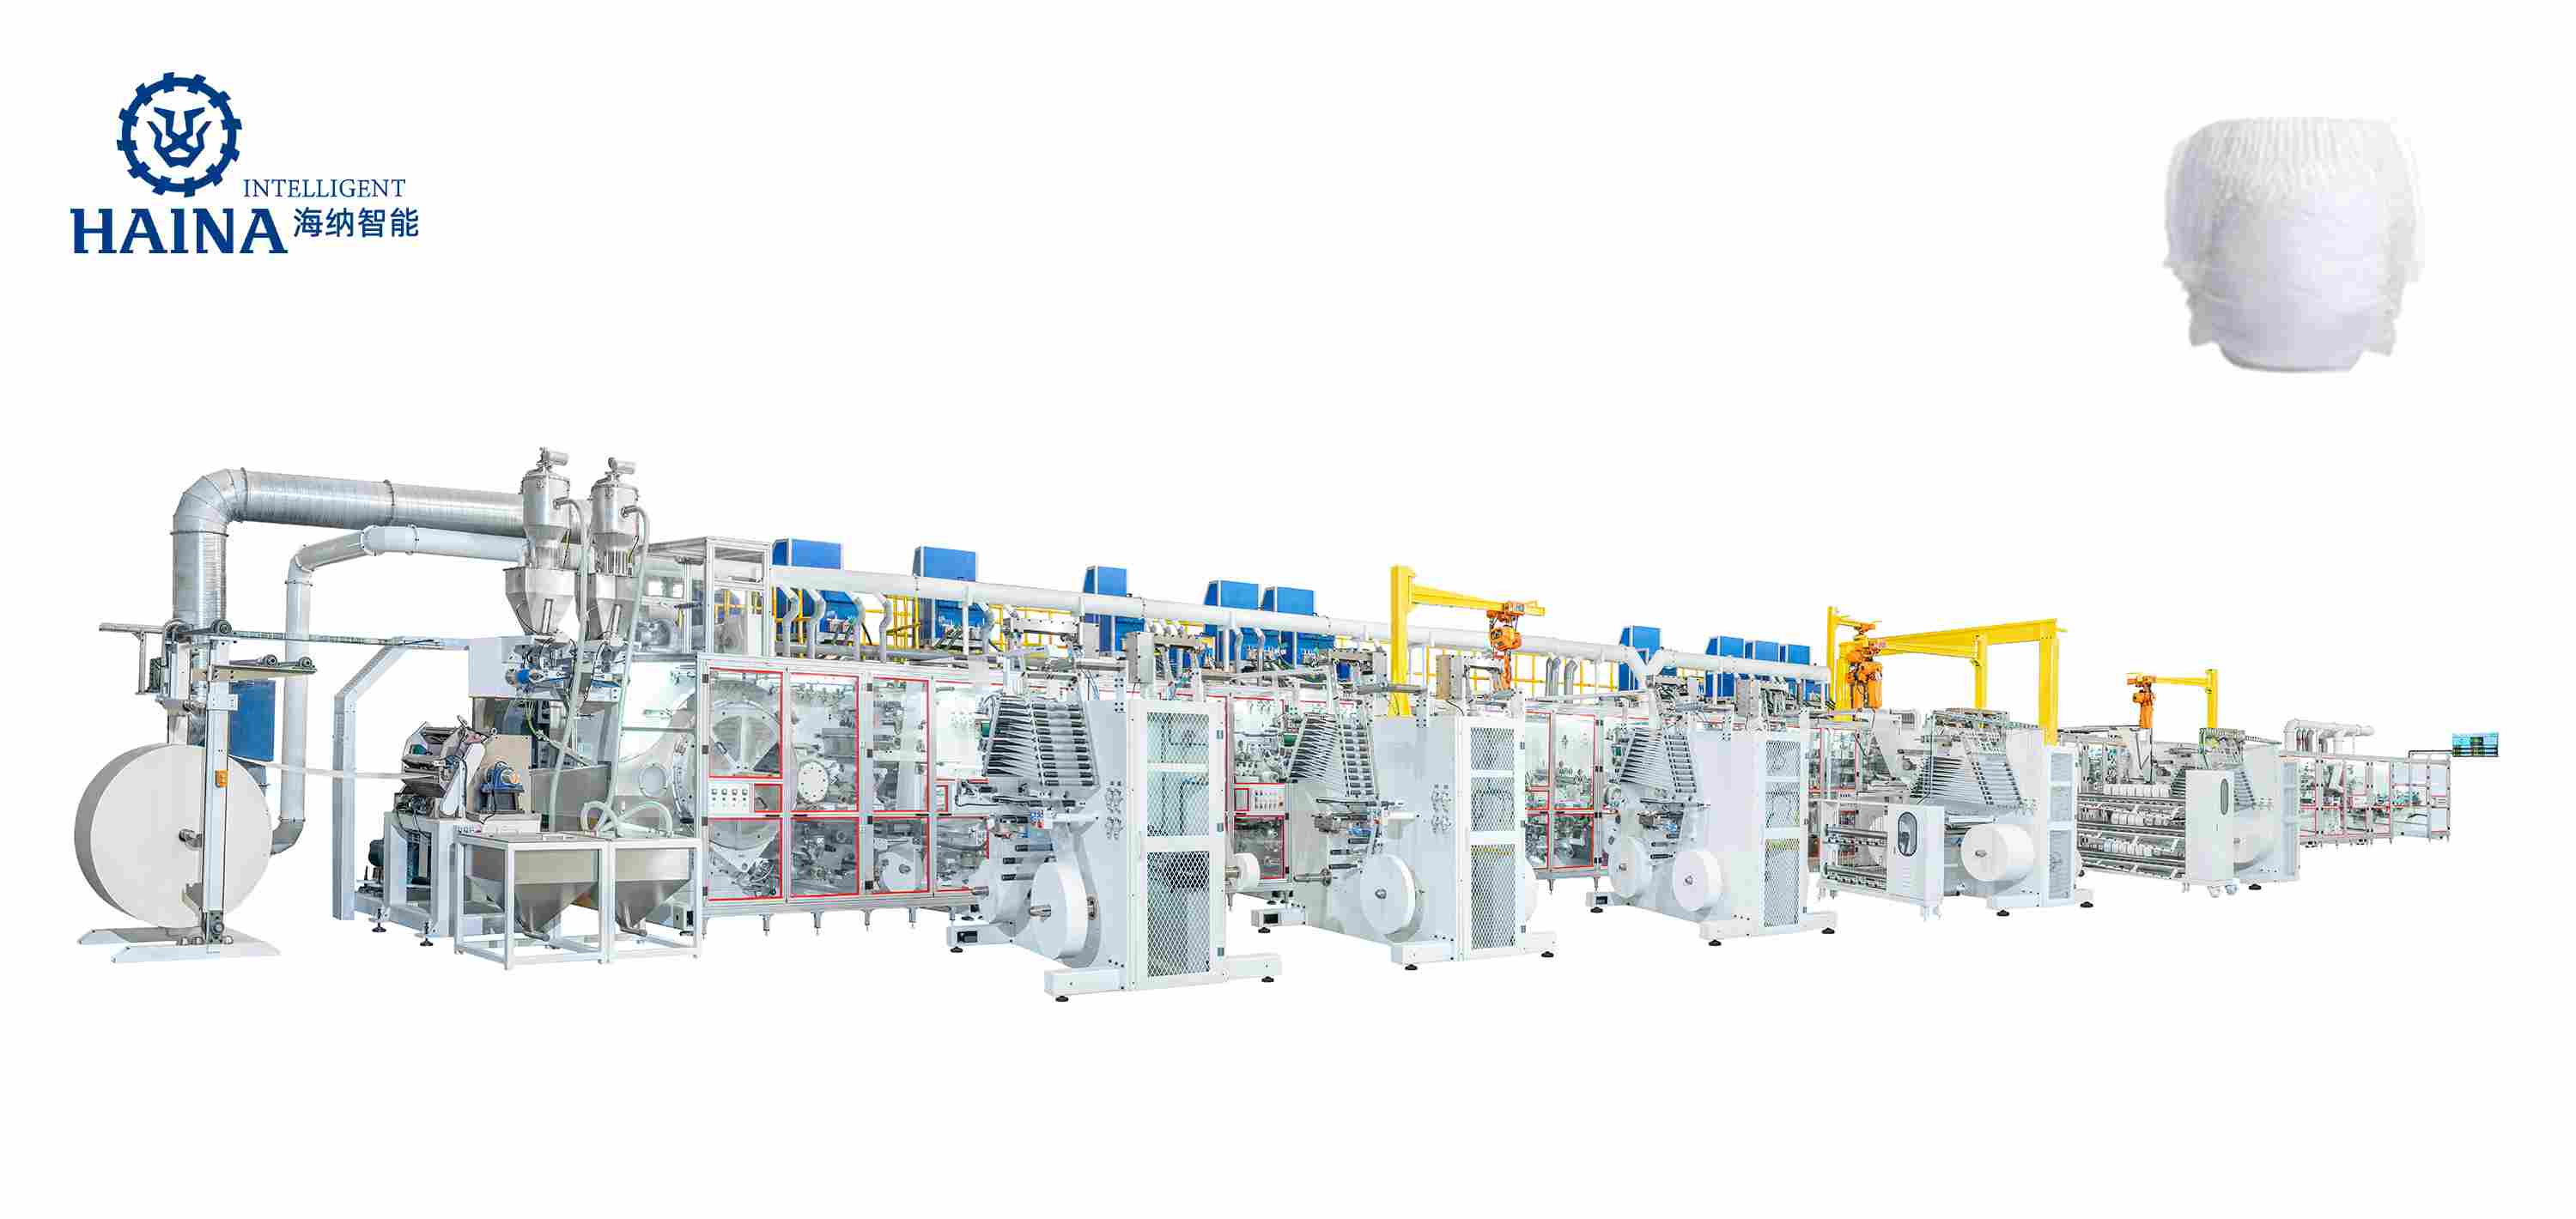
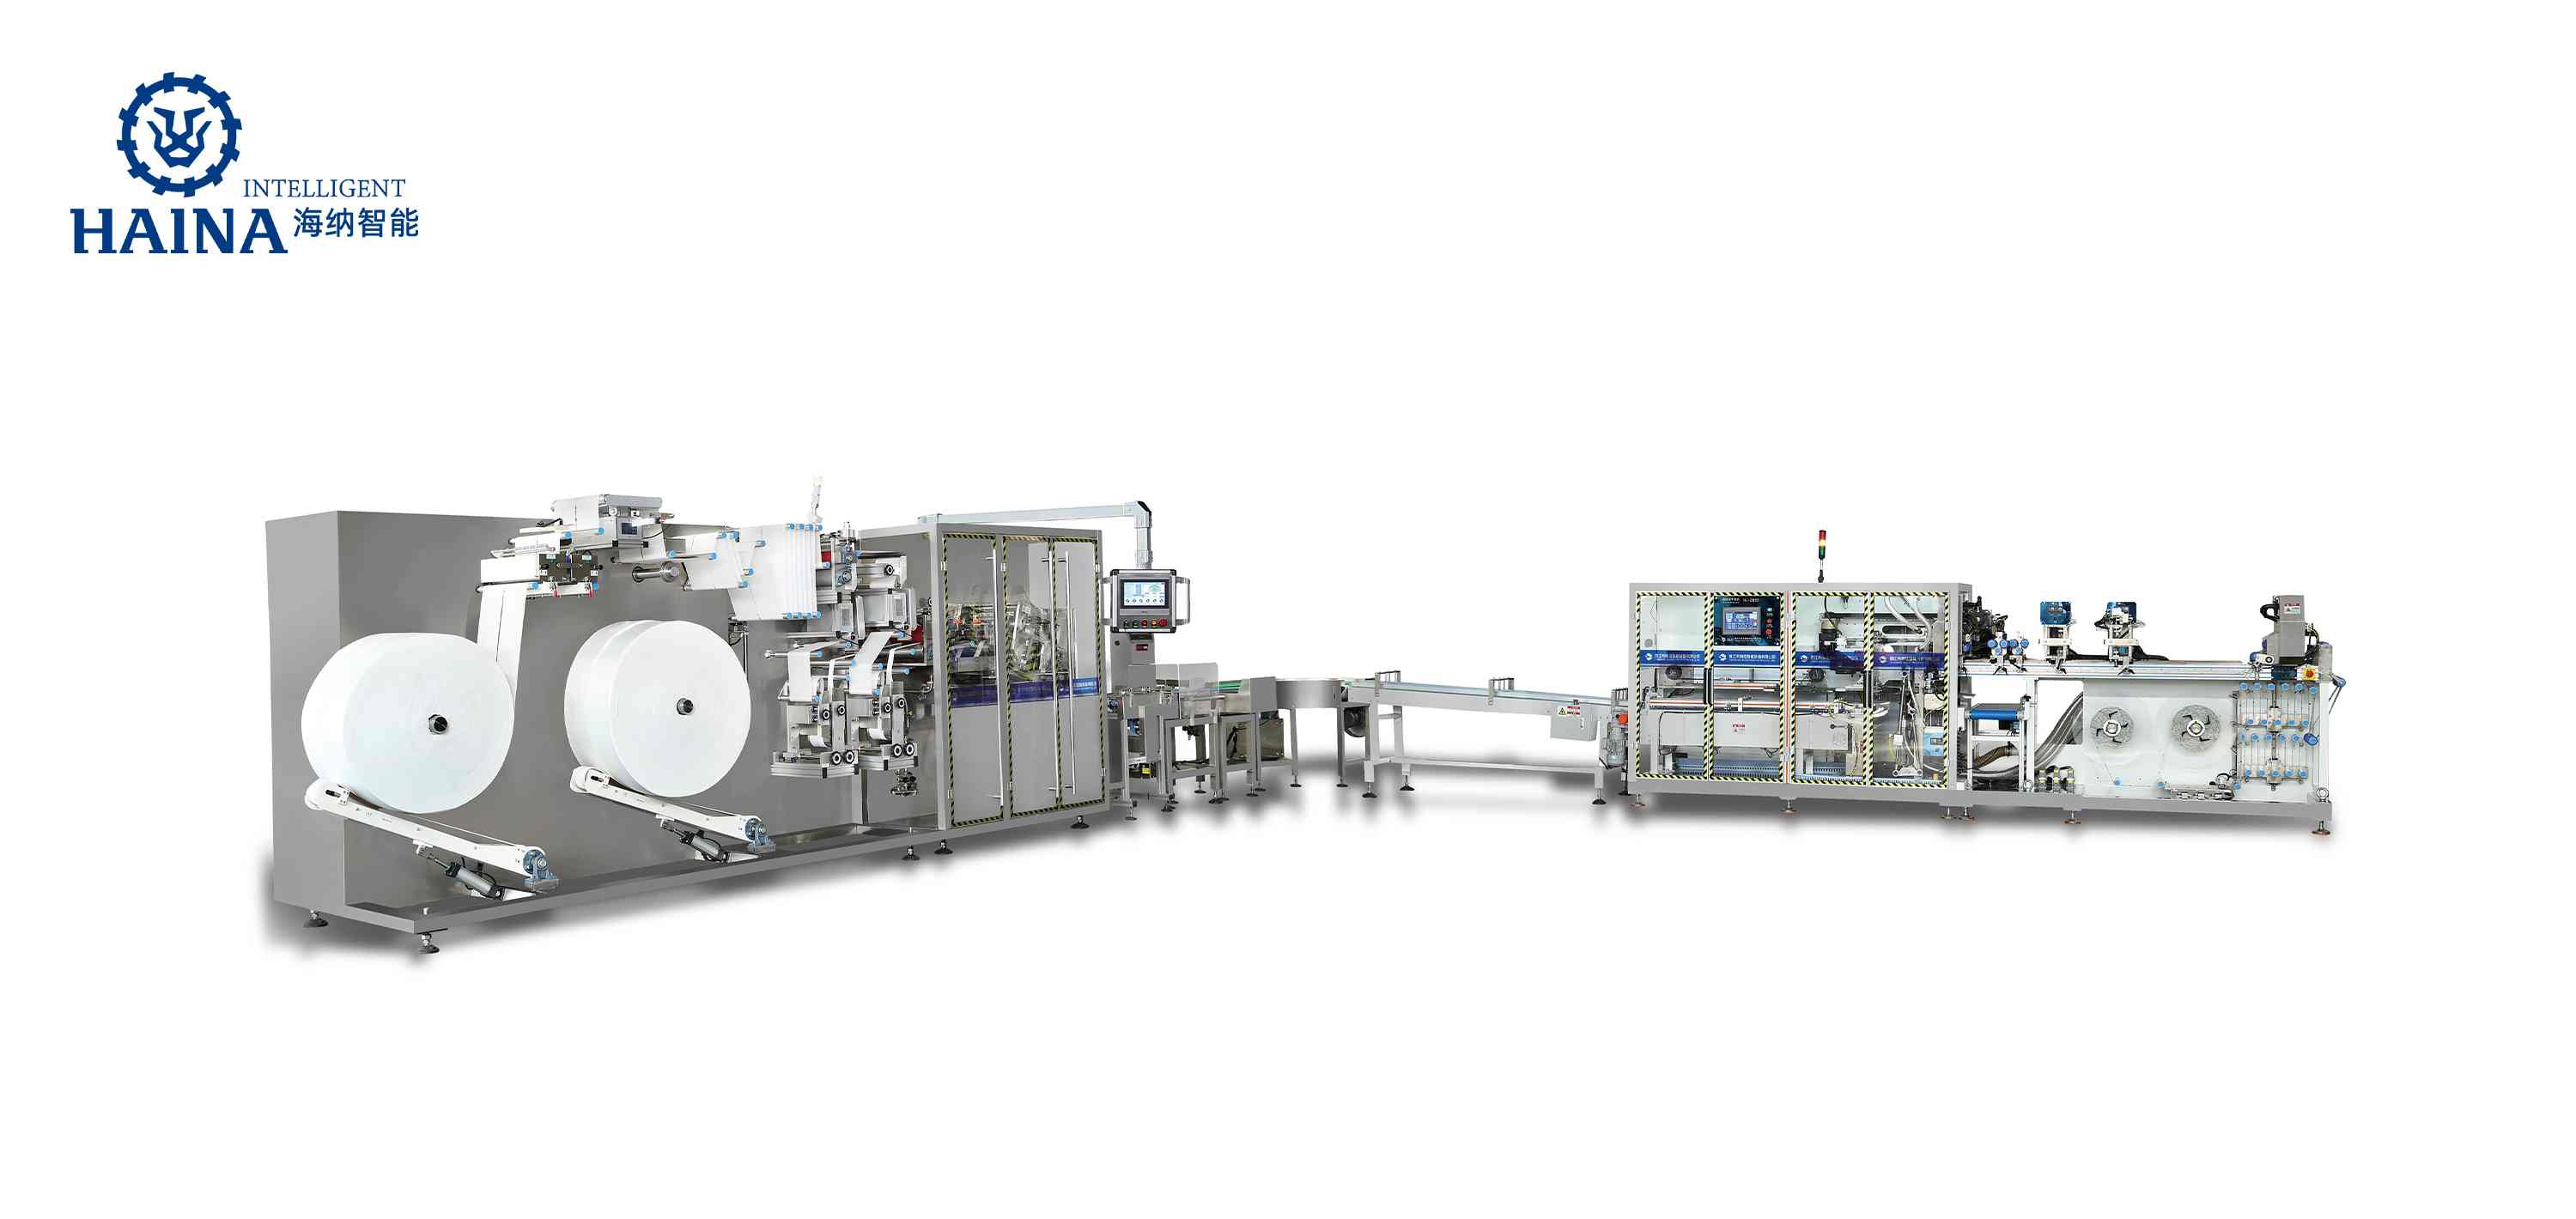
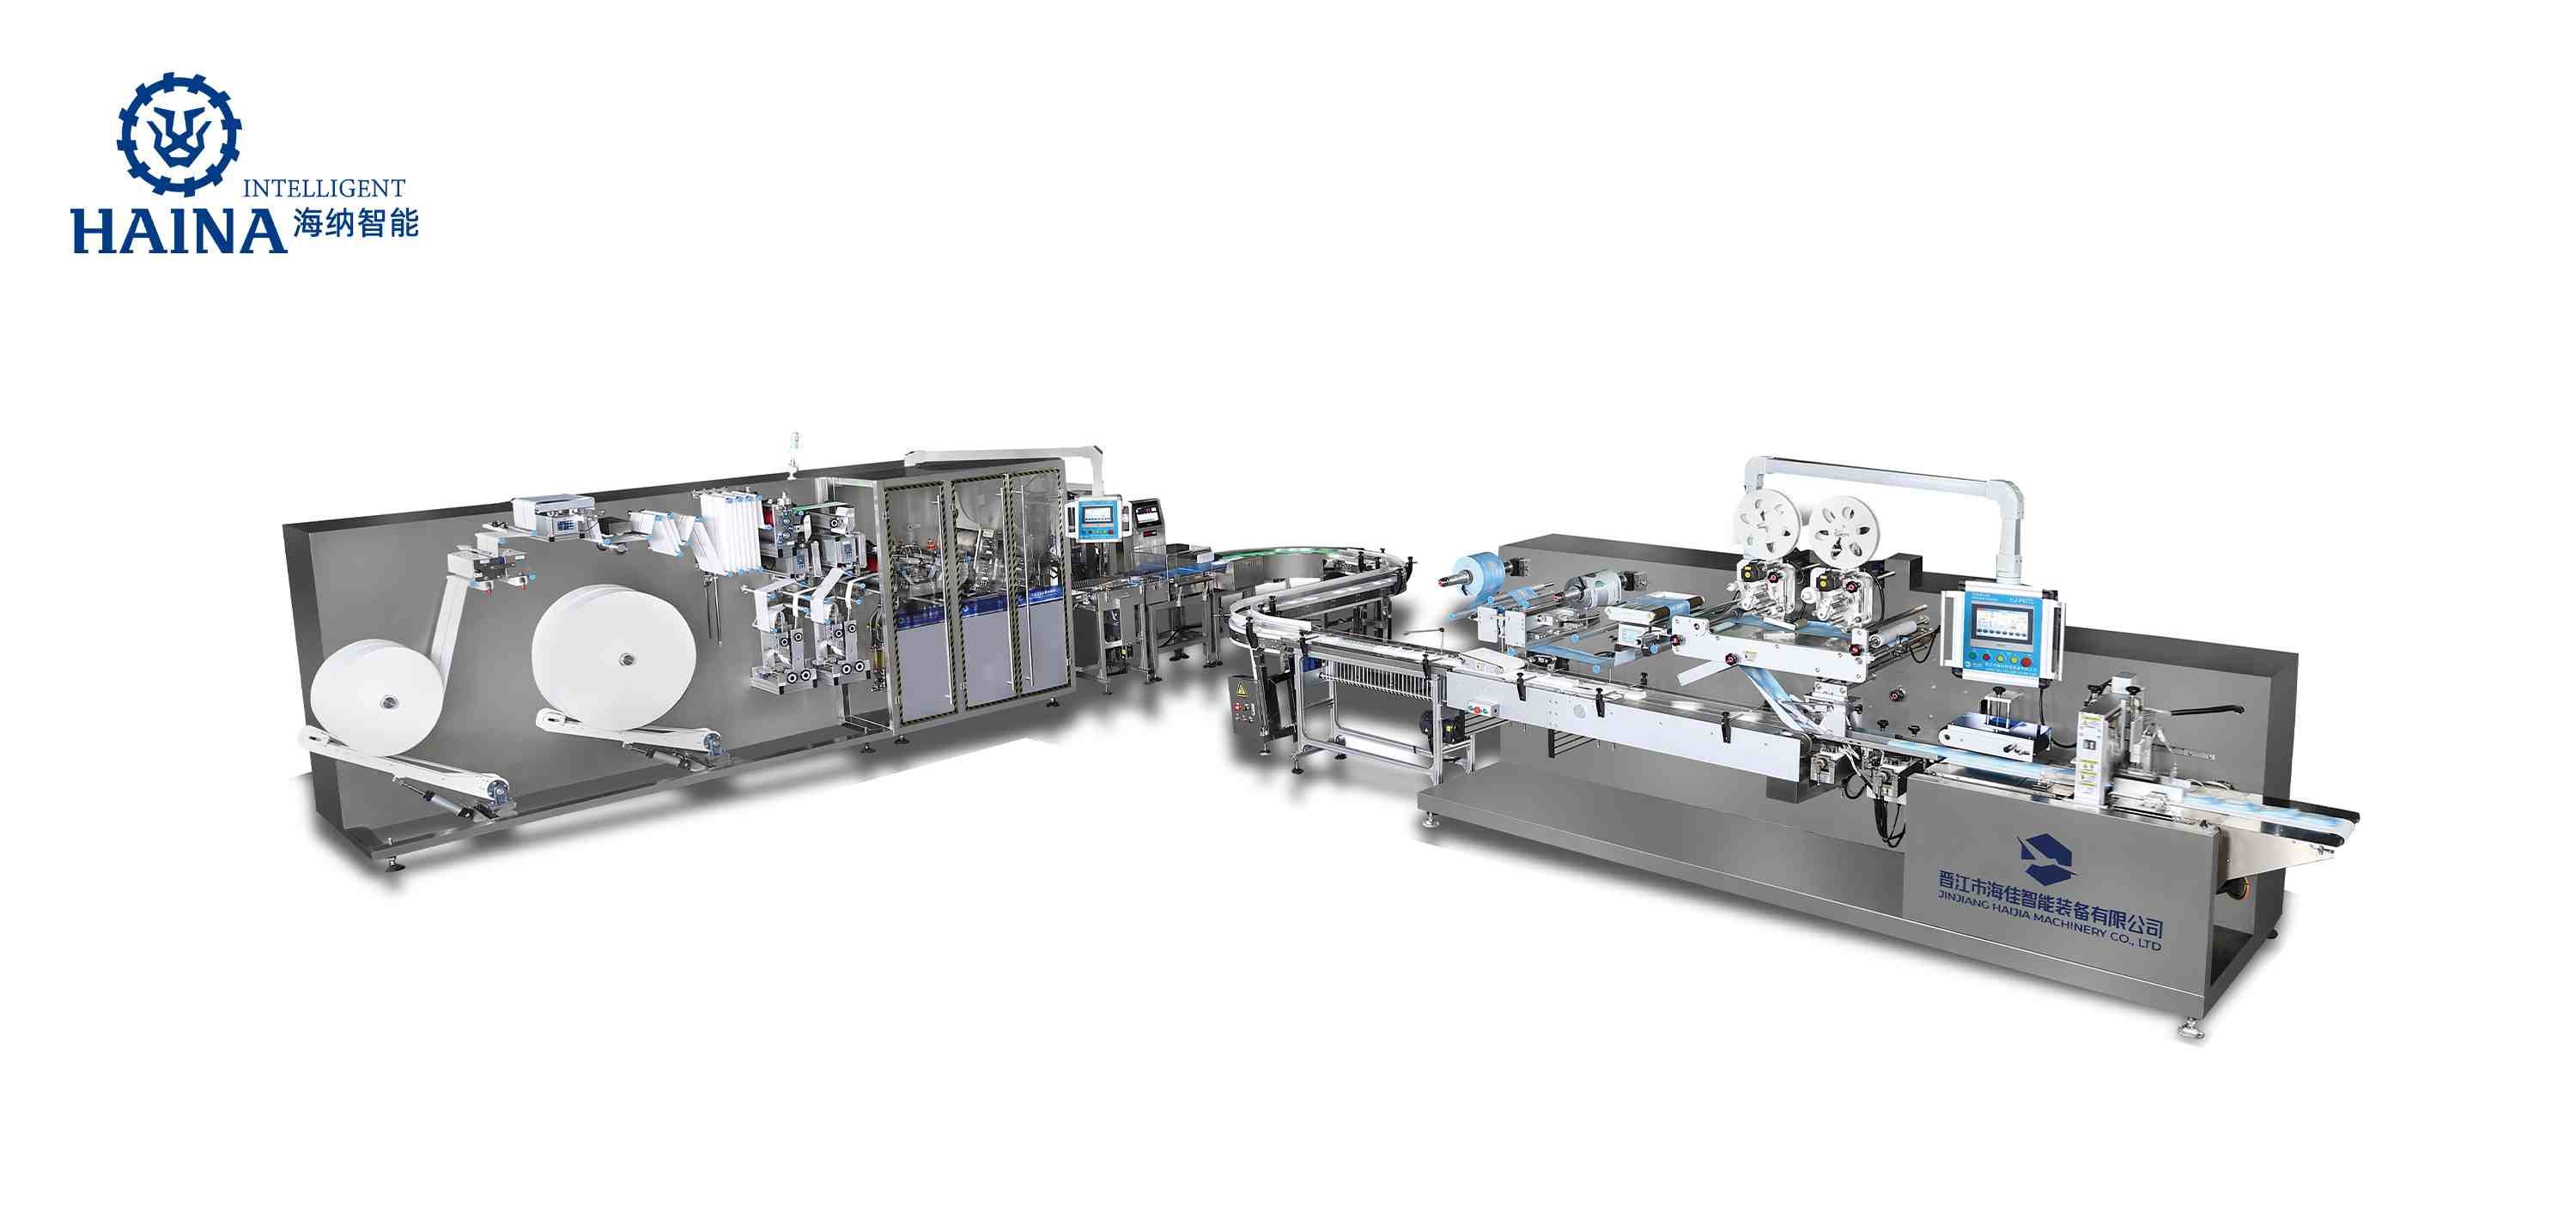
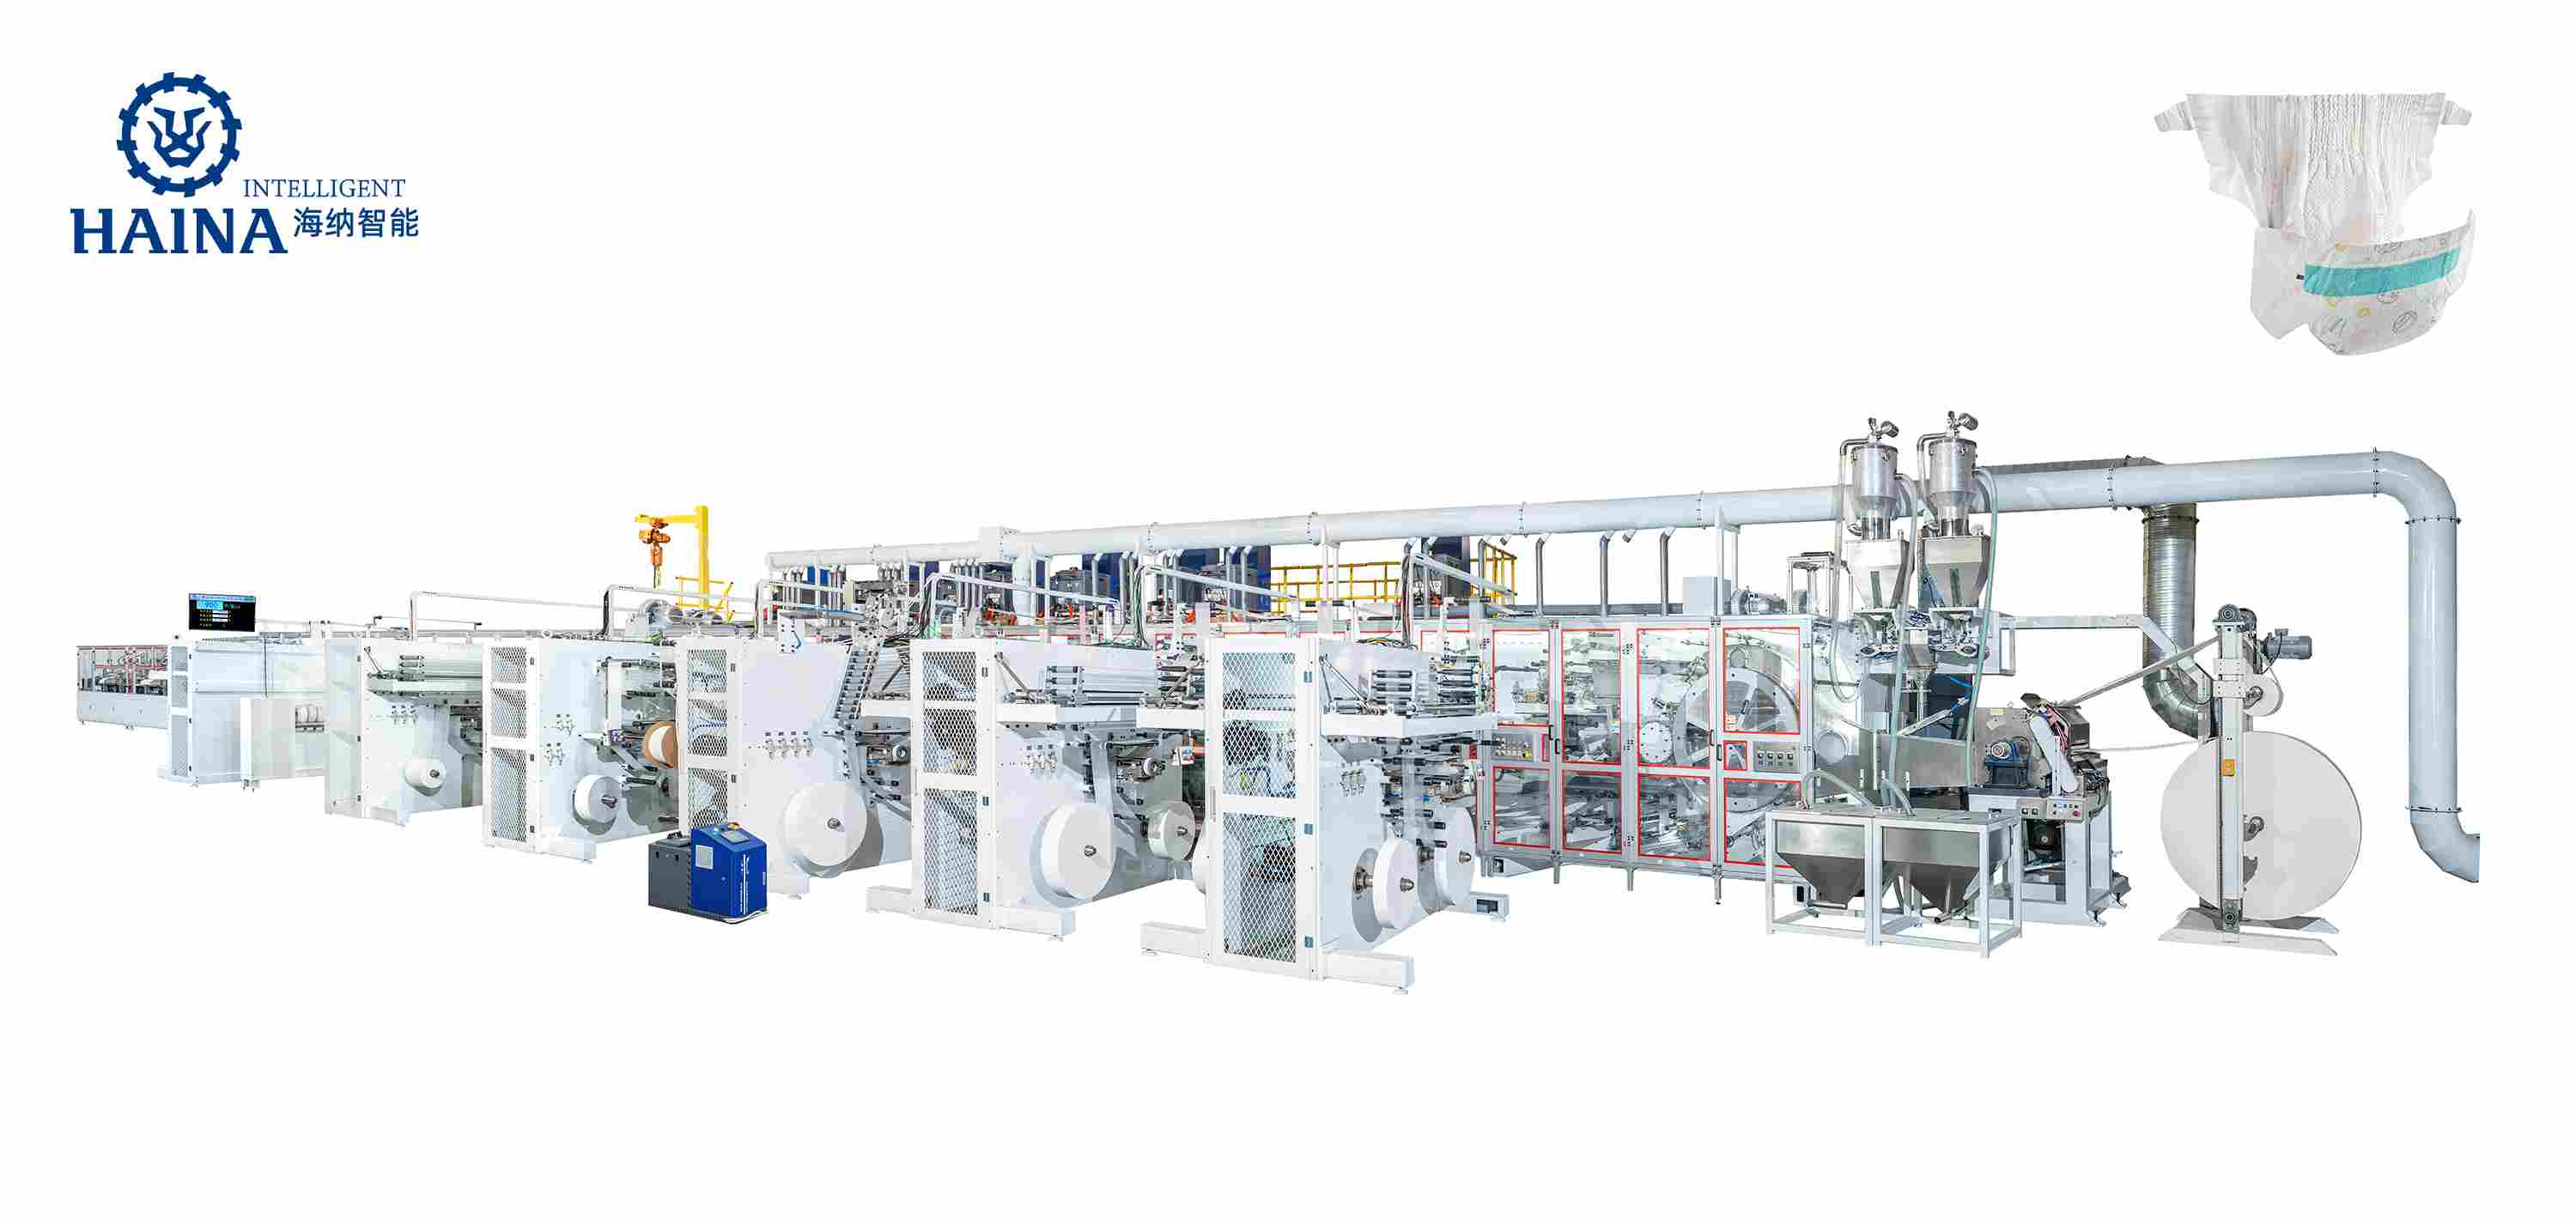
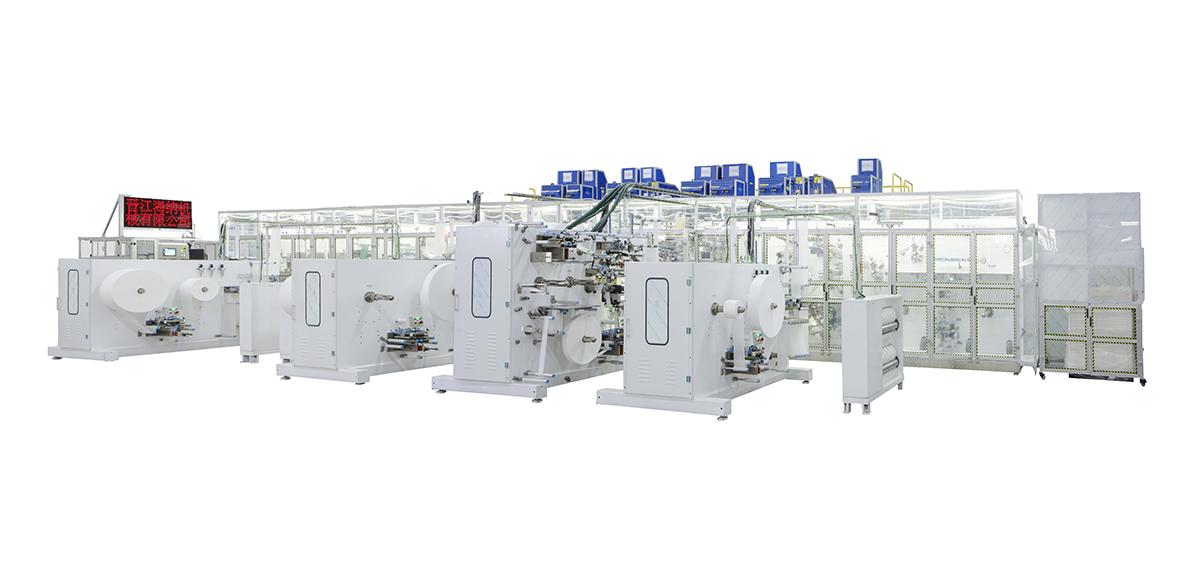
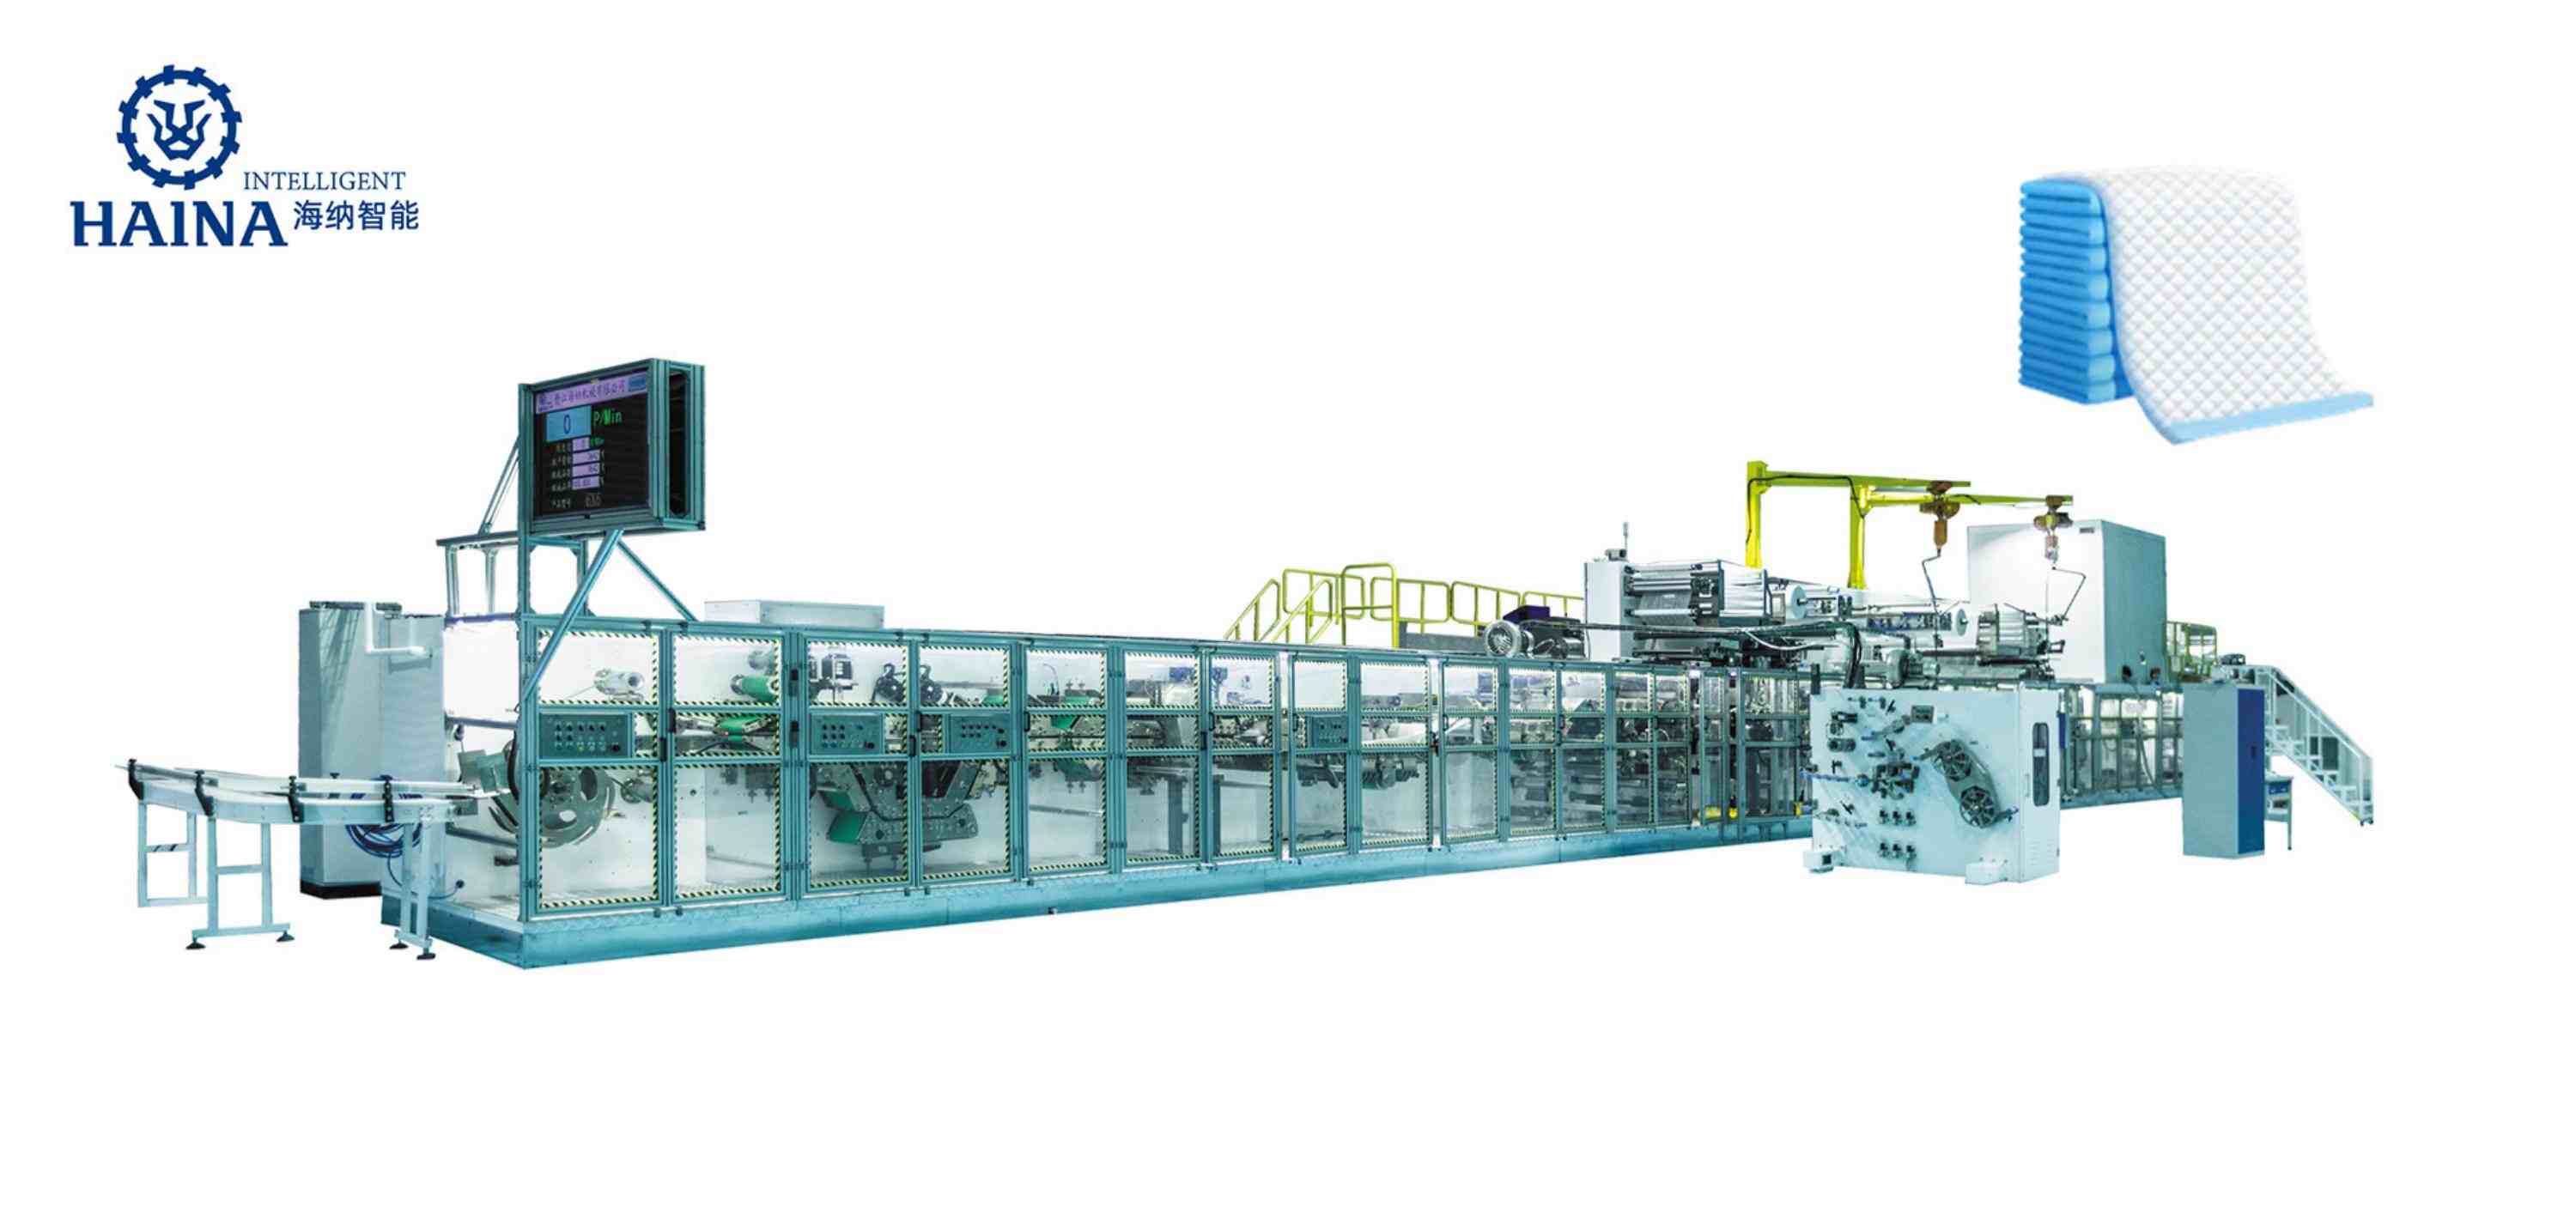
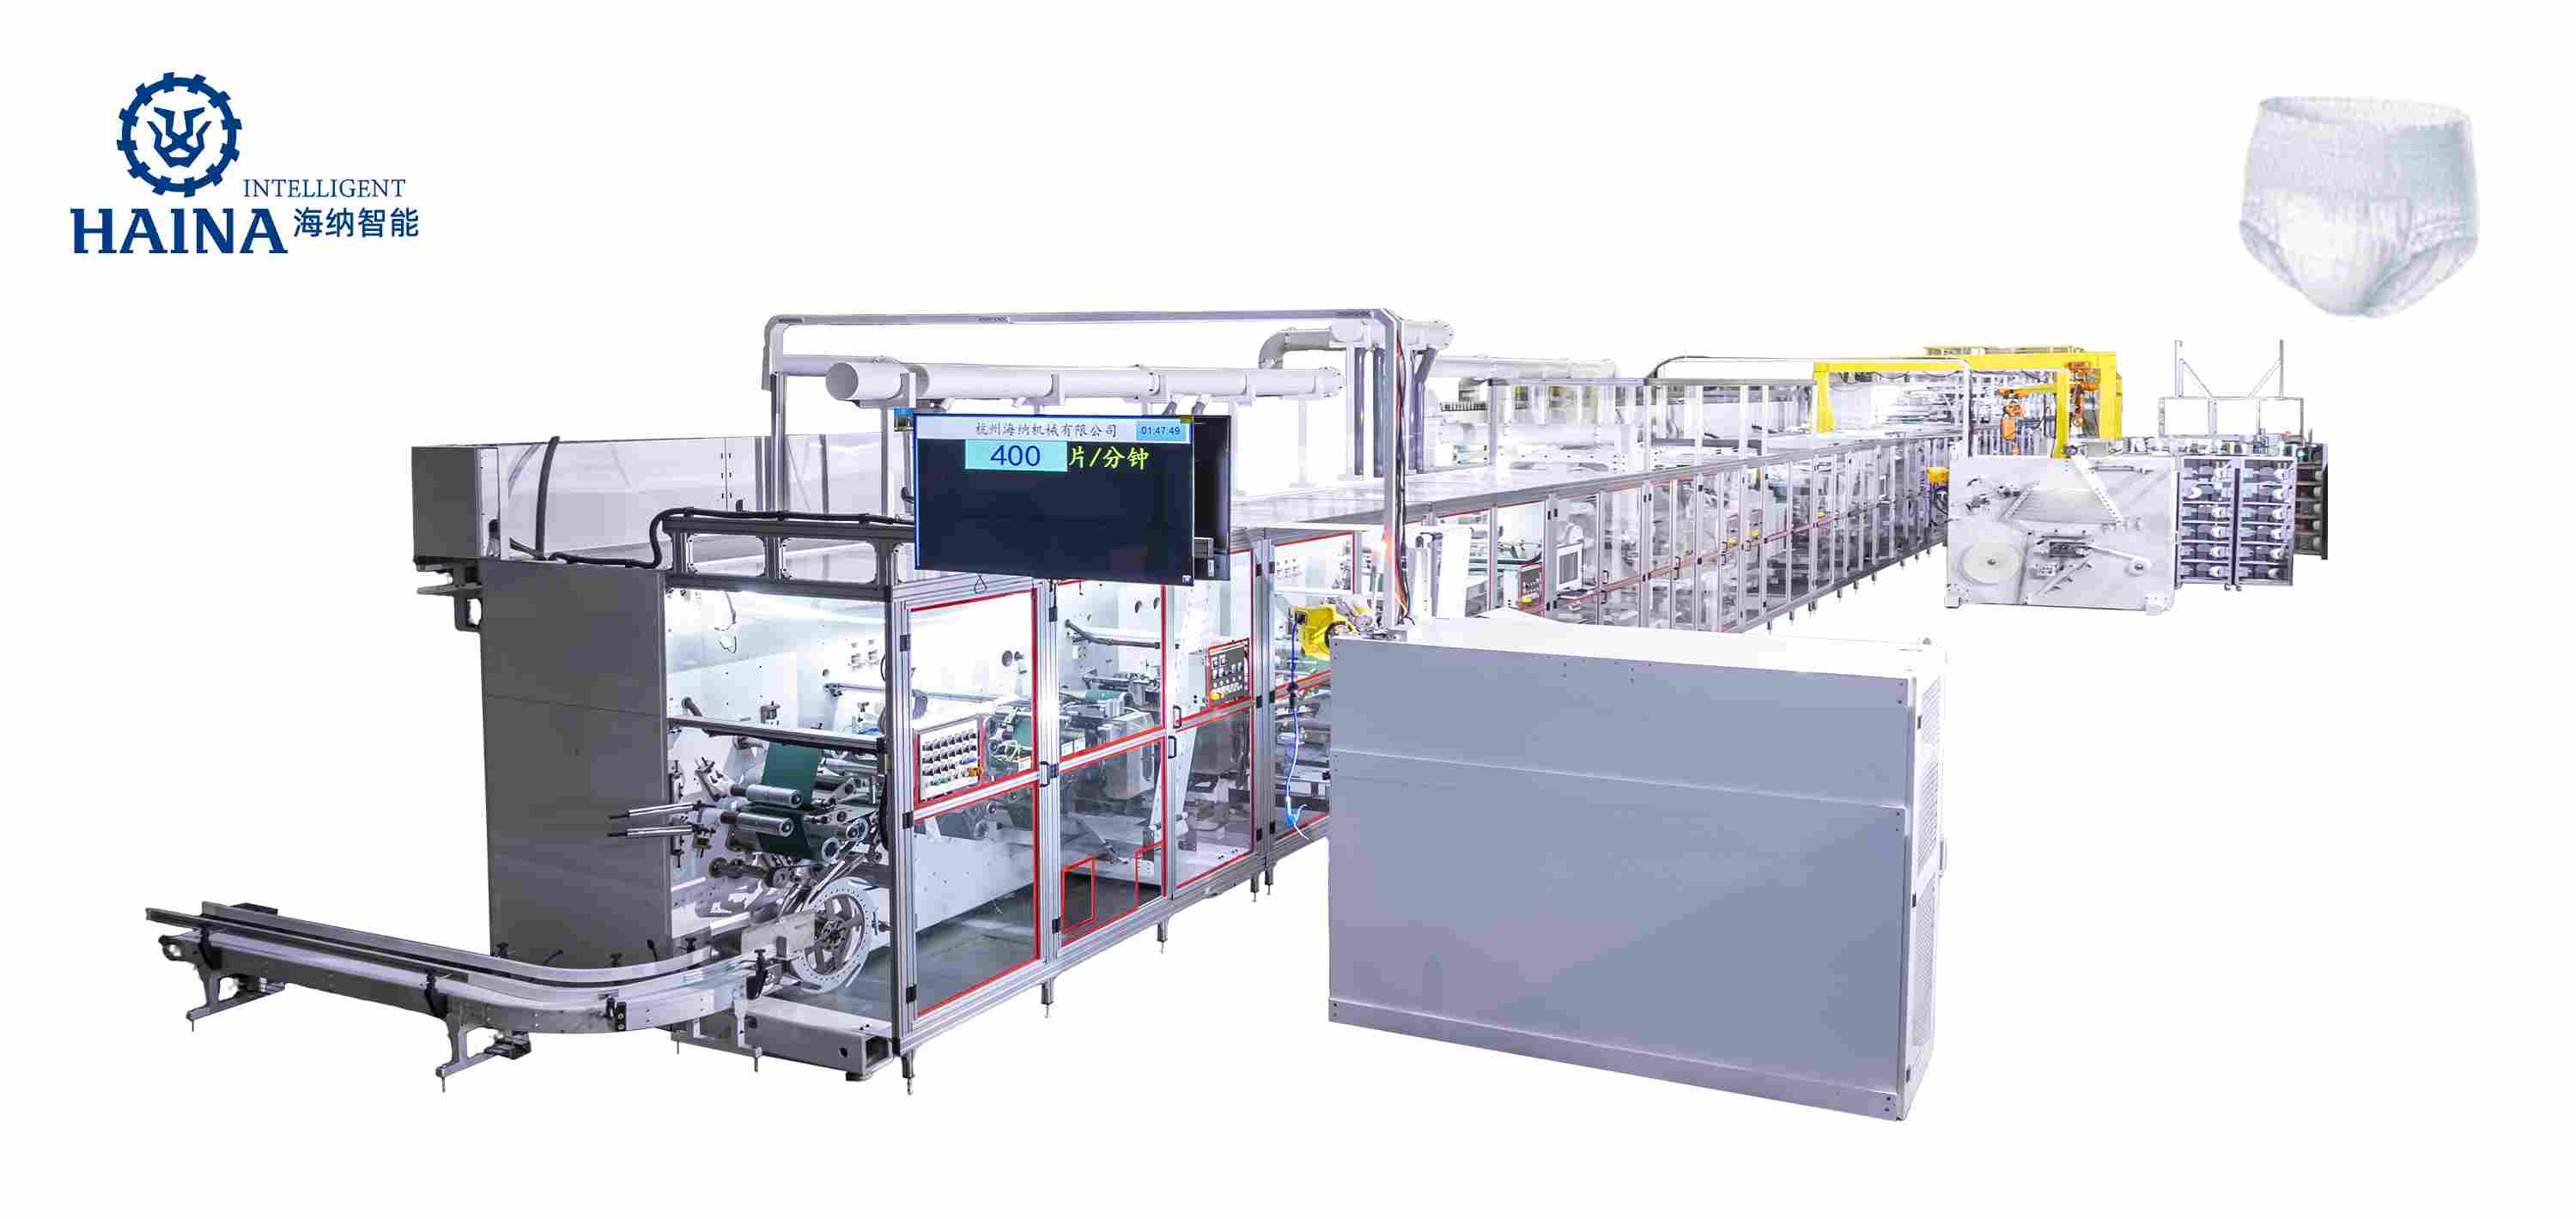
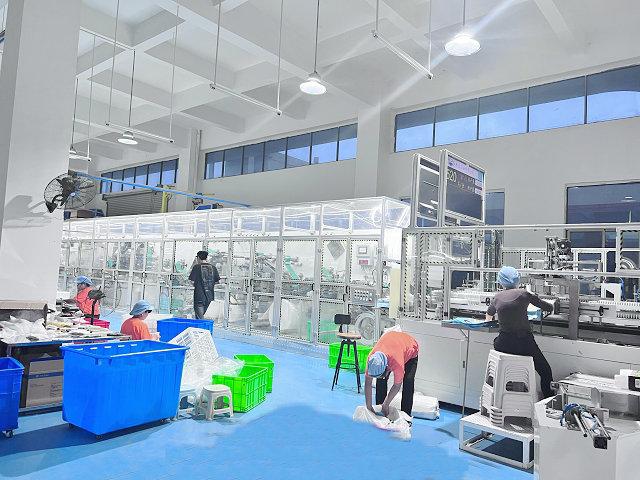
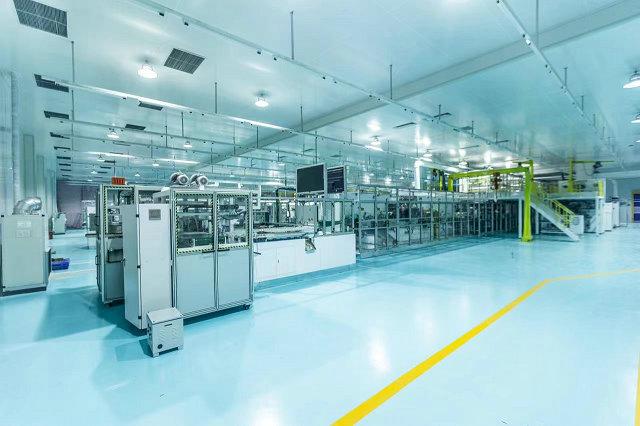
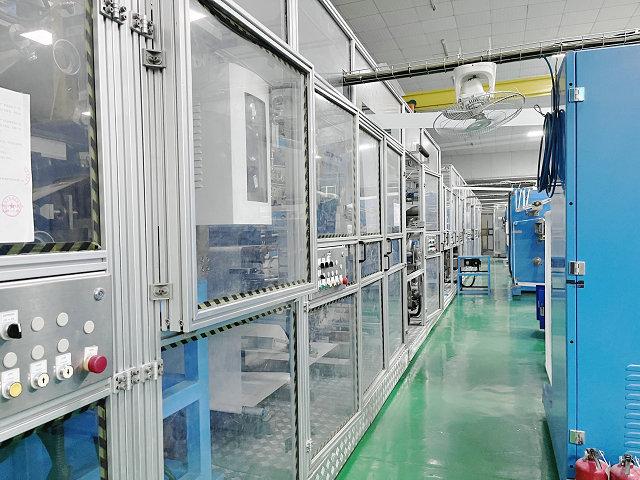
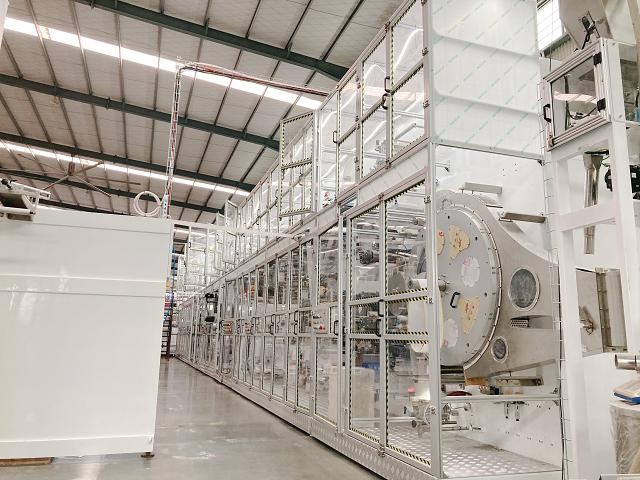
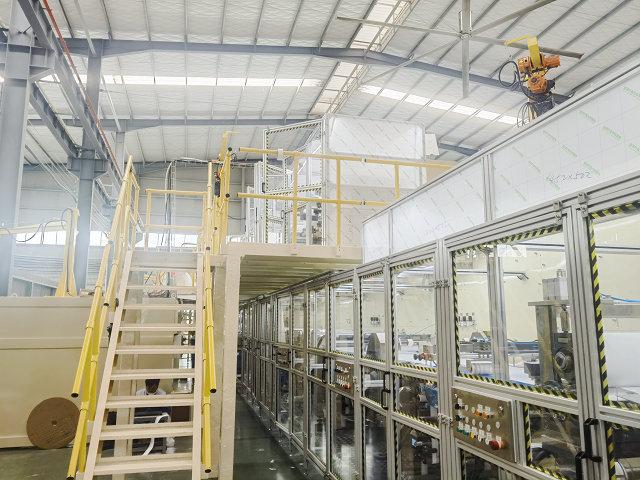
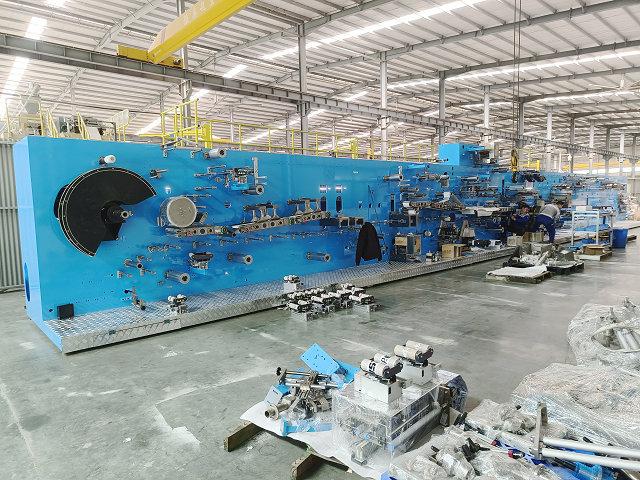
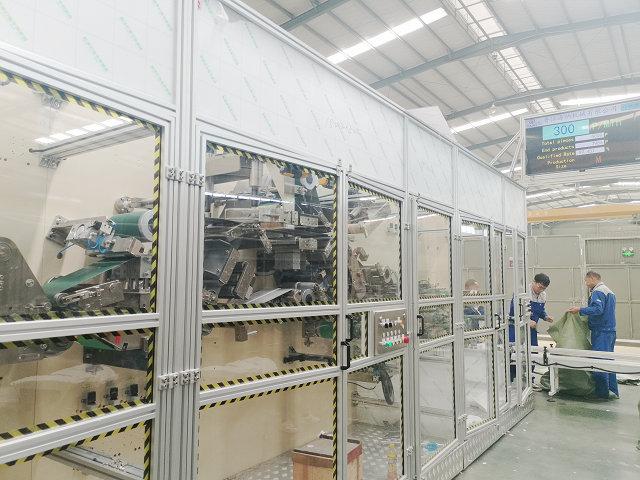
The guide titled Fully Automatic Baby Pull-Ups Machine Video is a starting point for examining baby pull-up pant equipment. Here the main questions concern quality inspection close to the source, then component registration, with automation boundary treated as a separate installation decision. HAINA keeps the published title and media link while adding a testable review path.
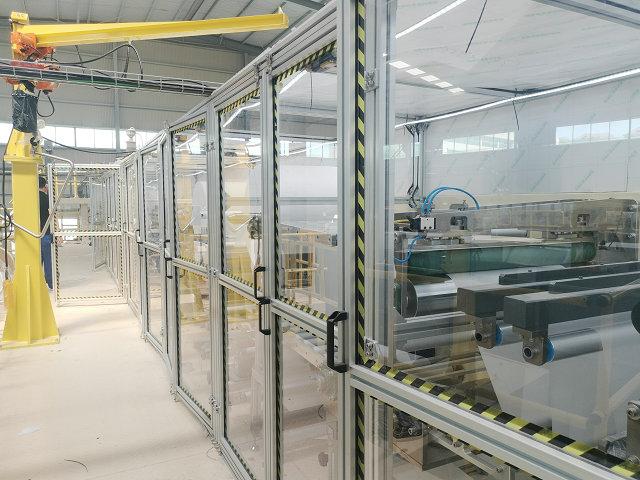
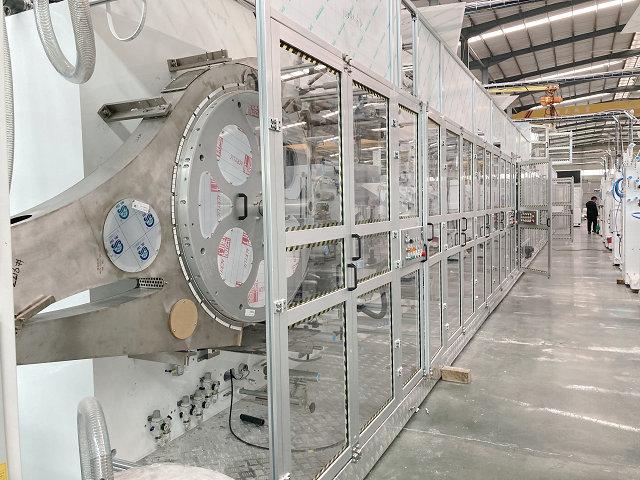
Compare the shown route with the purchaser's intended material route when studying the Fully Automatic Baby Pull-Ups Line footage; keep open questions beside the relevant installation document.
Compare the shown route with the buyer's intended material route for Fully Automatic Baby Pull-Ups Machine
A short run says little about roll changes, recovery time or downstream accumulation. For this guide, follow the path from absorbent chassis formation to pant folding and discharge. The process engineer should concentrate on material references, driven relationships and product tolerances while another reviewer notes every edit, intervention or hidden transfer.
Absorbent chassis formationFor Fully Automatic Baby Pull-Ups Line, note the handoff toward waist laminate preparation and link the observation to leg-opening symmetry.
Waist laminate preparationFor Fully Automatic Baby Pull-Ups Line, follow the handoff toward elastic control and link the observation to side condition.
Elastic controlFor Fully Automatic Baby Pull-Ups Line, check the handoff toward leg opening and side processing and link the observation to final fold.
Leg opening and side processingFor Fully Automatic Baby Pull-Ups Line, observe the handoff toward pant folding and discharge and link the observation to waist recovery.
Pant folding and dischargeFor Fully Automatic Baby Pull-Ups Line, trace the handoff toward absorbent chassis formation and link the observation to core-to-waist position.
Primary evidence at quality inspection close to the source
A useful inspection point sits near the station that creates the defect. This shortens diagnosis and limits the quantity made before correction. Applied to Fully Automatic Baby Pull-Ups Line, this means comparing the filmed condition with waist recovery and leg-opening symmetry on samples from the same operating period.
When the line changes speed, verify measurement of the critical feature and connect it to the finished-product result for core-to-waist position on Fully Automatic Baby Pull-Ups Line.
The team should document inspection location, then retain the corresponding Fully Automatic Baby Pull-Ups Line sample used to assess leg-opening symmetry.
For Fully Automatic Baby Pull-Ups Line, assess sample frequency before judging side condition at the next sampling point.
Around response to an out-of-limit result, compare the line condition and the later final fold outcome instead of relying on appearance.
Evidence gap: The earlier text for Fully Automatic Baby Pull-Ups Line did not provide a usable measured value. Ask for a timed run that identifies the SKU, approved material lots, accepted output, stops and rejects instead of inferring performance from screen speed.
Automation boundary for this project
Automation scope must identify the maker, stacker, bagger, inspection, rejection and case-handling boundaries one interface at a time. In the case of Fully Automatic Baby Pull-Ups Line, request an interface matrix showing which modules communicate, accumulate, stop and restart together. Keep the answer separate from the footage so an optional module or untested value is not mistaken for accepted scope.
Review layer
Guide-specific check
Film observation
Follow elastic control and mark the transition into leg opening and side processing for Fully Automatic Baby Pull-Ups Line.
First measurement
At quality inspection close to the source, check inspection location against leg-opening symmetry.
Independent review
Have the process engineer examine component registration for material references, driven relationships and product tolerances.
Document request
Request an interface matrix showing which modules communicate, accumulate, stop and restart together and accepted packed output with maker and packer stops classified separately for the Fully Automatic Baby Pull-Ups Line installation file.
Acceptance log
For Fully Automatic Baby Pull-Ups Line, retain samples showing final fold near quality inspection close to the source and reconcile them with stops, splices and accepted downstream output.
Second pass at component registration
Registration is a relationship between a material reference edge, sensor, driven axis and finished-product tolerance. The camera rarely shows all four at once. This second lens is deliberately different from quality inspection close to the source: for Fully Automatic Baby Pull-Ups Line, it should produce measured registration samples from each planned size or recipe, with the result reviewed by the process engineer.
Against the retained product sample, trace sensor location and connect it to the finished-product result for side condition on Fully Automatic Baby Pull-Ups Line.
The team should confirm component datum, then retain the corresponding Fully Automatic Baby Pull-Ups Line sample used to assess final fold.
For Fully Automatic Baby Pull-Ups Line, inspect correction method before judging waist recovery at the next sampling point.
Around products after a restart, note the line condition and the later core-to-waist position outcome instead of relying on appearance.
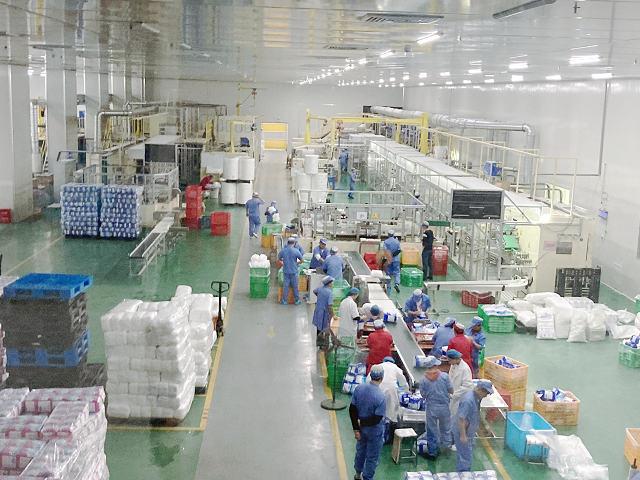
For Fully Automatic Baby Pull-Ups Line, the process engineer should use maker-to-packer handoff as a third cross-check after reviewing quality inspection close to the source. A line is only as productive as the transfer between the maker and the packer. Counting, accumulation and recovery should be reviewed as one process. Add accepted packed output with maker and packer stops classified separately only when that responsibility is included in the planned line.
Questions raised by the Fully Automatic Baby Pull-Ups Machine recording
What does the Fully Automatic Baby Pull-Ups Machine footage show well?
It helps locate absorbent chassis formation, quality inspection close to the source and pant folding and discharge. For this Fully Automatic Baby Pull-Ups Line review, it does not by itself establish waist recovery over time or confirm the component registration responsibility outside the camera view.
Which follow-up matters most for Fully Automatic Baby Pull-Ups Machine?
Ask for a control plan linking every critical feature to method, owner and response. Match that log to the same materials and SKU shown during the Fully Automatic Baby Pull-Ups Line review so that the observation and result describe one run.
How should a buyer use this baby pull-up pant video?
Use it to prepare questions for component registration, automation boundary and core-to-waist position. Close those questions through drawings, retained samples and signed acceptance outcomes.
Close the review with traceable evidence
File this footage with the product sample, material list, process drawing, line layout, utility schedule and FAT method for Fully Automatic Baby Pull-Ups Line. Number each open item under quality inspection close to the source, component registration or automation boundary; assign an owner and the verification needed to close it.
Before the equipment scope is signed, HAINA can compare the filmed arrangement with the planned module list for Fully Automatic Baby Pull-Ups Line. Final acceptance should use approved materials, agreed measurement methods and retained outcomes from the named test run, including any finding connected to maker-to-packer handoff.