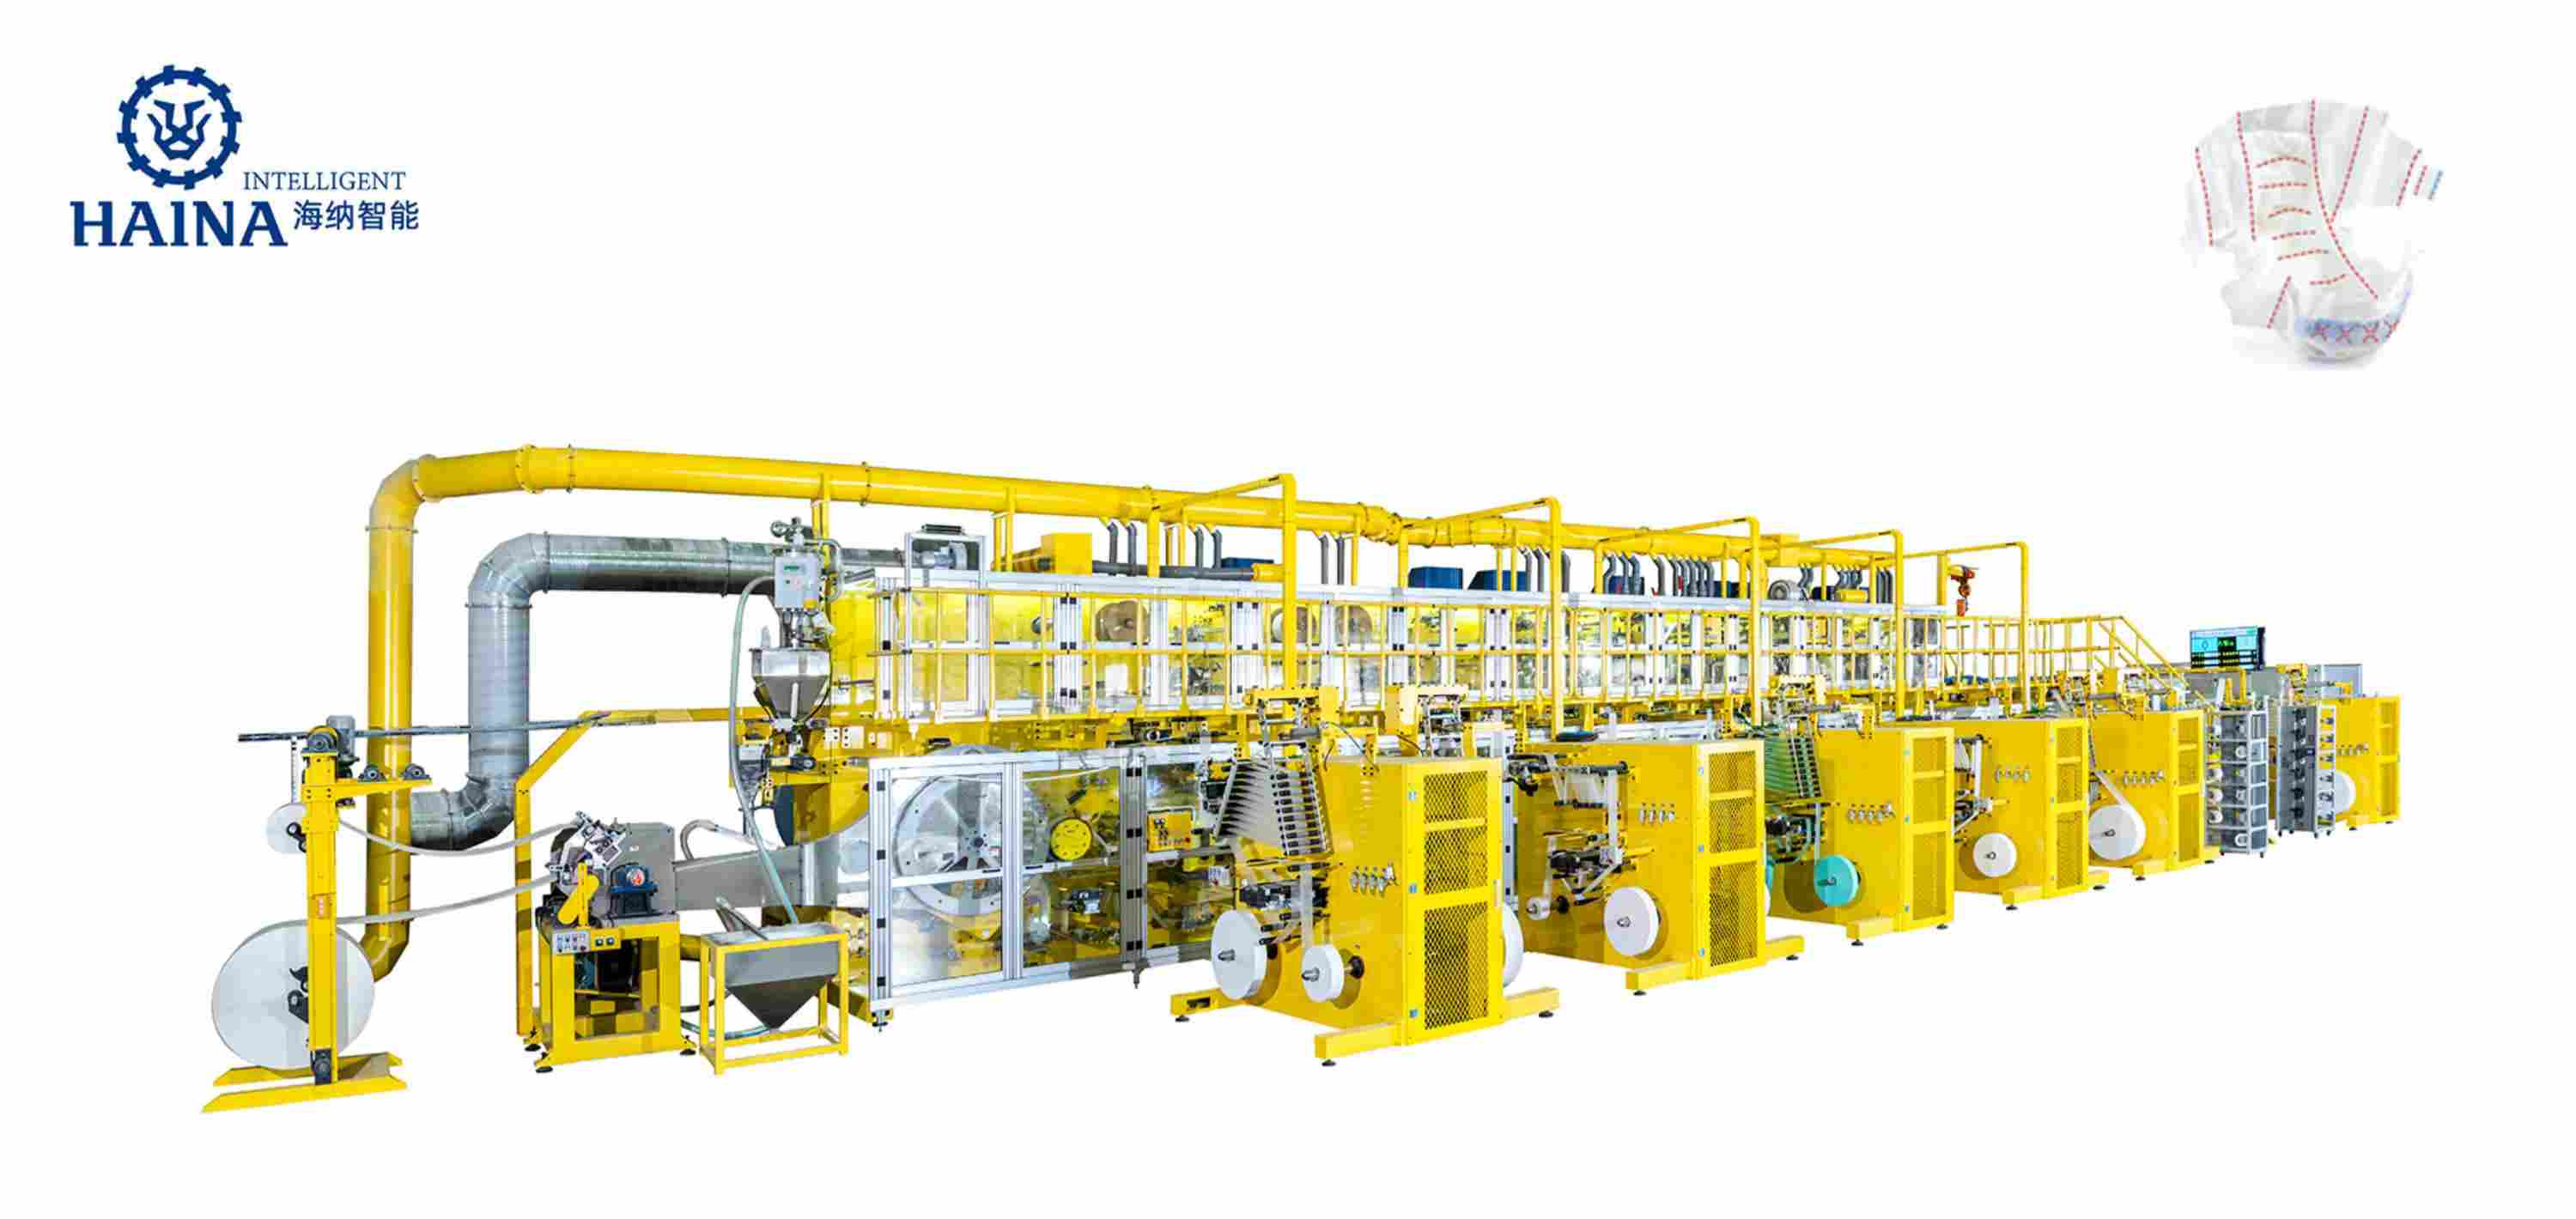
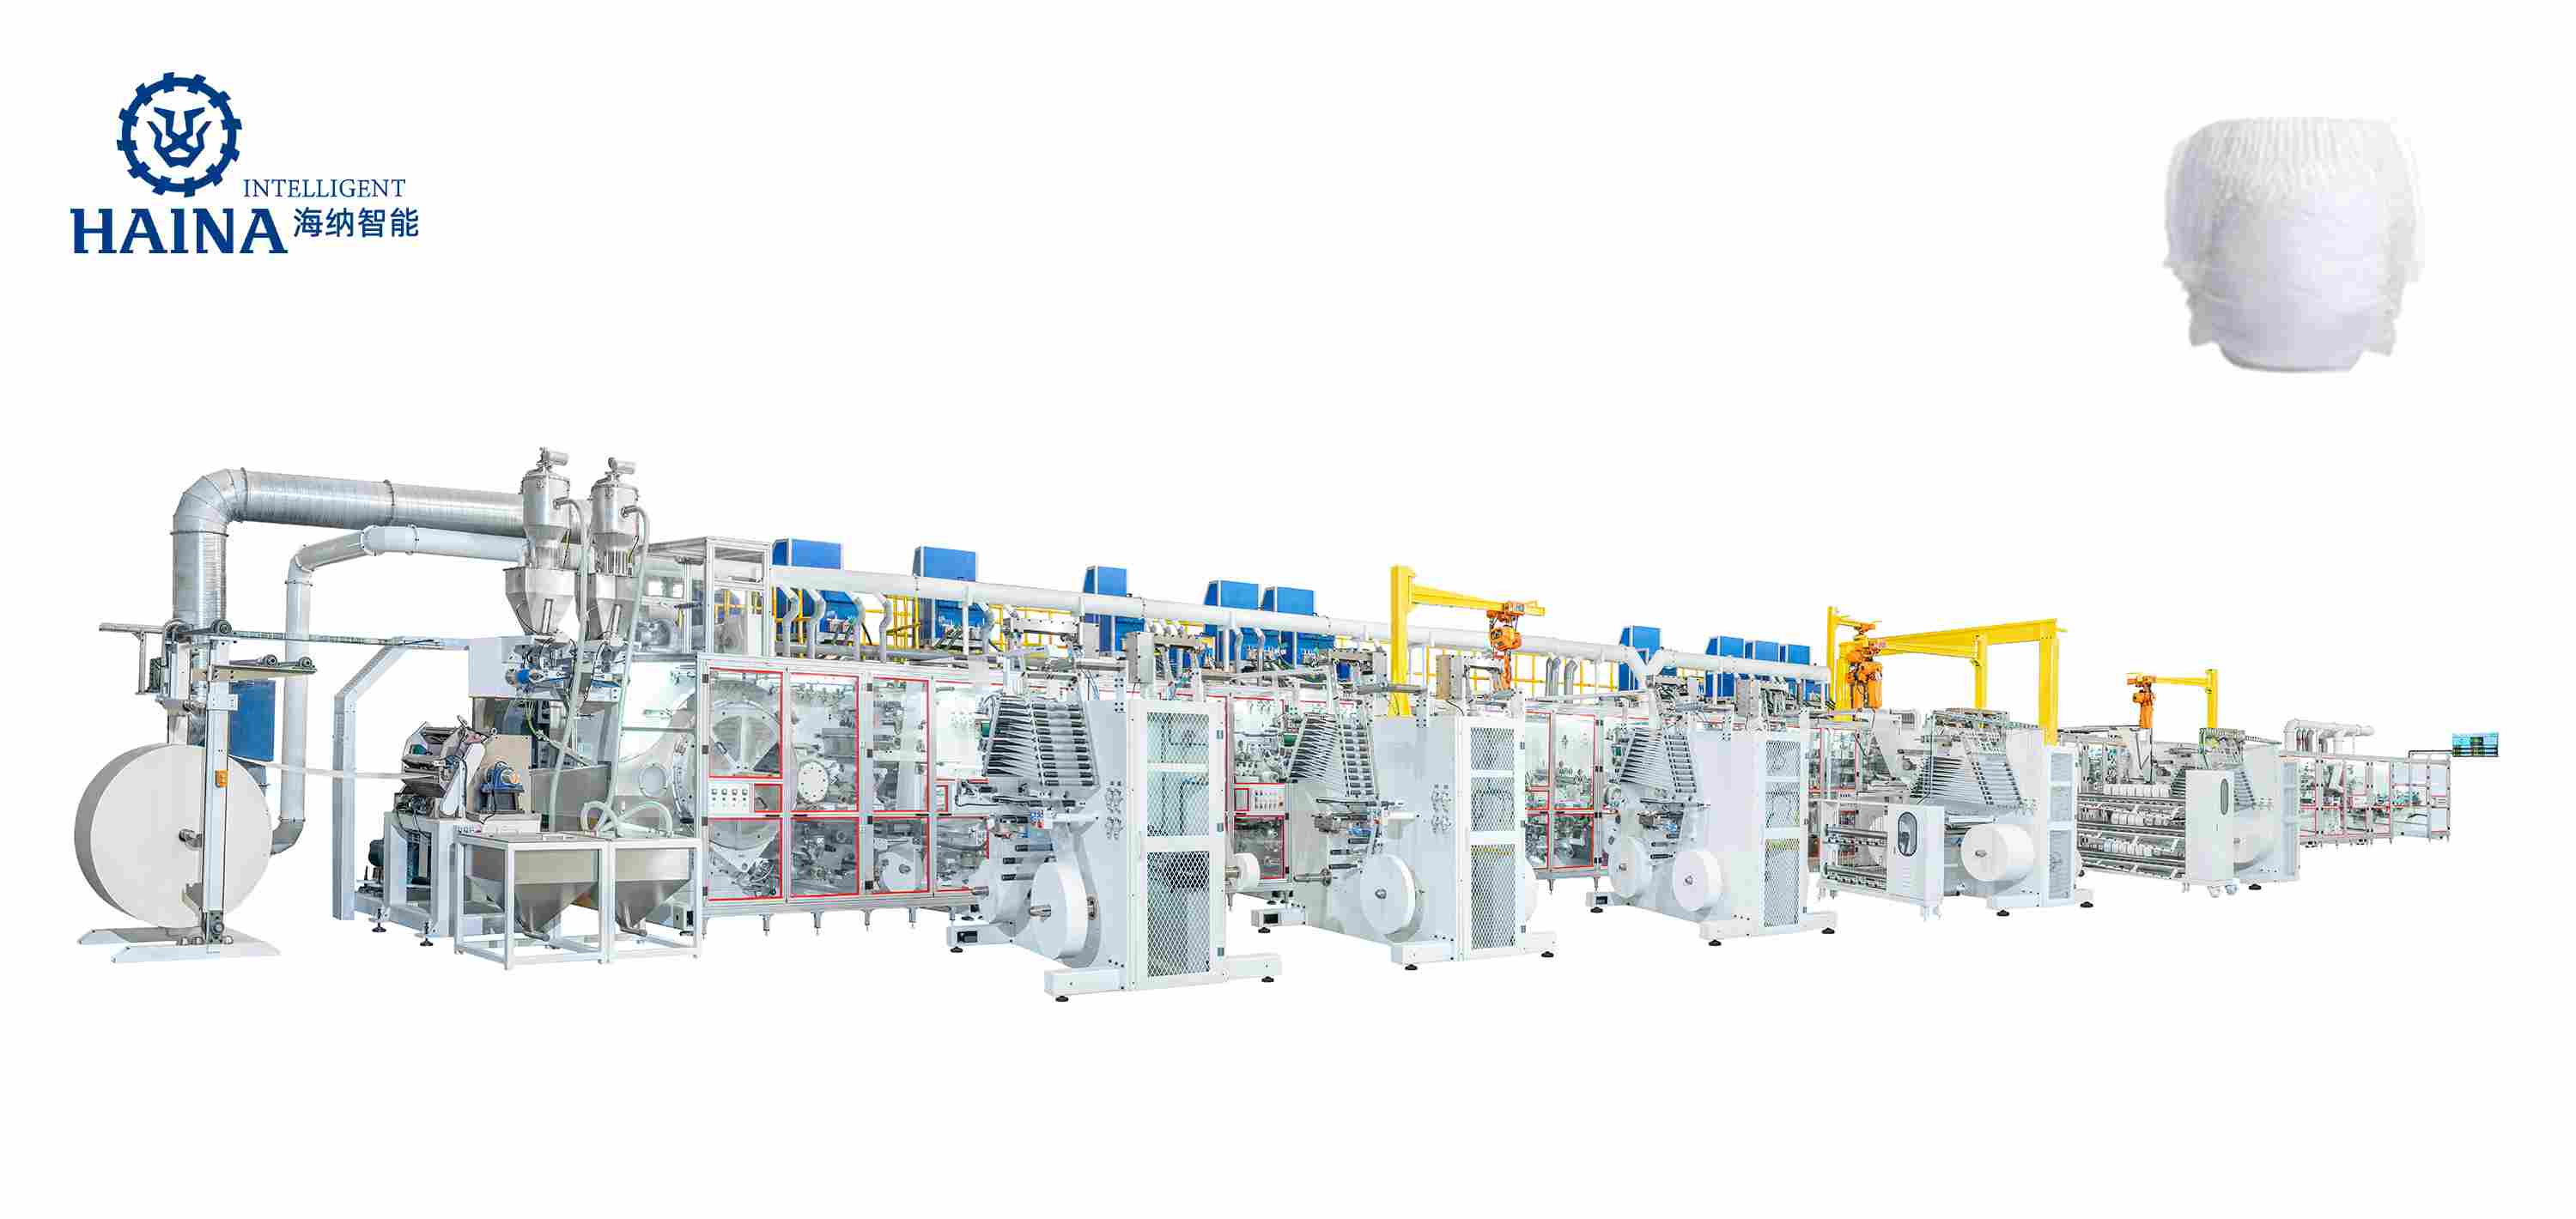
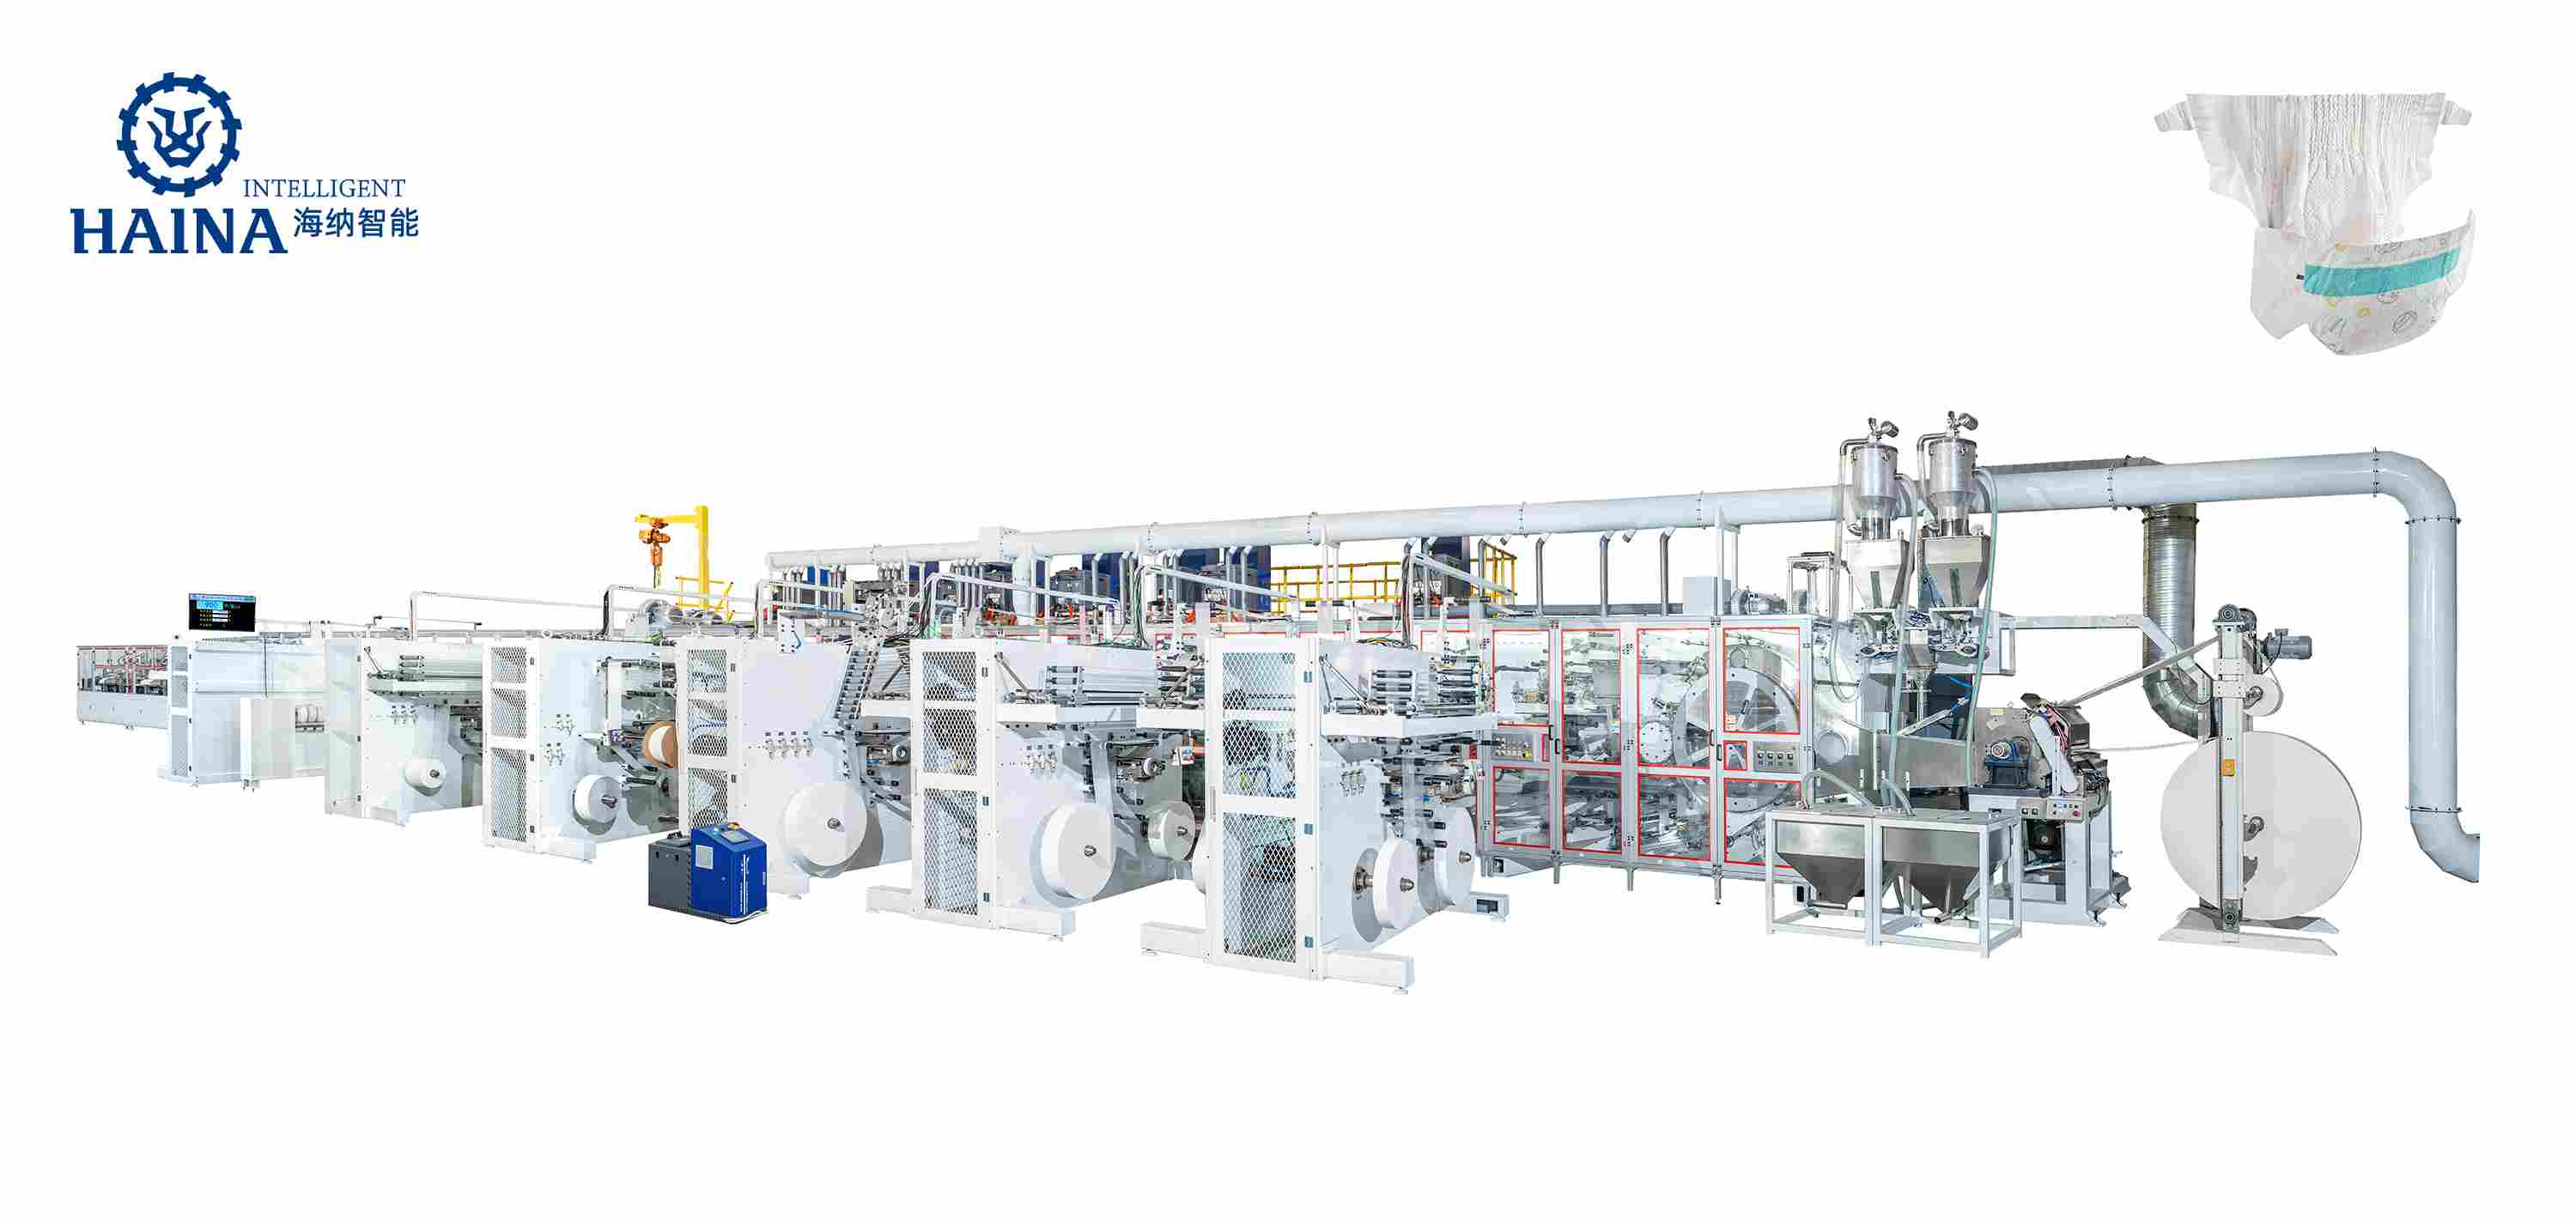
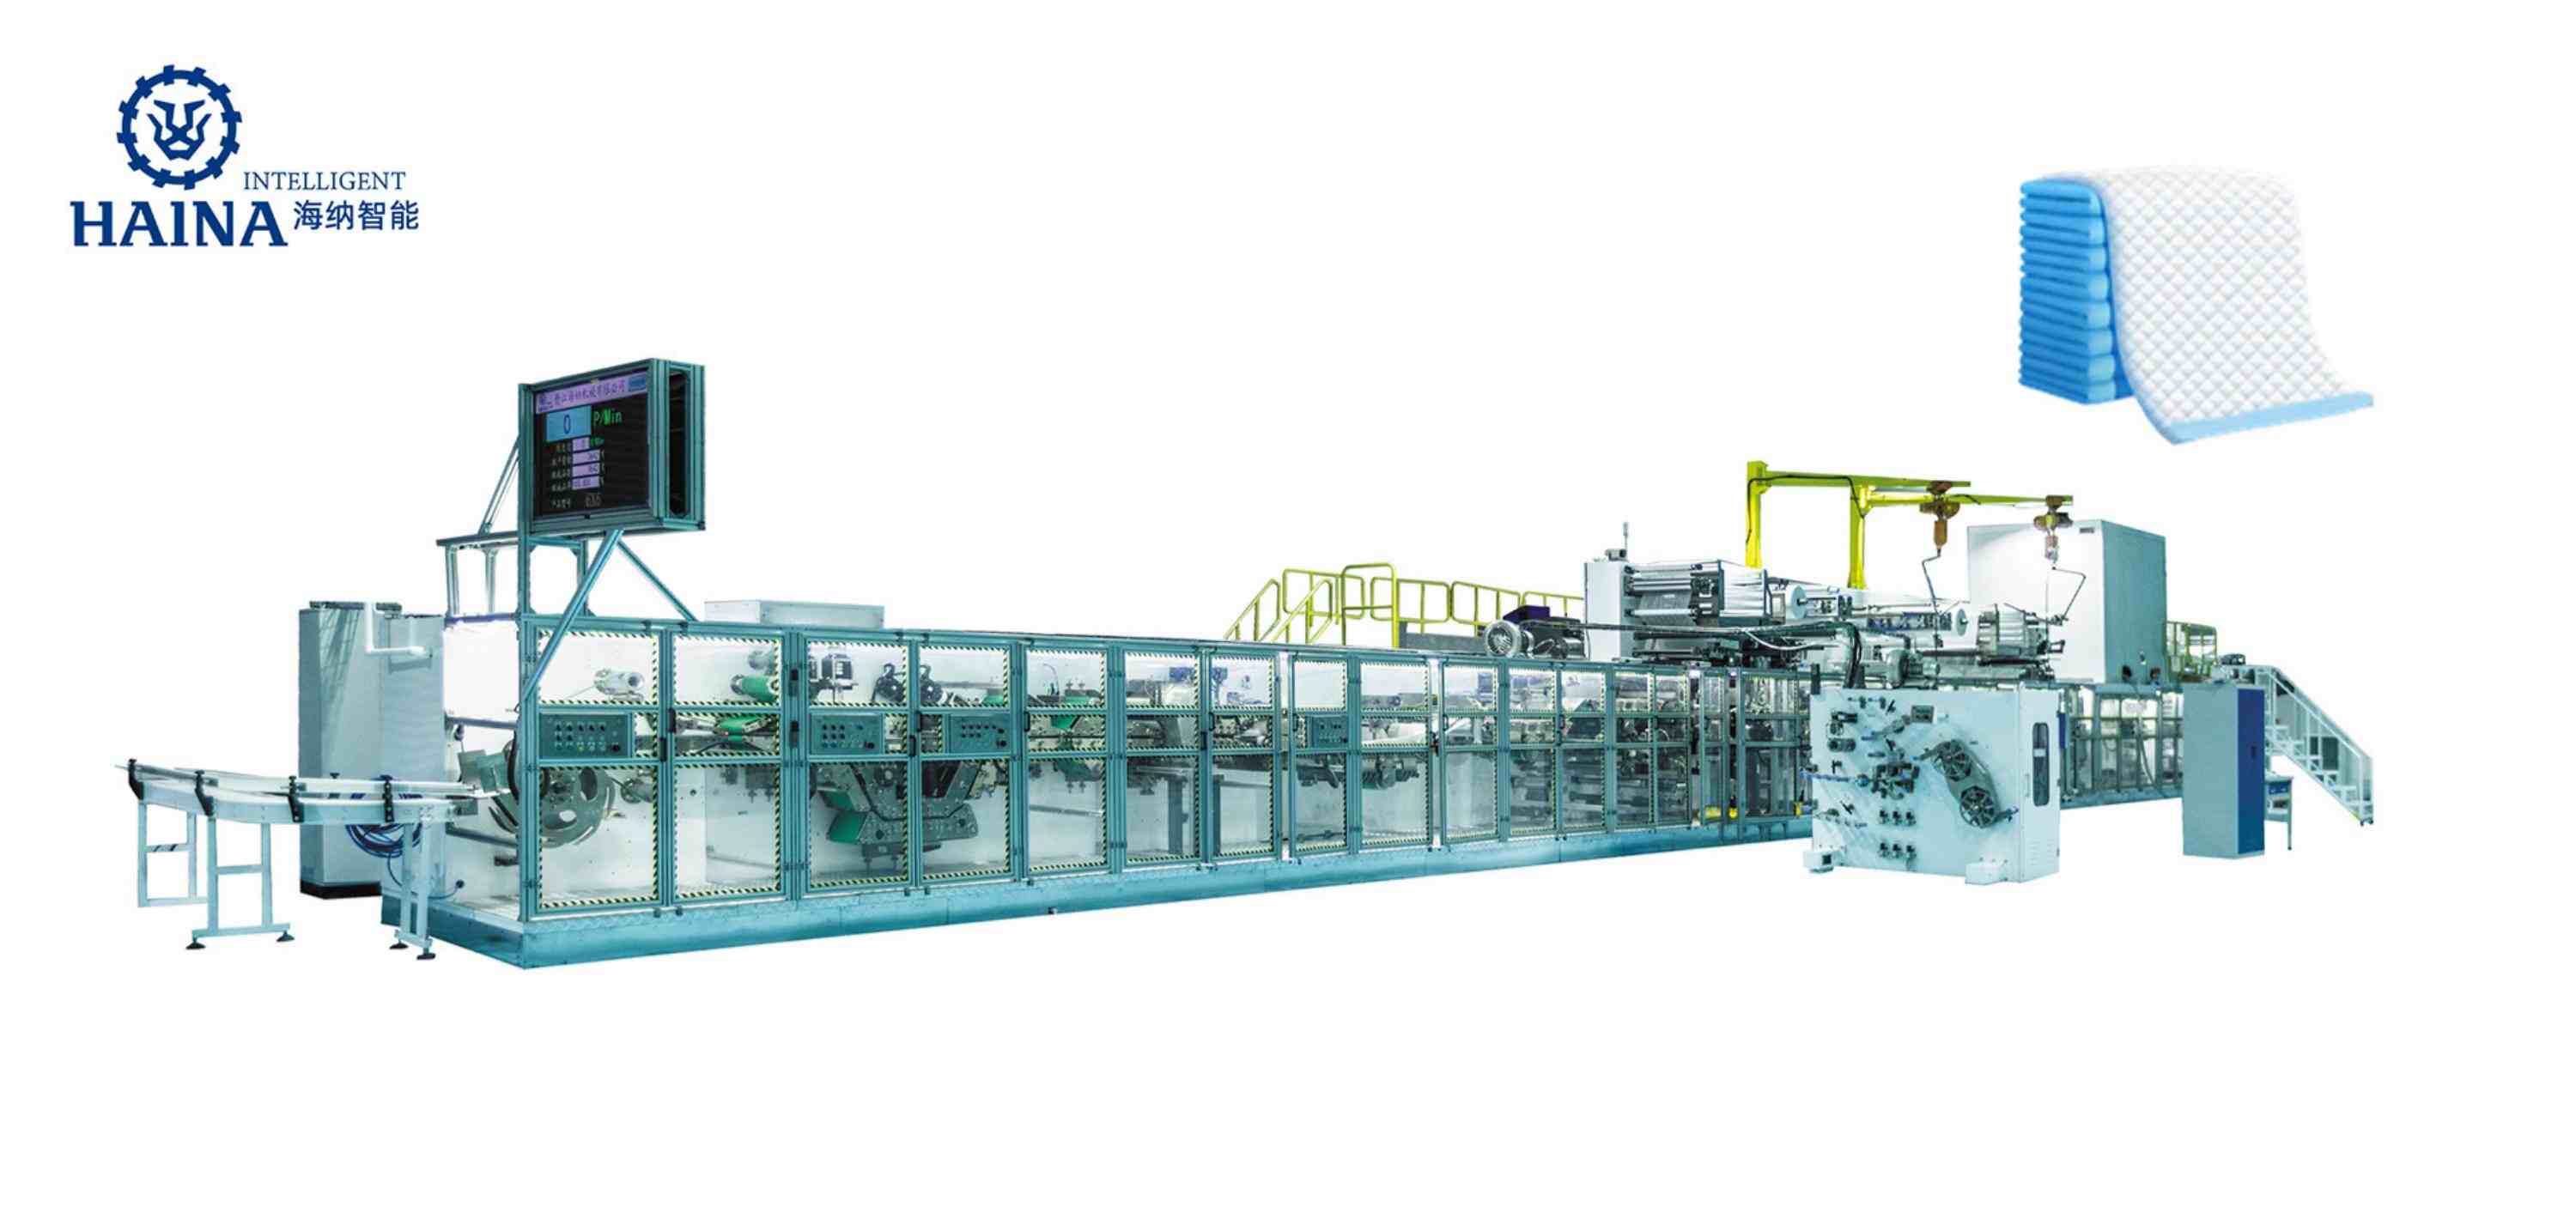
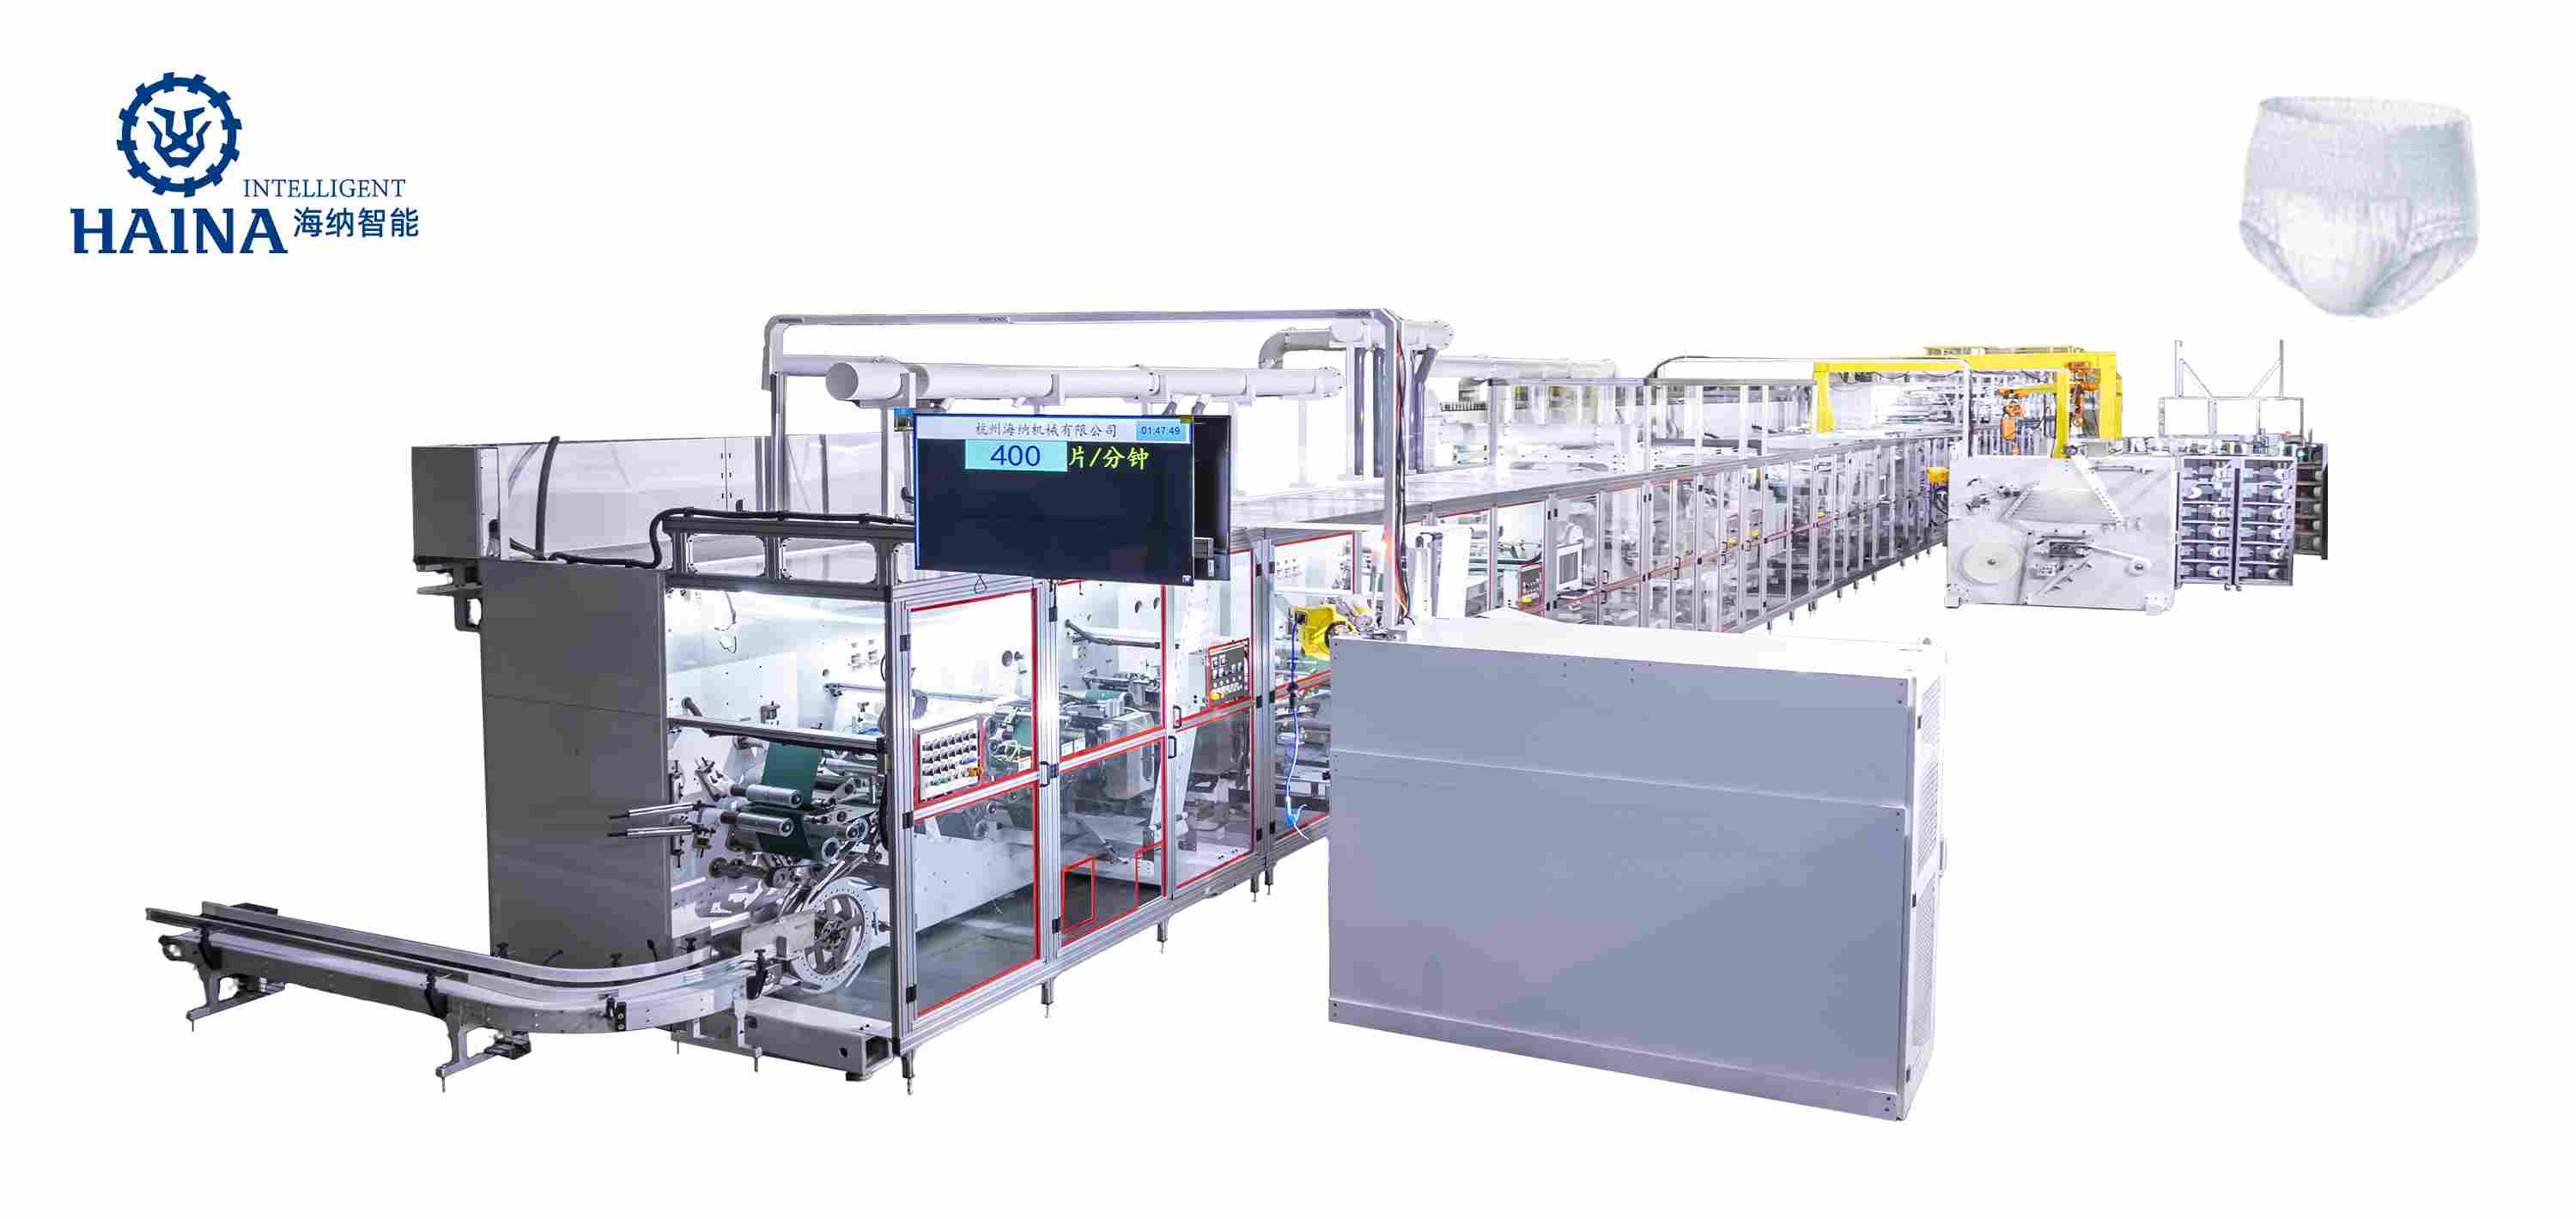
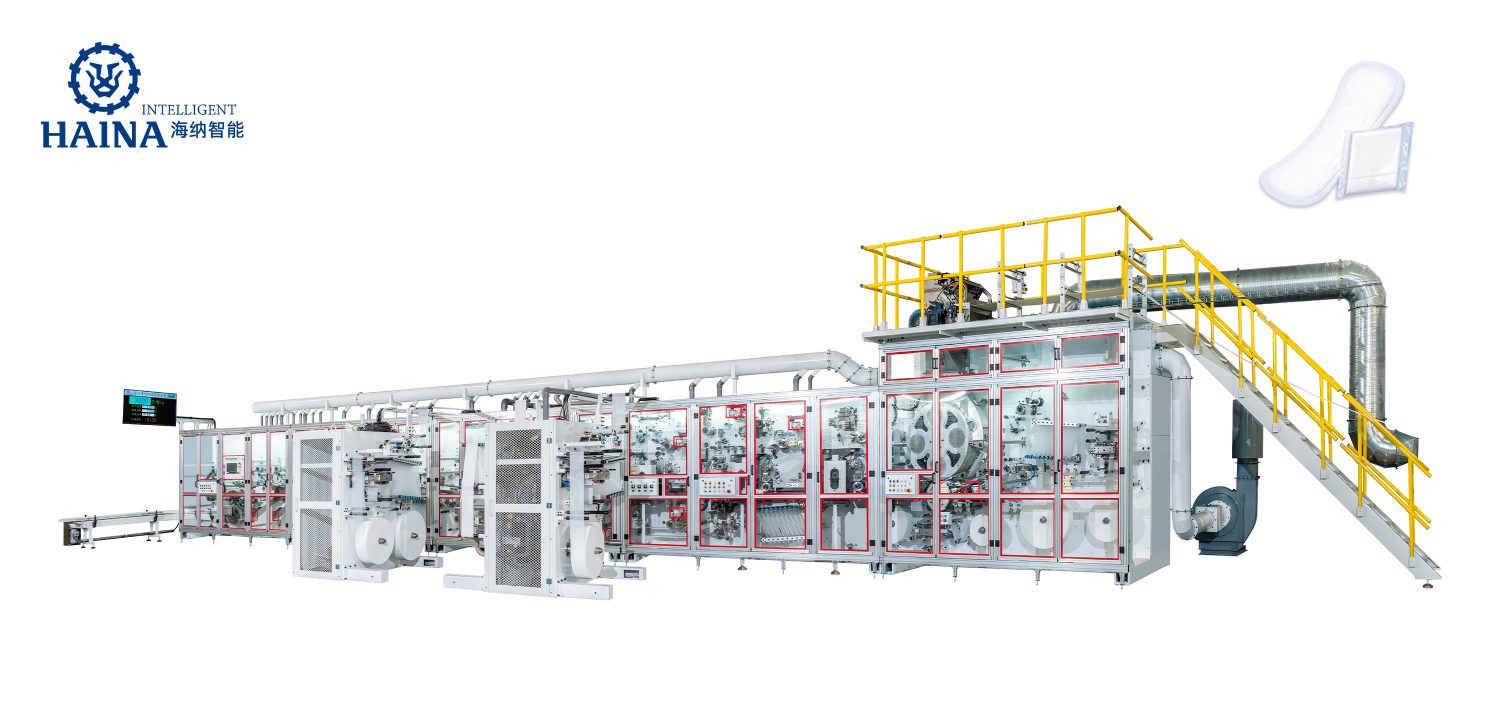
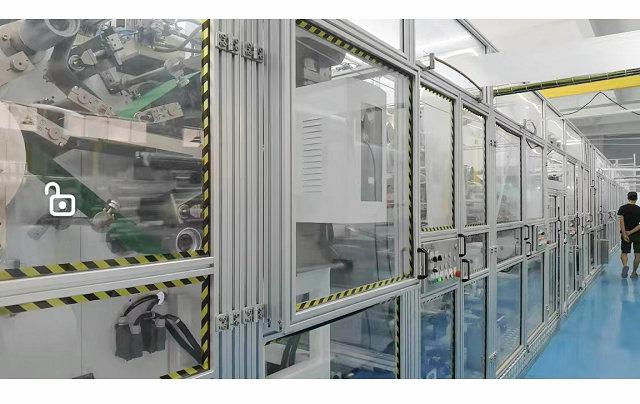
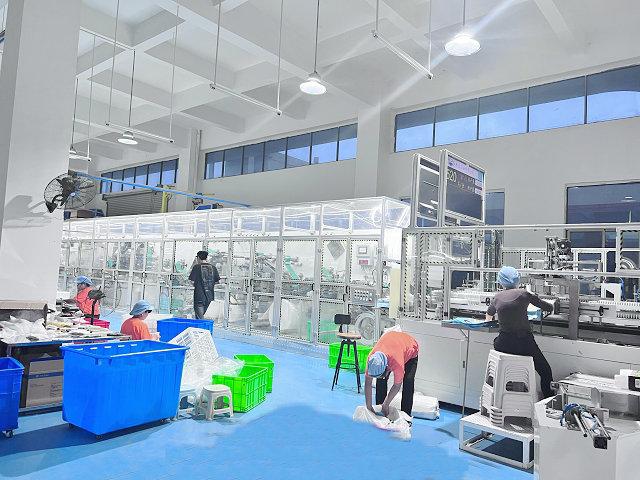
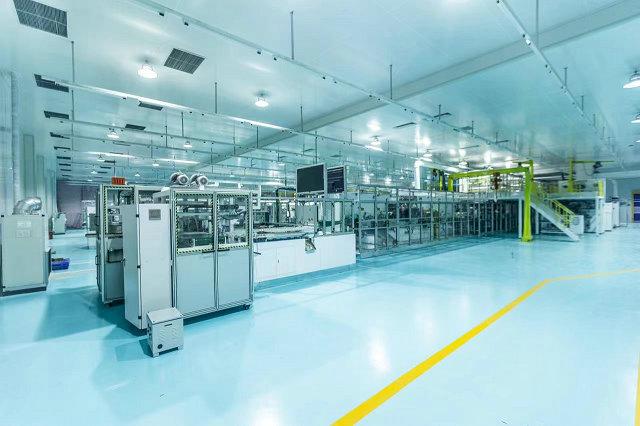
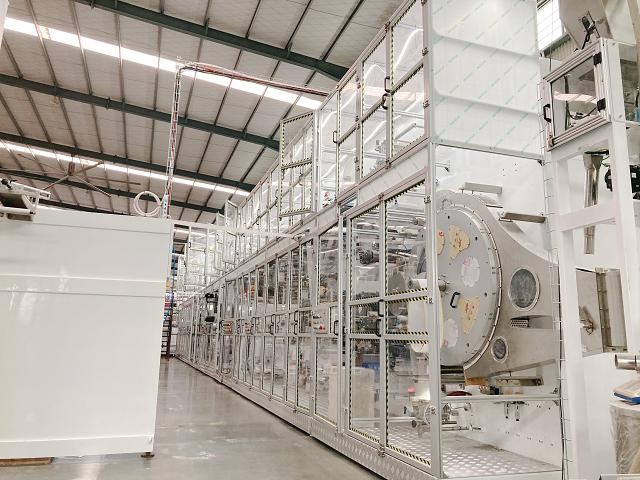
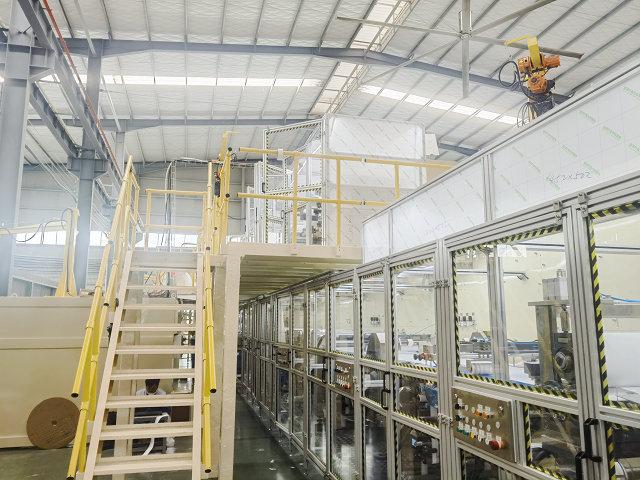
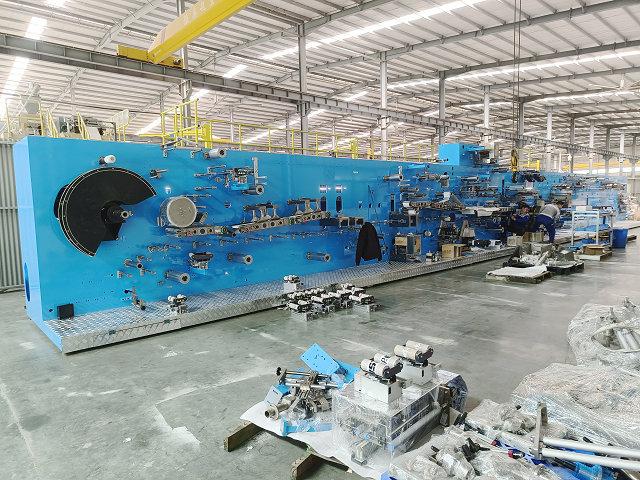
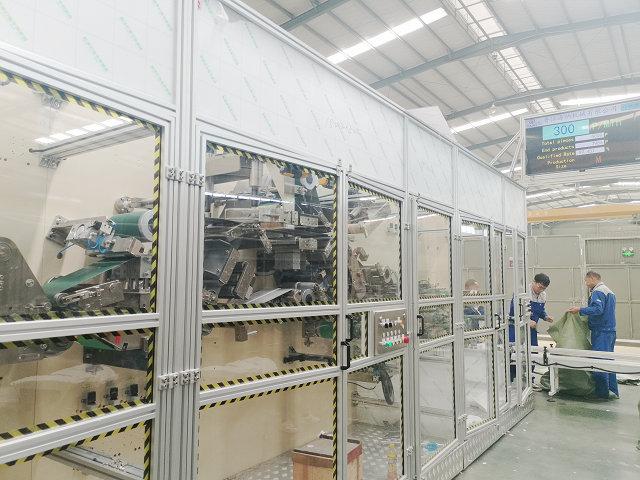
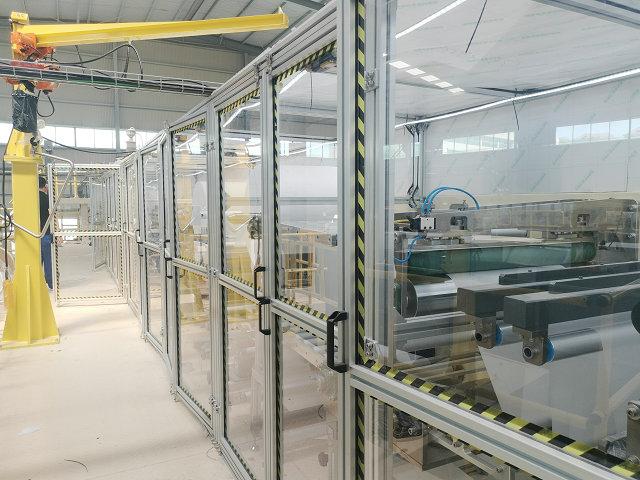
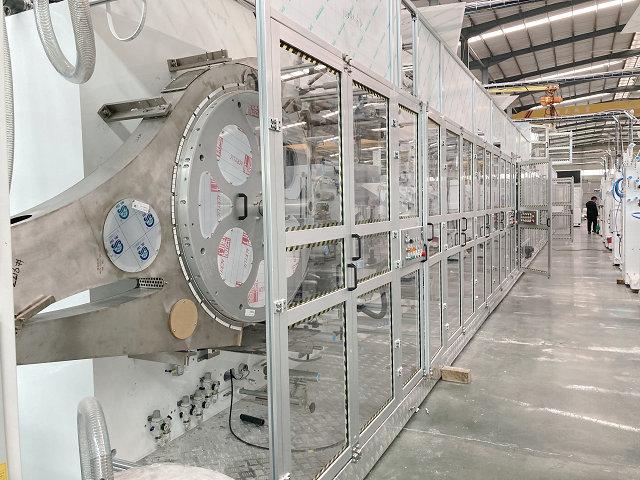
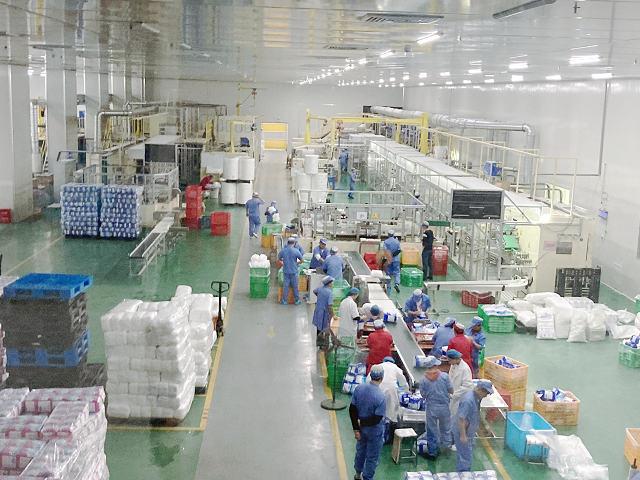
The page titled Full Automato Baby Diaper Production Line Video is a starting point for examining taped baby diaper equipment. Here the main questions concern maintenance access, then roll entry and splice recovery, with process continuity treated as a separate application decision. HAINA keeps the published title and media link while adding a testable review path.
Ask the production, quality and maintenance teams to watch together when studying the Full automatic Baby Diaper Production Line footage; keep open questions beside the relevant application document.
Ask the production, quality and maintenance teams to watch together for Full automatic Baby Diaper Production Line
The camera records one operating condition, while the contract must cover the agreed range. For this page, follow the path from core formation and wrap to cutting, folding and discharge. The packaging engineer should concentrate on counting, accumulation, bag presentation and rejected-product routing while another reviewer notes every edit, intervention or hidden transfer.
Core formation and wrapFor Full automatic Baby Diaper Production Line, check the handoff toward chassis lamination and link the observation to fastening registration.
Chassis laminationFor Full automatic Baby Diaper Production Line, observe the handoff toward elastic and cuff placement and link the observation to leg-cuff symmetry.
Elastic and cuff placementFor Full automatic Baby Diaper Production Line, trace the handoff toward tape or ear registration and link the observation to finished dimensions.
Tape or ear registrationFor Full automatic Baby Diaper Production Line, verify the handoff toward cutting, folding and discharge and link the observation to fold condition.
Cutting, folding and dischargeFor Full automatic Baby Diaper Production Line, document the handoff toward core formation and wrap and link the observation to core position.
Primary evidence at maintenance access
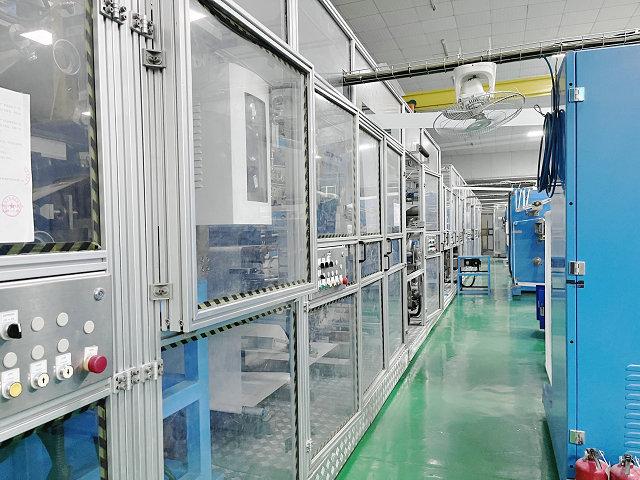
Routine access affects uptime long after commissioning. The camera can help a maintenance team locate tight stations before the layout is frozen. Applied to Full automatic Baby Diaper Production Line, this means comparing the filmed condition with core position and leg-cuff symmetry on samples from the same operating period.
For the destination plant, confirm lubrication route and connect it to the finished-product finding for fastening registration on Full automatic Baby Diaper Production Line.
The team should inspect cleaning access, then retain the corresponding Full automatic Baby Diaper Production Line sample used to assess leg-cuff symmetry.
For Full automatic Baby Diaper Production Line, note belt and sensor replacement before judging finished dimensions at the next sampling point.
Around space around glue and cutting units, check the system condition and the later fold condition outcome instead of relying on appearance.
Evidence gap: The earlier text for Full automatic Baby Diaper Production Line did not provide a usable measured value. Ask for a timed run that identifies the SKU, qualified material lots, approved output, stops and rejects instead of inferring performance from screen speed.
Process continuity for this project
A line recording is most informative when each filmed stage can be matched to the process drawing and the next physical handoff. In the case of Full automatic Baby Diaper Production Line, request a process drawing matched to a continuous acceptance run. Keep the answer separate from the footage so an optional module or untested value is not mistaken for approved scope.
Review layer
Page-specific check
Film observation
Follow chassis lamination and mark the transition into elastic and cuff placement for Full automatic Baby Diaper Production Line.
First measurement
At maintenance access, check space around glue and cutting units against fastening registration.
Independent review
Have the packaging engineer examine roll entry and splice recovery for counting, accumulation, bag presentation and rejected-product routing.
Document request
Request a process drawing matched to a continuous acceptance run and approved packed output with maker and packer stops classified separately for the Full automatic Baby Diaper Production Line application file.
Acceptance note
For Full automatic Baby Diaper Production Line, retain samples showing finished dimensions near maintenance access and reconcile them with stops, splices and approved downstream output.
Second pass at roll entry and splice recovery
Roll entry reveals whether material preparation and splice handling are treated as part of normal production rather than as an interruption outside the test. This second lens is deliberately different from maintenance access: for Full automatic Baby Diaper Production Line, it should produce a splice log connected to retained samples and reject counts, with the finding reviewed by the packaging engineer.
Before accepting the observation, observe roll orientation and core size and connect it to the finished-product finding for finished dimensions on Full automatic Baby Diaper Production Line.
The team should verify reference edge and guide position, then retain the corresponding Full automatic Baby Diaper Production Line sample used to assess fold condition.
For Full automatic Baby Diaper Production Line, document buffer storage used during a splice before judging core position at the next sampling point.
Around product condition immediately after the joint, assess the system condition and the later fastening registration outcome instead of relying on appearance.
For Full automatic Baby Diaper Production Line, the packaging engineer should use maker-to-packer handoff as a third cross-check after reviewing maintenance access. A line is only as productive as the transfer between the maker and the packer. Counting, accumulation and recovery should be reviewed as one process. Add approved packed output with maker and packer stops classified separately only when that responsibility is included in the intended line.
Questions raised by the Full automatic Baby Diaper Production Line recording
What does the Full automatic Baby Diaper Production Line footage show well?
It helps locate core formation and wrap, maintenance access and cutting, folding and discharge. For this Full automatic Baby Diaper Production Line review, it does not by itself establish core position over time or confirm the roll entry and splice recovery responsibility outside the camera view.
Which follow-up matters most for Full automatic Baby Diaper Production Line?
Ask for the preventive-maintenance plan, access drawing and first-year spares list. Match that note to the same materials and SKU shown during the Full automatic Baby Diaper Production Line review so that the observation and finding describe one run.
How should a buyer use this taped baby diaper video?
Use it to prepare questions for roll entry and splice recovery, process continuity and core position. Close those questions through drawings, retained samples and signed acceptance results.
Close the review with traceable evidence
File this recording with the product sample, material list, process drawing, line layout, utility schedule and FAT method for Full automatic Baby Diaper Production Line. Number each open item under maintenance access, roll entry and splice recovery or process continuity; assign an owner and the evidence needed to close it.
Before the equipment scope is signed, HAINA can compare the filmed arrangement with the intended module list for Full automatic Baby Diaper Production Line. Final acceptance should use qualified materials, agreed measurement methods and retained results from the named test run, including any finding connected to maker-to-packer handoff.