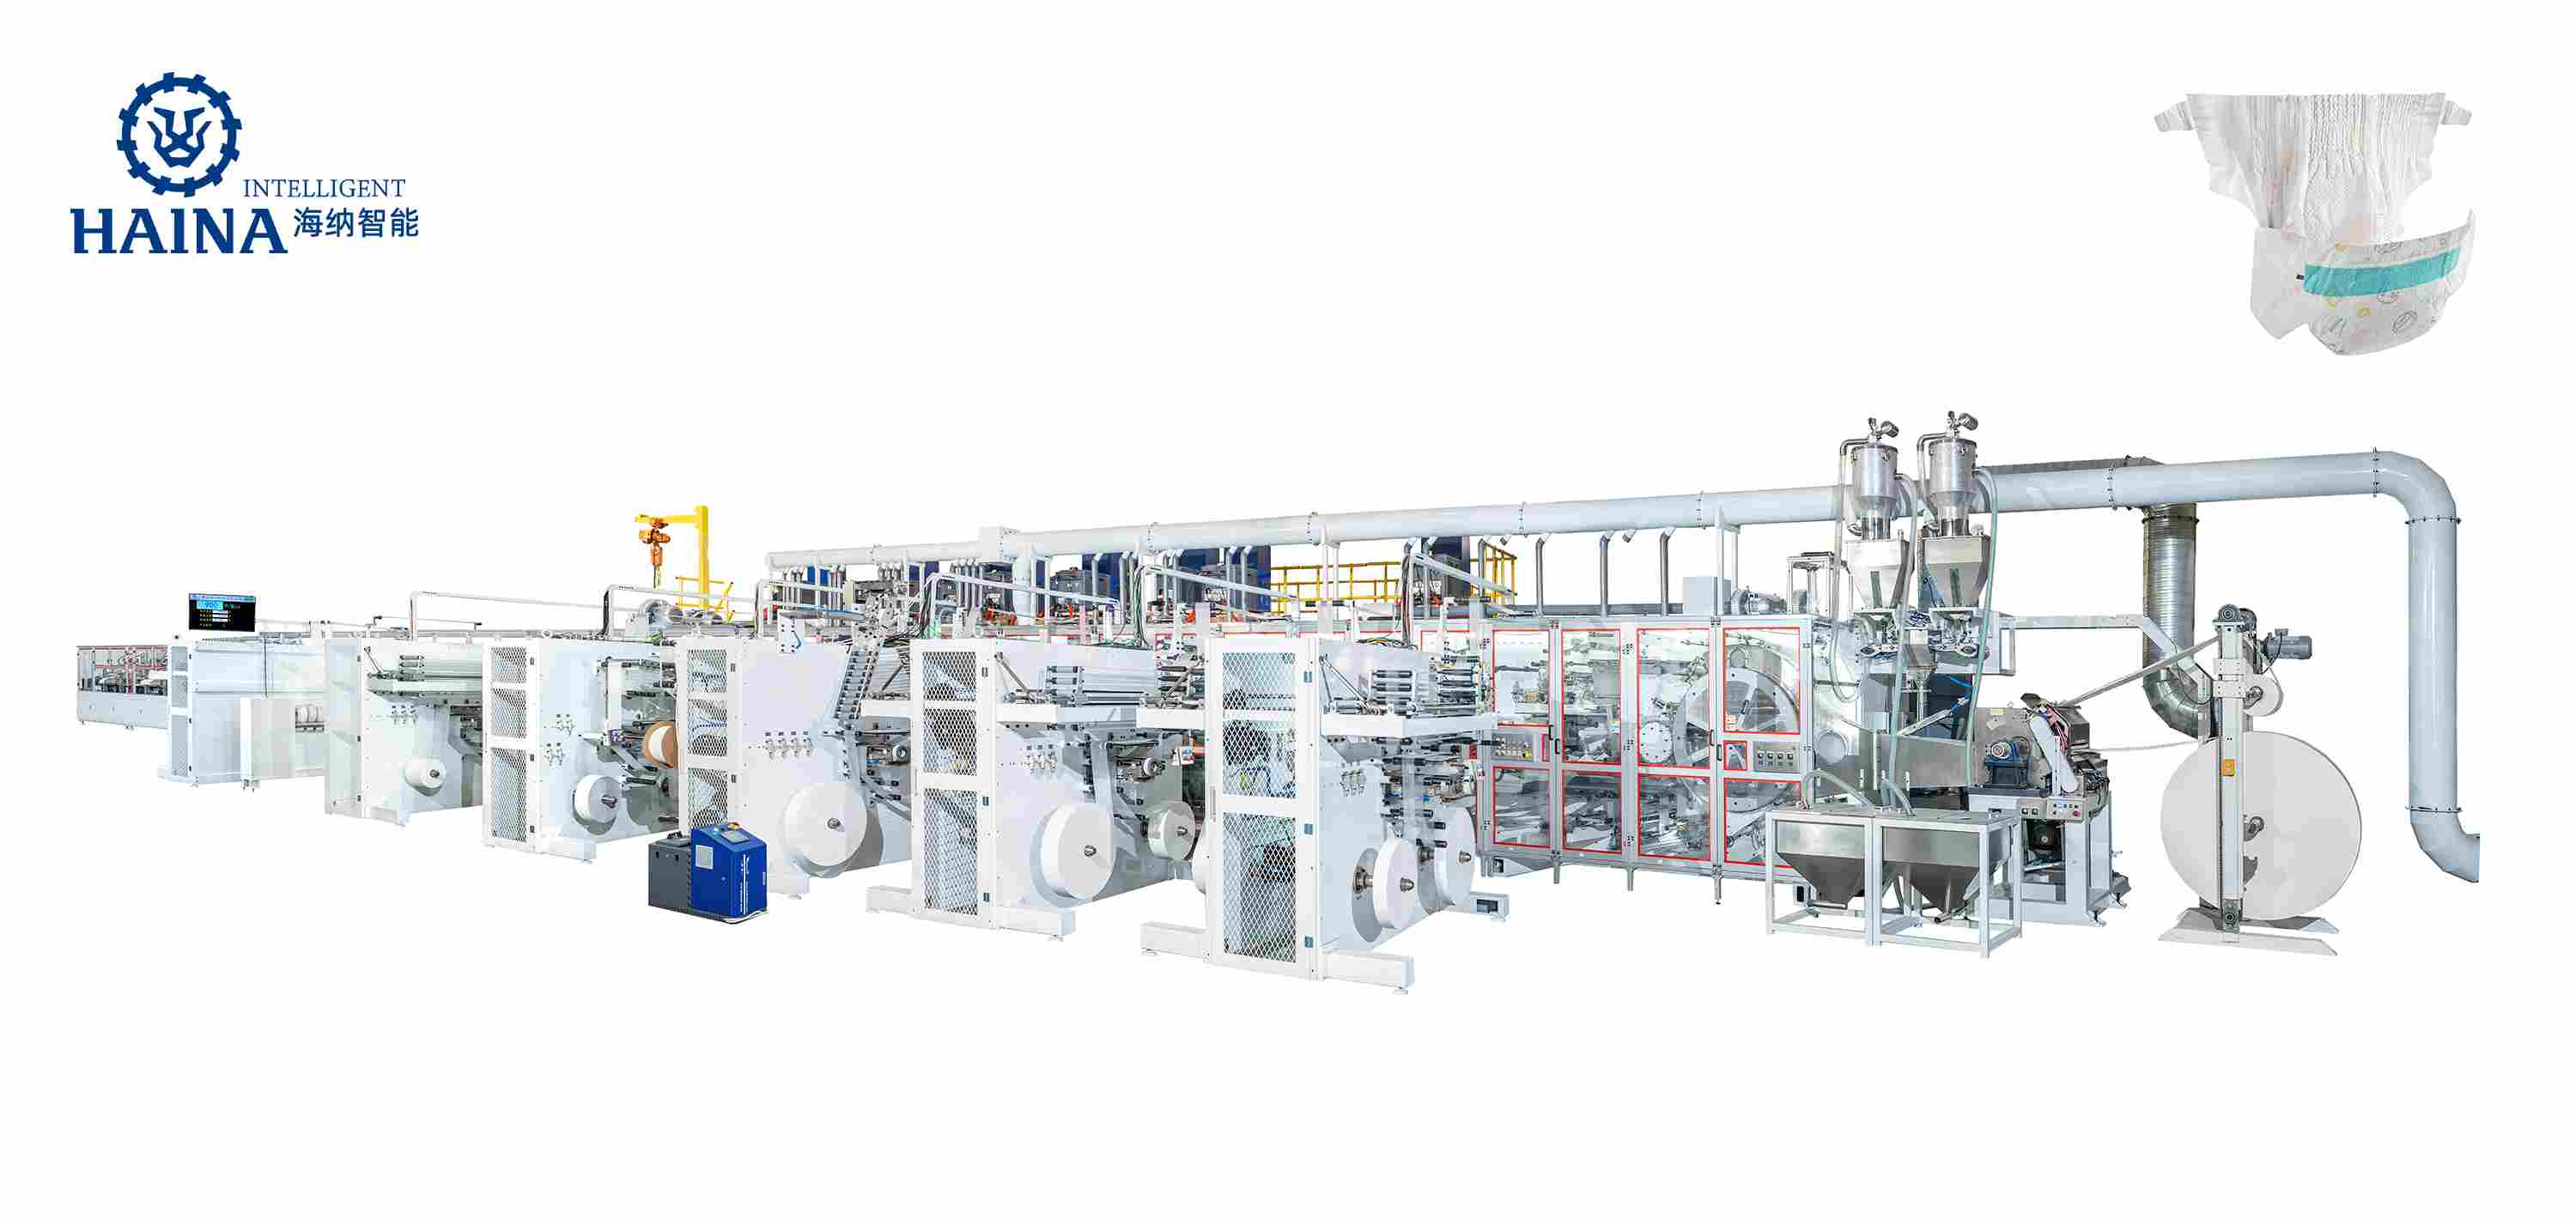
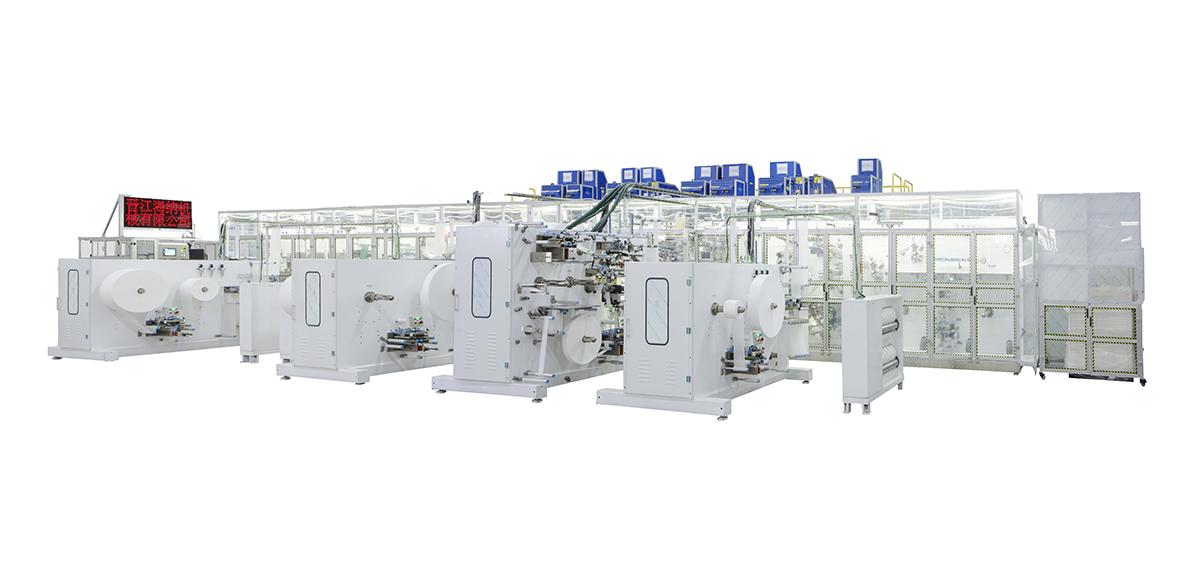
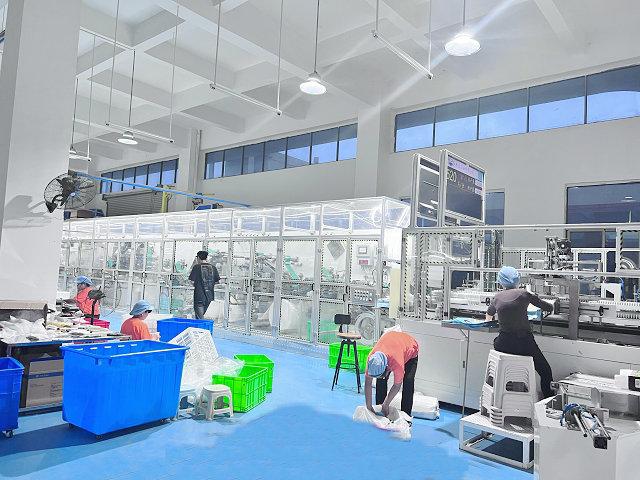
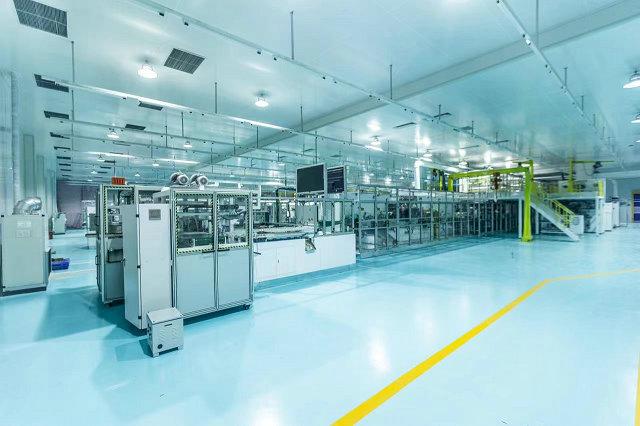
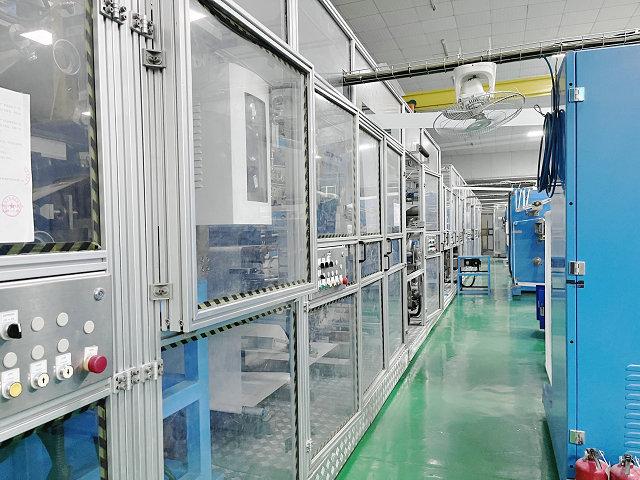
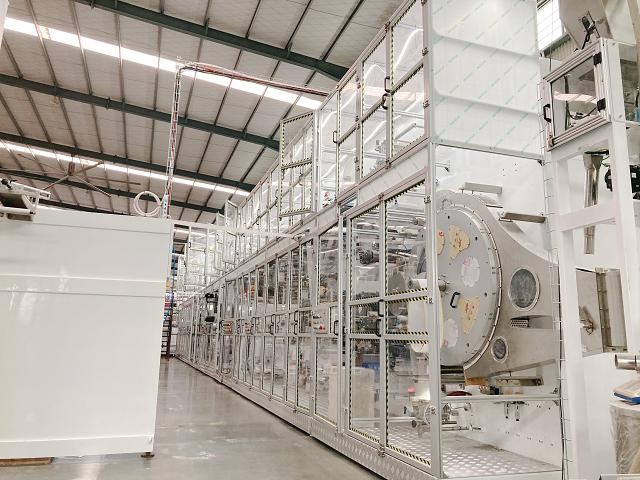
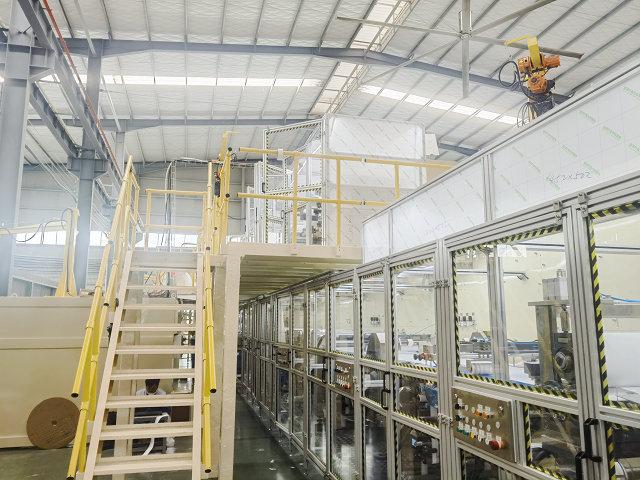
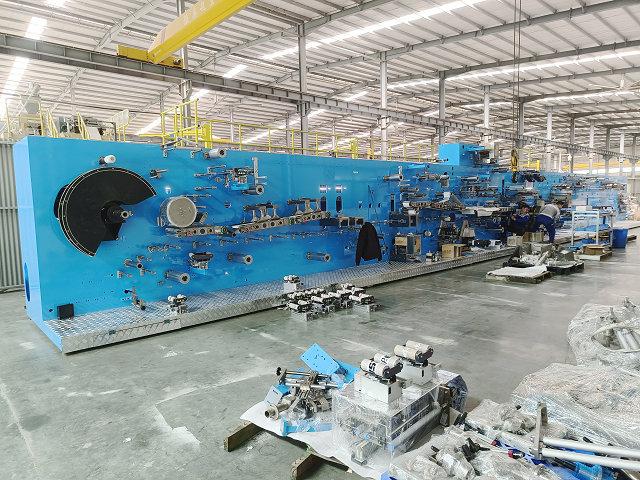
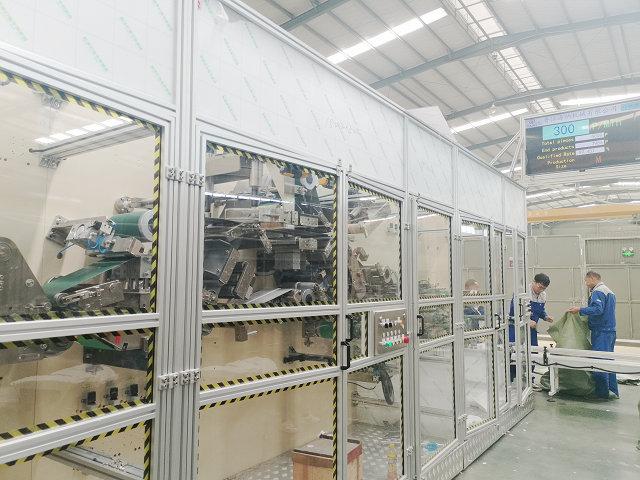
On the guide titled Best diaper production line Manufacturer Video, watch the disposable absorbent product route through two specific lenses: maker-to-packer handoff and timed acceptance data. The commercial lens is quality verification. HAINA uses the guide to connect filmed movement with documents, material trials and measurable factory acceptance work.
Start at the unwind and follow one product pitch forward when studying the diaper production line recording; keep open issues beside the relevant project document.
Start at the unwind and follow one product pitch forward for diaper production line
What looks aligned on screen may still need a measured datum on the finished article. For this guide, follow the path from raw-material feeding to counting and discharge. The process engineer should concentrate on material references, driven relationships and product tolerances while another reviewer notes every edit, intervention or hidden transfer.
Raw-material feedingFor diaper production line, note the handoff toward absorbent structure preparation and link the observation to absorbent structure.
Absorbent structure preparationFor diaper production line, follow the handoff toward multi-layer assembly and link the observation to component registration.
Multi-layer assemblyFor diaper production line, check the handoff toward product shaping and link the observation to finished dimensions.
Product shapingFor diaper production line, observe the handoff toward counting and discharge and link the observation to accepted output.
Counting and dischargeFor diaper production line, trace the handoff toward raw-material feeding and link the observation to material tracking.
Primary evidence at maker-to-packer handoff
A line is only as productive as the transfer between the maker and the packer. Counting, accumulation and recovery should be reviewed as one process. Applied to diaper production line, this means comparing the filmed condition with material tracking and component registration on samples from the same operating period.
Around maker discharge spacing, note the system condition and the later absorbent structure outcome instead of relying on appearance.
Use counter response as the observation; use component registration as the measured result for this diaper production line review.
On the project drawing, examine accumulation behavior and connect it to the finished-product result for finished dimensions on diaper production line.
The team should observe restart after a downstream stop, then retain the corresponding diaper production line sample used to assess accepted output.
Evidence gap: The earlier text for diaper production line did not provide a usable measured value. Ask for a timed run that identifies the SKU, approved material lots, accepted output, stops and rejects instead of inferring performance from screen speed.
Quality evidence for this project
The project file should turn appearance claims into measurable product features and agreed acceptance limits. In the case of diaper production line, request a signed control plan and retained samples from the measured run. Keep the answer separate from the recording so an optional module or untested value is not mistaken for accepted scope.
Review layer
Guide-specific check
Film observation
Follow absorbent structure preparation and mark the transition into multi-layer assembly for diaper production line.
First measurement
At maker-to-packer handoff, check counter response against absorbent structure.
Independent review
Have the process engineer examine timed acceptance data for material references, driven relationships and product tolerances.
Document request
Request a signed control plan and retained samples from the measured run and a splice log connected to retained samples and reject counts for the diaper production line project file.
Acceptance note
For diaper production line, retain samples showing finished dimensions near maker-to-packer handoff and reconcile them with stops, splices and accepted downstream output.
Second pass at timed acceptance data
Video can show motion, but investment decisions depend on a timed run with a known SKU, approved materials and reconciled counters. This second lens is deliberately different from maker-to-packer handoff: for diaper production line, it should produce a signed FAT sheet that reconciles input time, system counters and accepted packs, with the result reviewed by the process engineer.
Around start and finish time, document the system condition and the later finished dimensions outcome instead of relying on appearance.
Use accepted product count as the observation; use accepted output as the measured result for this diaper production line review.
During the timed window, compare stops and splices and connect it to the finished-product result for material tracking on diaper production line.
The team should review rejects and remaining work, then retain the corresponding diaper production line sample used to assess absorbent structure.
For diaper production line, the process engineer should use roll entry and splice recovery as a third cross-check after reviewing maker-to-packer handoff. Roll entry reveals whether material preparation and splice handling are treated as part of normal production rather than as an interruption outside the test. Add a splice log connected to retained samples and reject counts only when that responsibility is included in the intended line.
Questions raised by the diaper production line recording
What does the diaper production line footage show well?
It helps locate raw-material feeding, maker-to-packer handoff and counting and discharge. For this diaper production line review, it does not by itself establish material tracking over time or confirm the timed acceptance data responsibility outside the camera view.
Which follow-up matters most for diaper production line?
Ask for accepted packed output with maker and packer stops classified separately. Match that note to the same materials and SKU filmed during the diaper production line review so that the observation and result describe one run.
How should a buyer use this disposable absorbent product video?
Use it to prepare issues for timed acceptance data, quality verification and material tracking. Close those issues through drawings, retained samples and signed acceptance outcomes.
Close the review with traceable evidence
File this video with the product sample, material list, process drawing, line layout, utility schedule and FAT method for diaper production line. Number each open item under maker-to-packer handoff, timed acceptance data or quality verification; assign an owner and the verification needed to close it.
Before the equipment scope is signed, HAINA can compare the filmed arrangement with the intended module list for diaper production line. Final acceptance should use approved materials, agreed measurement methods and retained outcomes from the named test run, including any finding connected to roll entry and splice recovery.