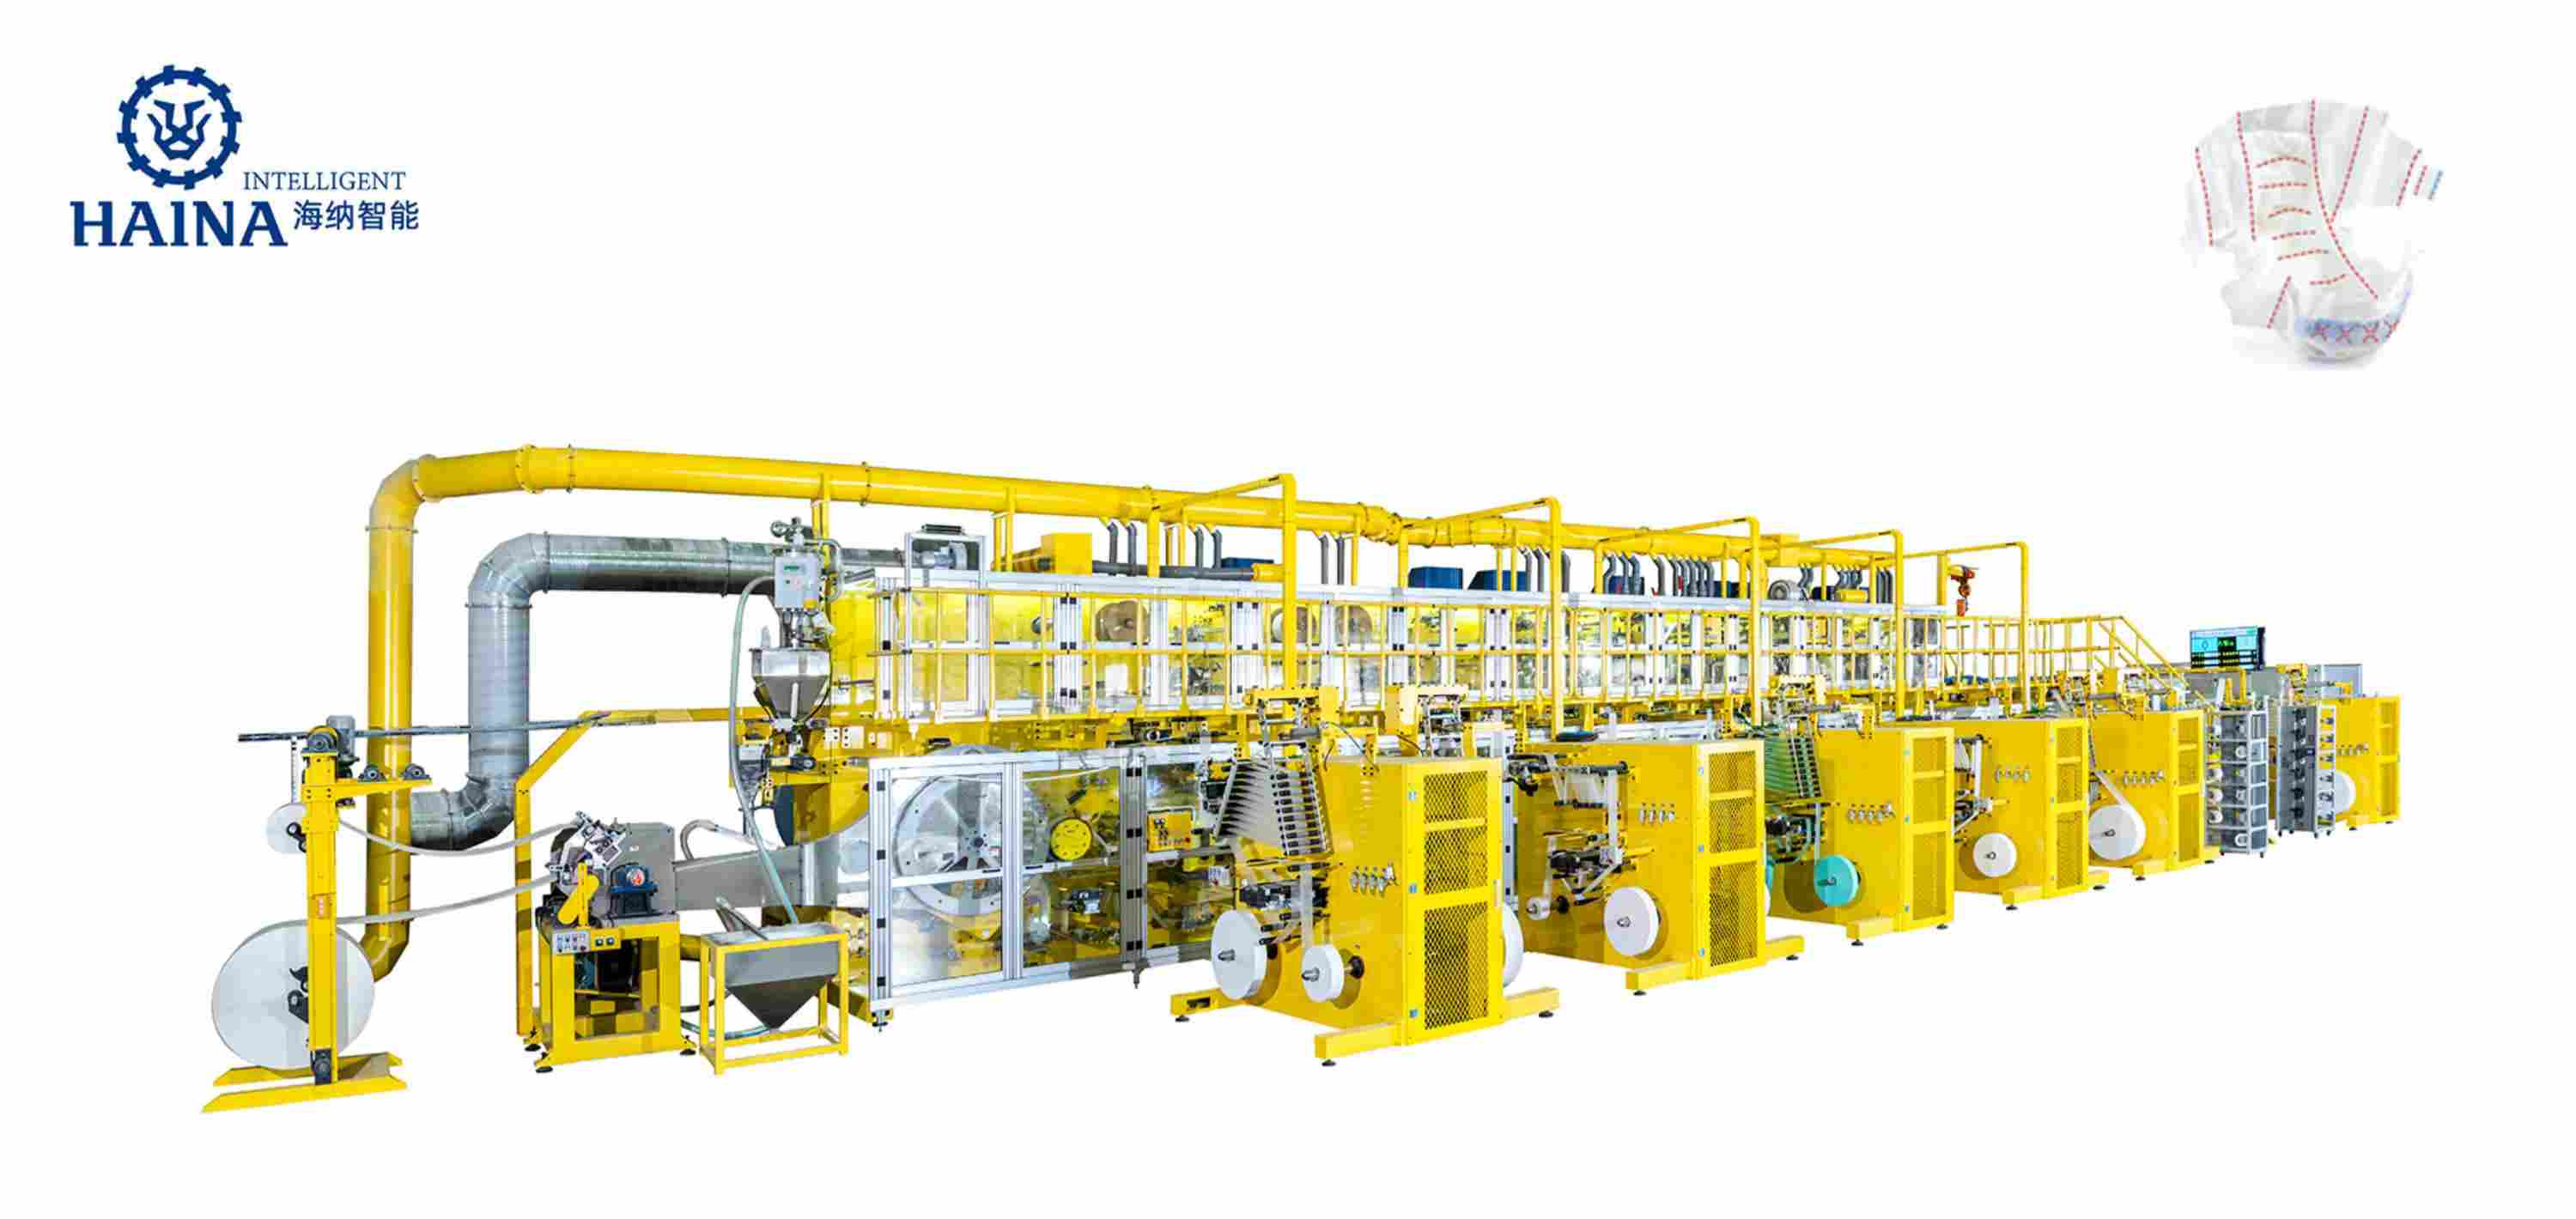
UNK600 is best understood as a sequence of controlled handoffs. The saved configuration combines servo drive, an HMI, buffered tension control, automatic web guiding and a full-surround waist structure. Each station can run, yet the finished diaper is acceptable only when the references carried from one station to the next remain aligned.

Identify the hydrophilic topsheet, hydrophobic leg-cuff nonwoven, ADL, fluff pulp, SAP, tissue or nonwoven wraps and PE film by supplier lot. Winding direction and roll edge should be recorded before loading.
The pulp, SAP and upper and lower wrap materials establish the core that later stations must hold in position. The approved sample and recipe provide the reference; the historical page does not state a universal dosage.
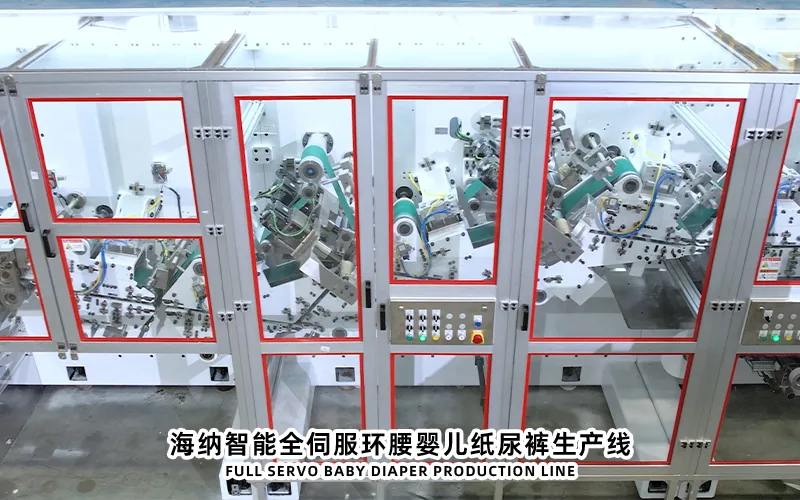
Topsheet, backsheet, leg-cuff materials, elastics and ADL meet around the core. Servo synchronization and digital size change are recorded functions, but every planned size still needs its own recipe and measured sample.
Nonwoven and elastic for the big waistband, together with the S-cut hook and glue materials listed in the source, create the defining U-shape construction. Registration after a splice or restart is a product-quality checkpoint, not merely a machine-motion check.
The old scope says the automatic stacker and packaging machine are to be defined by the customer. Pack count, discharge direction and communication with downstream equipment therefore belong in the project boundary.
The legacy description records a tension system with a buffer and automatic web guiding intended to support zero-speed splicing. That statement should be translated into a station list: which rolls can splice without stopping, where accumulation is available, which guide controls each web, and how many products are isolated after a join. A splice trial is complete only when the team records the roll, time, alarm response and first accepted diaper.
| Recorded item | Legacy value | Flow decision it affects |
|---|---|---|
| Design speed | 550 ppm | Mechanical reference for the configured route |
| Stable working speed | 450-500 ppm | Timed-run target to verify with named materials |
| Dimensions | 24 m x 4 m x 3.6 m | Unwind, service and downstream layout |
| Installed capacity | 300 kW | Electrical distribution planning |
| Air pressure | 0.6-0.8 MPa | Pneumatic supply check |
| Machine weight | 70 tons | Foundation, unloading and lifting plan |
The same table lists rejection at no more than 3 percent and efficiency at no less than 85 percent. Their counting rules are not defined in the old page, so HAINA should place the definitions, exclusions and sample interval in the signed FAT protocol.
Three references should meet at this station: the chassis centerline, the incoming waist-web edge and the elastic position after recovery. Inspection should include the first pieces after startup, every splice and every size change. A visually correct empty run does not replace a trial with the buyer's approved nonwoven, elastic, hook and adhesive grades.
The saved scope names an operating-side guard, emergency-stop switch, safety identification and a pull wire on the drive side. Acceptance should test each device in the state where it is intended to stop the line. The stacker and packer require a separate ownership table covering supply, controls, reject handling and recovery after a downstream stop.
No. It is recorded as design speed. The legacy stable working range is 450-500 ppm, and saleable output also depends on the agreed efficiency, rejection definitions, product size, materials and packaging boundary.
The historical text says the automatic stacker and packaging machine are to be defined by customer need. The final quotation must state exactly what is included.
Use the contracted waist nonwoven, elastic, hook and adhesive, then retain products before and after the splice. Position, recovery and reject handling should be measured against the approved sample.
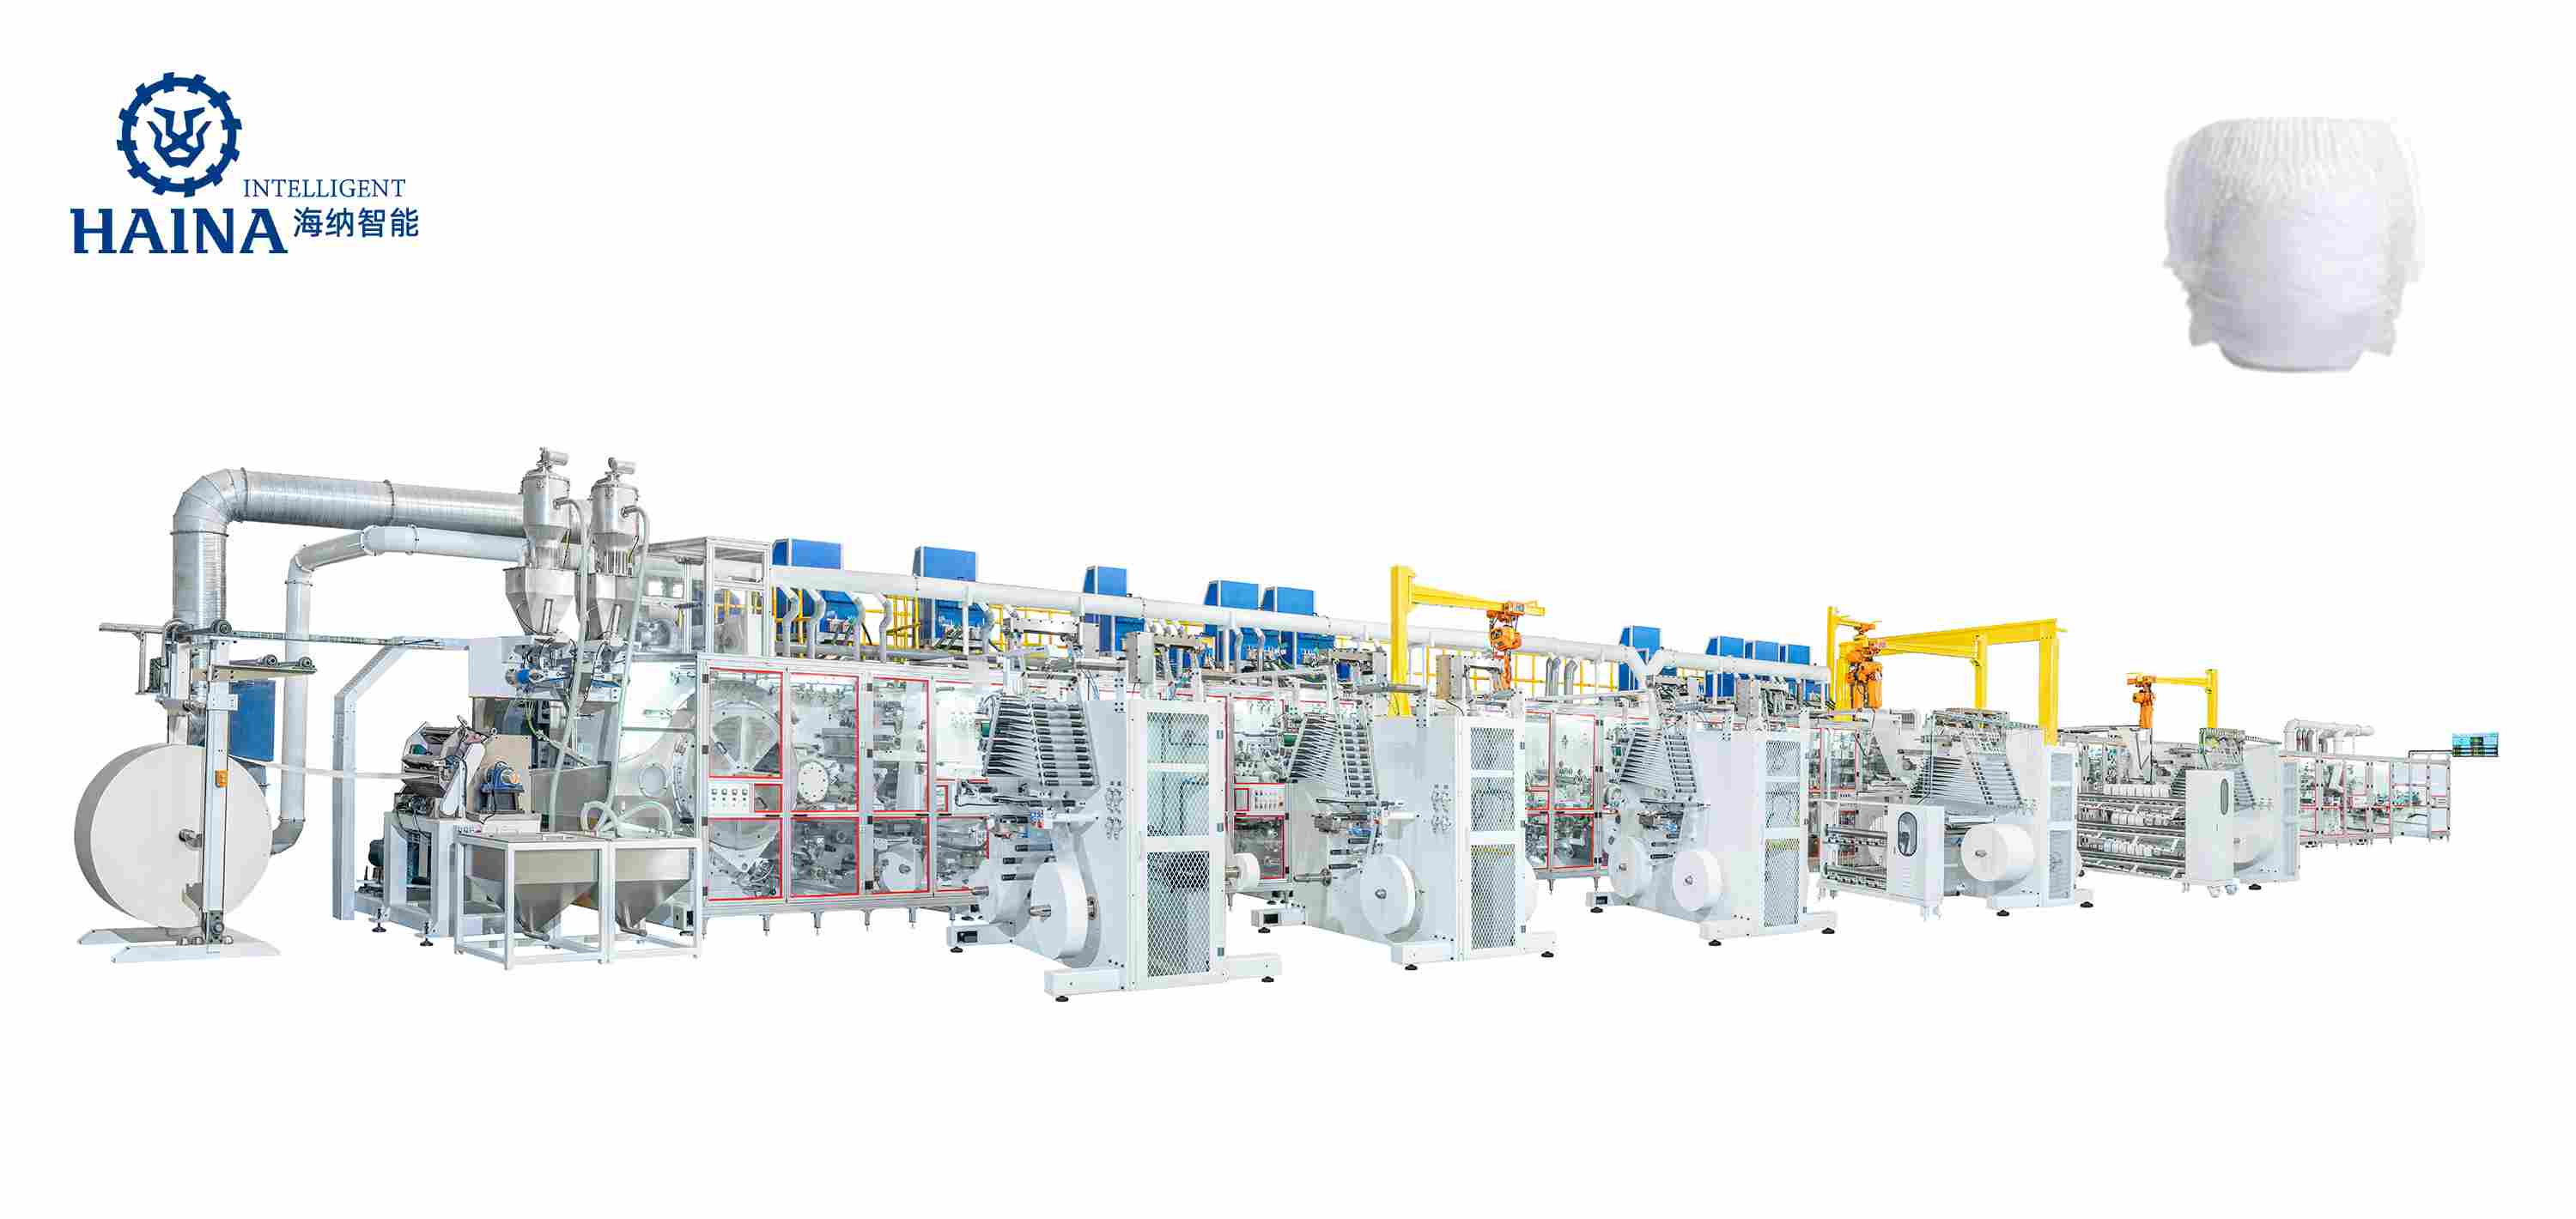
U-Shape Baby Diaper Production Line
|
Dimensions(L×W×H8) |
24m*4m*3.6m |
|
Design Speed: |
550ppm |
|
Stable Working Speed: |
450-500ppm |
|
Rejection Rate: |
≤3% |
|
Efficiency: |
≥85% |
|
Power Source: |
380V,50HZ |
|
Machine Capacity: |
300KW |
|
Air Pressure: |
0.6-0.8Mpa |
|
Machine Weight: |
70 tons |
U-Shape Baby Diaper Production Line Description:
The U-Shape Baby Diaper Production Line is a state-of-the-art manufacturing system designed for the efficient and automated production of high-quality baby diapers. This production line incorporates advanced technology and engineering expertise to provide a comprehensive solution for diaper manufacturers.
Technical Features:
1. Automated Production: The U-Shape Baby Diaper Production Line is equipped with advanced robotics and automation systems, ensuring fast and accurate production processes. This minimizes human intervention and maximizes efficiency.
2. Flexibility: This production line offers a high level of flexibility, allowing for easy customization and adjustment according to specific manufacturing requirements. It can produce various sizes and types of baby diapers, meeting the diverse demands of the market.
3. High-Speed Operation: With its optimized design and cutting-edge machinery, the U-Shape Baby Diaper Production Line achieves exceptional production speeds, significantly increasing output capacity and reducing production time.
4. Quality Control: This production line integrates reliable quality control mechanisms, ensuring that each diaper meets strict quality standards. It includes automated inspection systems for detecting defects and irregularities in real-time, guaranteeing consistent product excellence.
Baby Diaper Production Line Application:
The U-Shape Baby Diaper Production Line caters to the needs of manufacturers in the baby care industry. It is suitable for producing disposable baby diapers, ranging from newborn sizes to larger sizes for toddlers. This production line enables manufacturers to meet the growing demand for high-quality diapers in both domestic and international markets.
Key Functions:
1. Material Handling: The U-Shape Baby Diaper Production Line efficiently handles various raw materials such as absorbent cores, non-woven fabrics, and elastic bands, ensuring smooth production flow.
2. Cutting and Shaping: The production line precisely cuts and shapes the materials into the desired diaper design, including waistbands, leg cuffs, and absorbent cores, ensuring optimal fit and comfort for babies.
3. Fusion and Assembly: The components are securely fused and assembled using advanced bonding techniques, resulting in leak-proof and durable baby diapers.
4. Packaging: Once the diapers are manufactured, the production line automatically packages them into convenient packs, ready for distribution and retail.
Precautions:
1. Maintenance and Inspection: Regular maintenance and inspection of the U-Shape Baby Diaper Production Line are essential to ensure optimal performance and prolong its lifespan. Follow the manufacturer's guidelines for servicing and inspecting the machinery.
2. Safety Measures: Operators should strictly adhere to safety protocols while working with the production line, including wearing appropriate protective gear and avoiding contact with moving parts.
3. Training: Proper training of operators is crucial to maximize productivity, minimize errors, and ensure safe operation of the U-Shape Baby Diaper Production Line. Provide comprehensive training programs to ensure proficiency in operating and troubleshooting the equipment.
4. Quality Assurance: Implement rigorous quality control processes throughout the production process to maintain consistent product quality. Regularly monitor and adjust the production parameters to meet quality standards.
In summary, the U-Shape Baby Diaper Production Line is an innovative and efficient solution for manufacturers in the baby care industry. With its advanced technology, flexibility, high-speed operation, and emphasis on quality control, this production line enables seamless production of high-quality baby diapers, meeting the demands of both domestic and international markets. Taking necessary precautions and ensuring proper maintenance will ensure optimal performance and safe operation of the production line.
U-Shape Baby Diaper Production Line
| No. | Raw materials |
| 1 | Hydrophilic NW (Topsheet) |
| 2 | Hydrophobic NW (Legcuff) |
| 3 | Elastic for Legcuff |
| 4 | ADL |
| 5 | Fluff pulp |
| 6 | SAP |
| 7 | Upper tissue/NW |
| 8 | Lower tissue/NW |
| 9 | Pe film |
| 10 | NW for laminating |
| 11 | Frontal tape |
| 12 | NW for S cut |
| 13 | Hook for S cut |
| 14 | Glue for S cut |
| 15 | NW for big waistband |
| 16 | Elastic for big waistband |
| 17 | Construction glue |
| 18 | Elastic glue |
| 19 | Wetness indicator glue |


Understand LKQ1000 full-servo Q-shape baby pant controls, web handling, ultrasonic waist sealing, safety, utilities and acceptance checks....

Trace the TK900 full-servo T-shape diaper line from material unwinds and PLC-controlled forming to folding, alarms and auto-bagger scope....

This isMenstrual Pad Machine, also can produce adult pant machine from this machine. The structure is pulp type and ultra thin type, with dual legcuff, can...

Pampers Nappies Manufacturers South Africa. This machine design speed is 700pcs/minm,stable working speed is 600pcs/min. This machine is lastest technolo...


The Baby Diaper machine technical support provided by the manufacturer has been excellent, ensuring that our production runs smoothly without any hiccups.amy 2024-05-30
The Baby Diaper Machine is easy to operate and requires minimal maintenance, saving us time and resources. It's definitely worth the investment.Ethen 2024-05-30
The Baby Diaper Machine efficient, reliable, and produces high-quality diapers consistentlyjone 2024-05-30
The reliability of the Baby Diaper Machine has given us peace of mind. We can fulfill orders on time without worrying about breakdowns or delays.Henry 2024-05-30