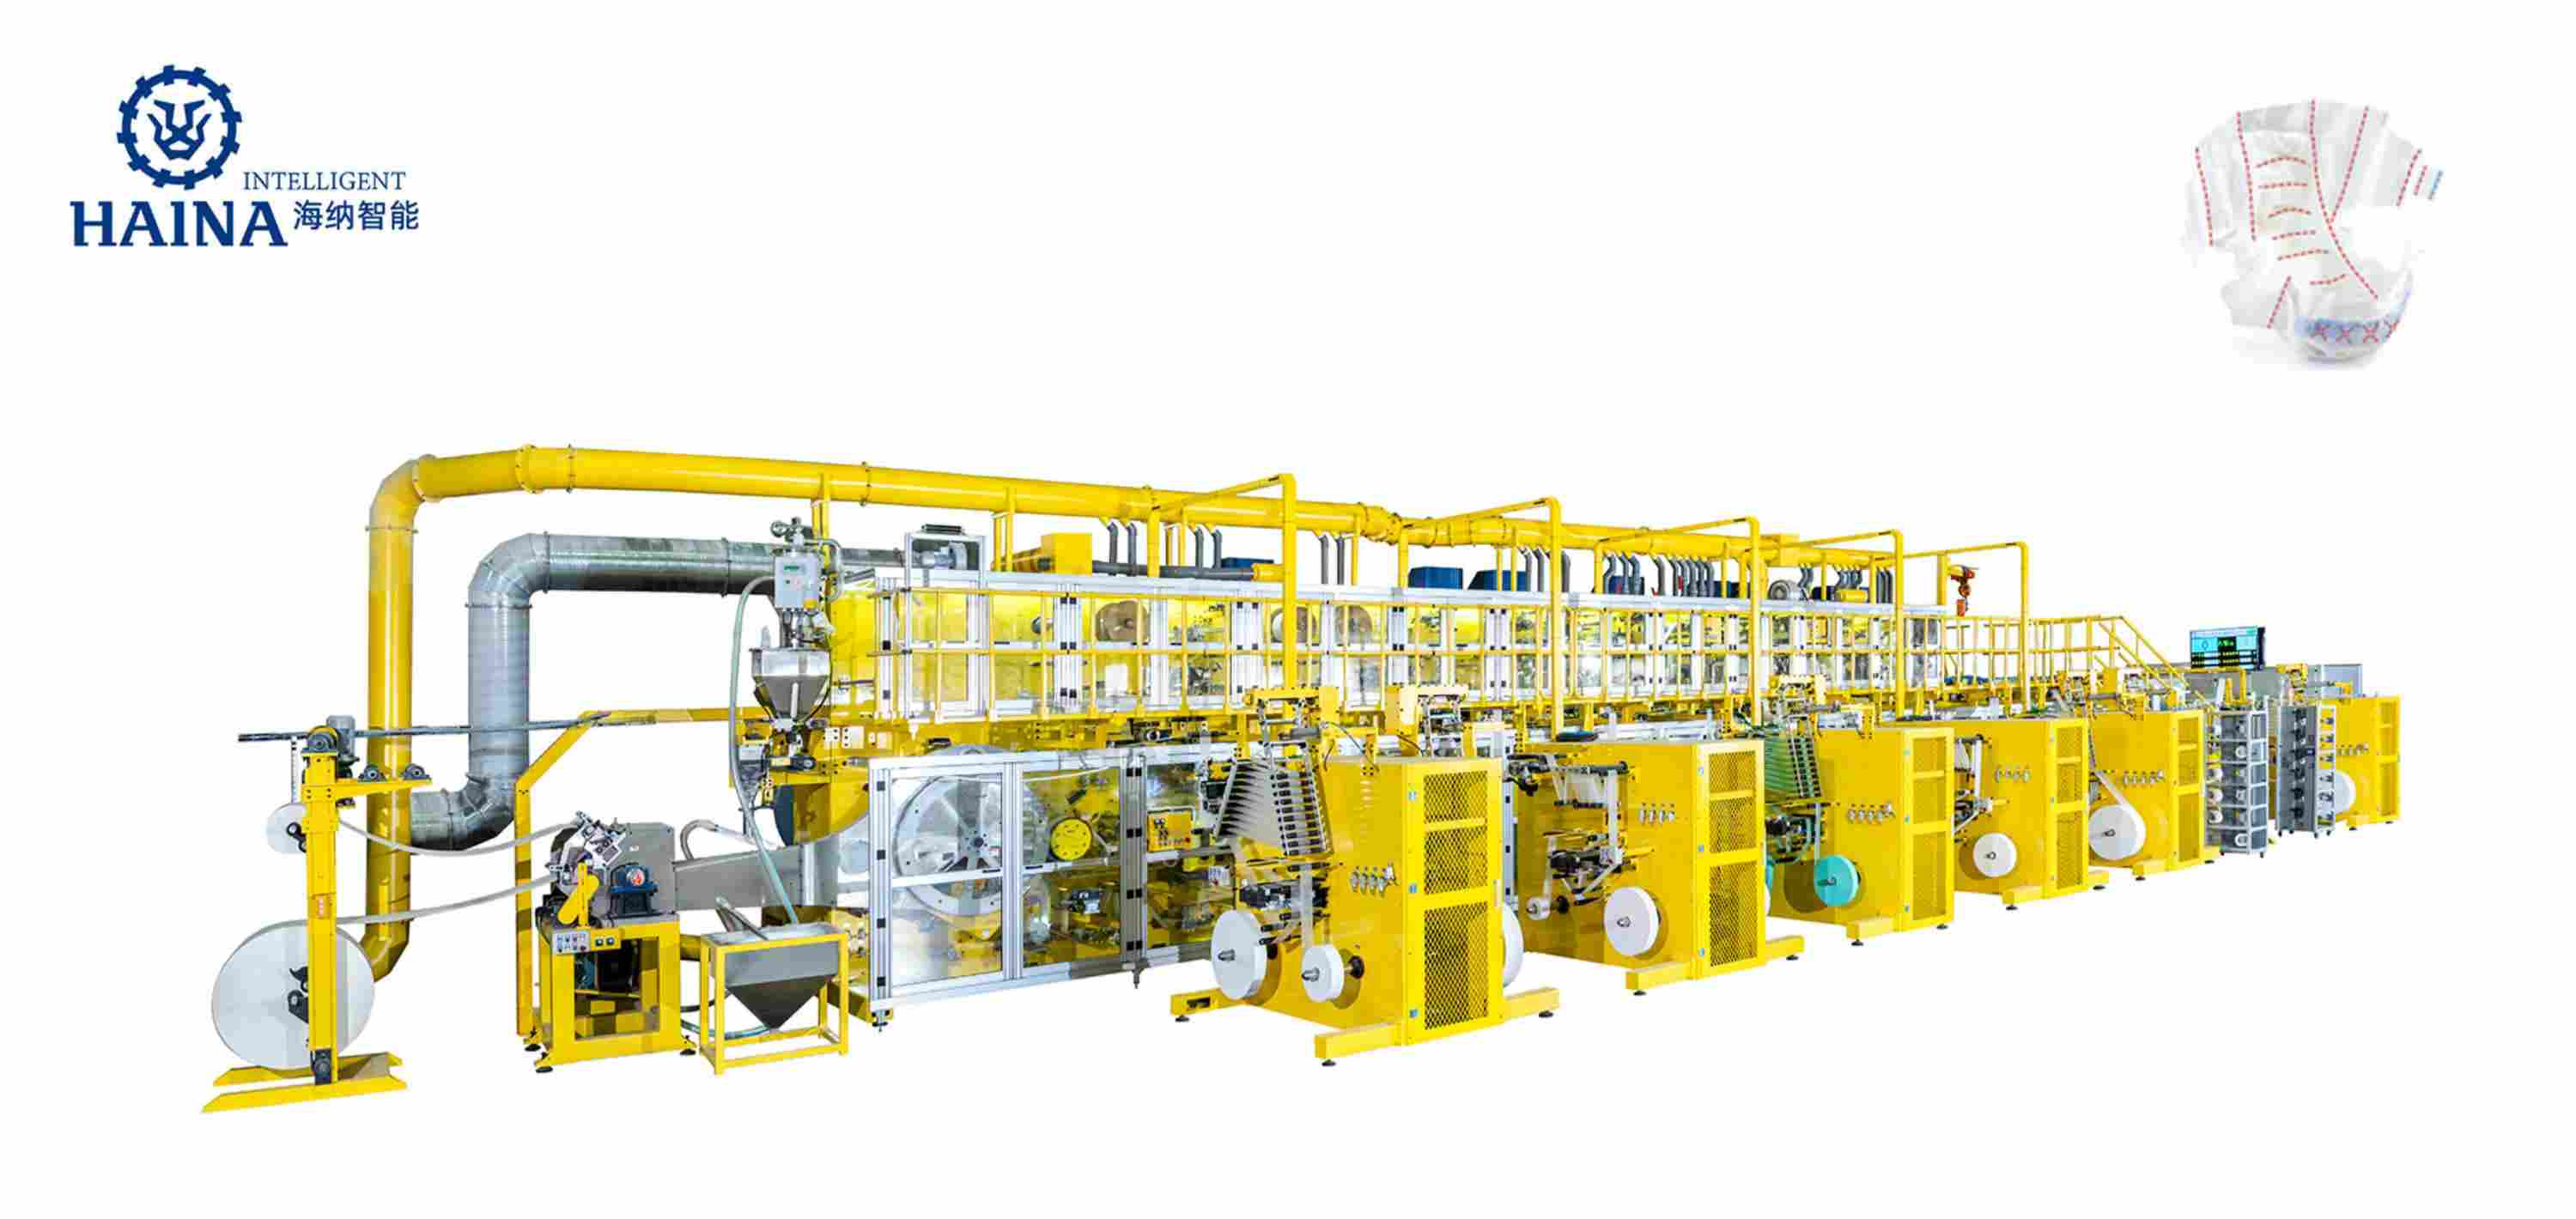
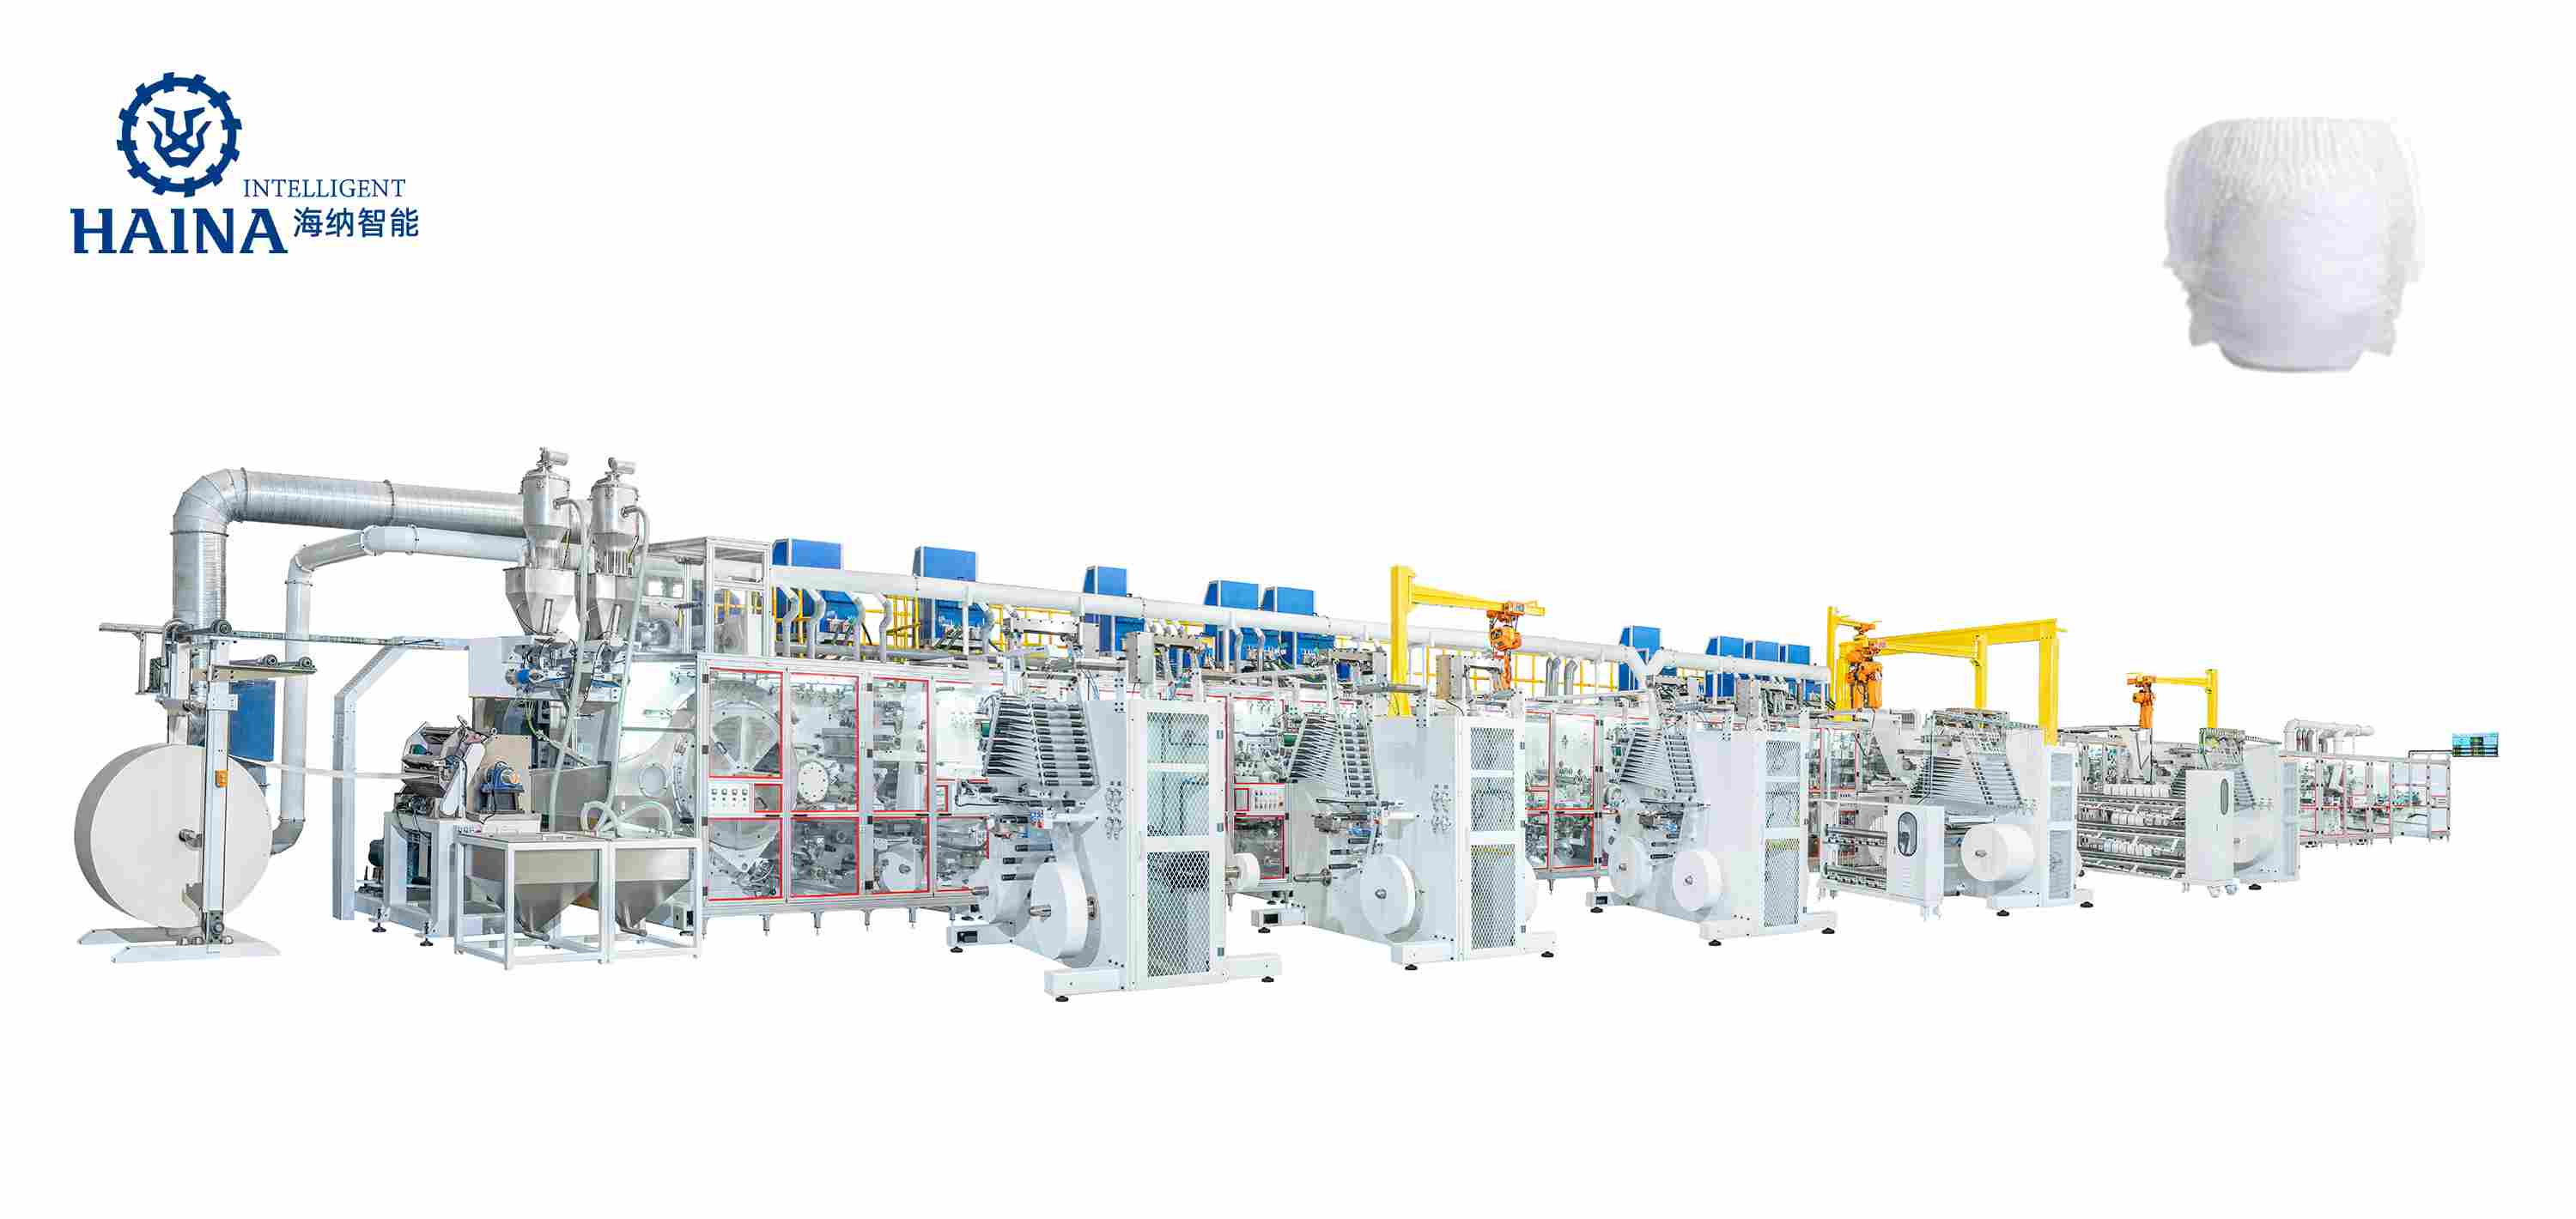
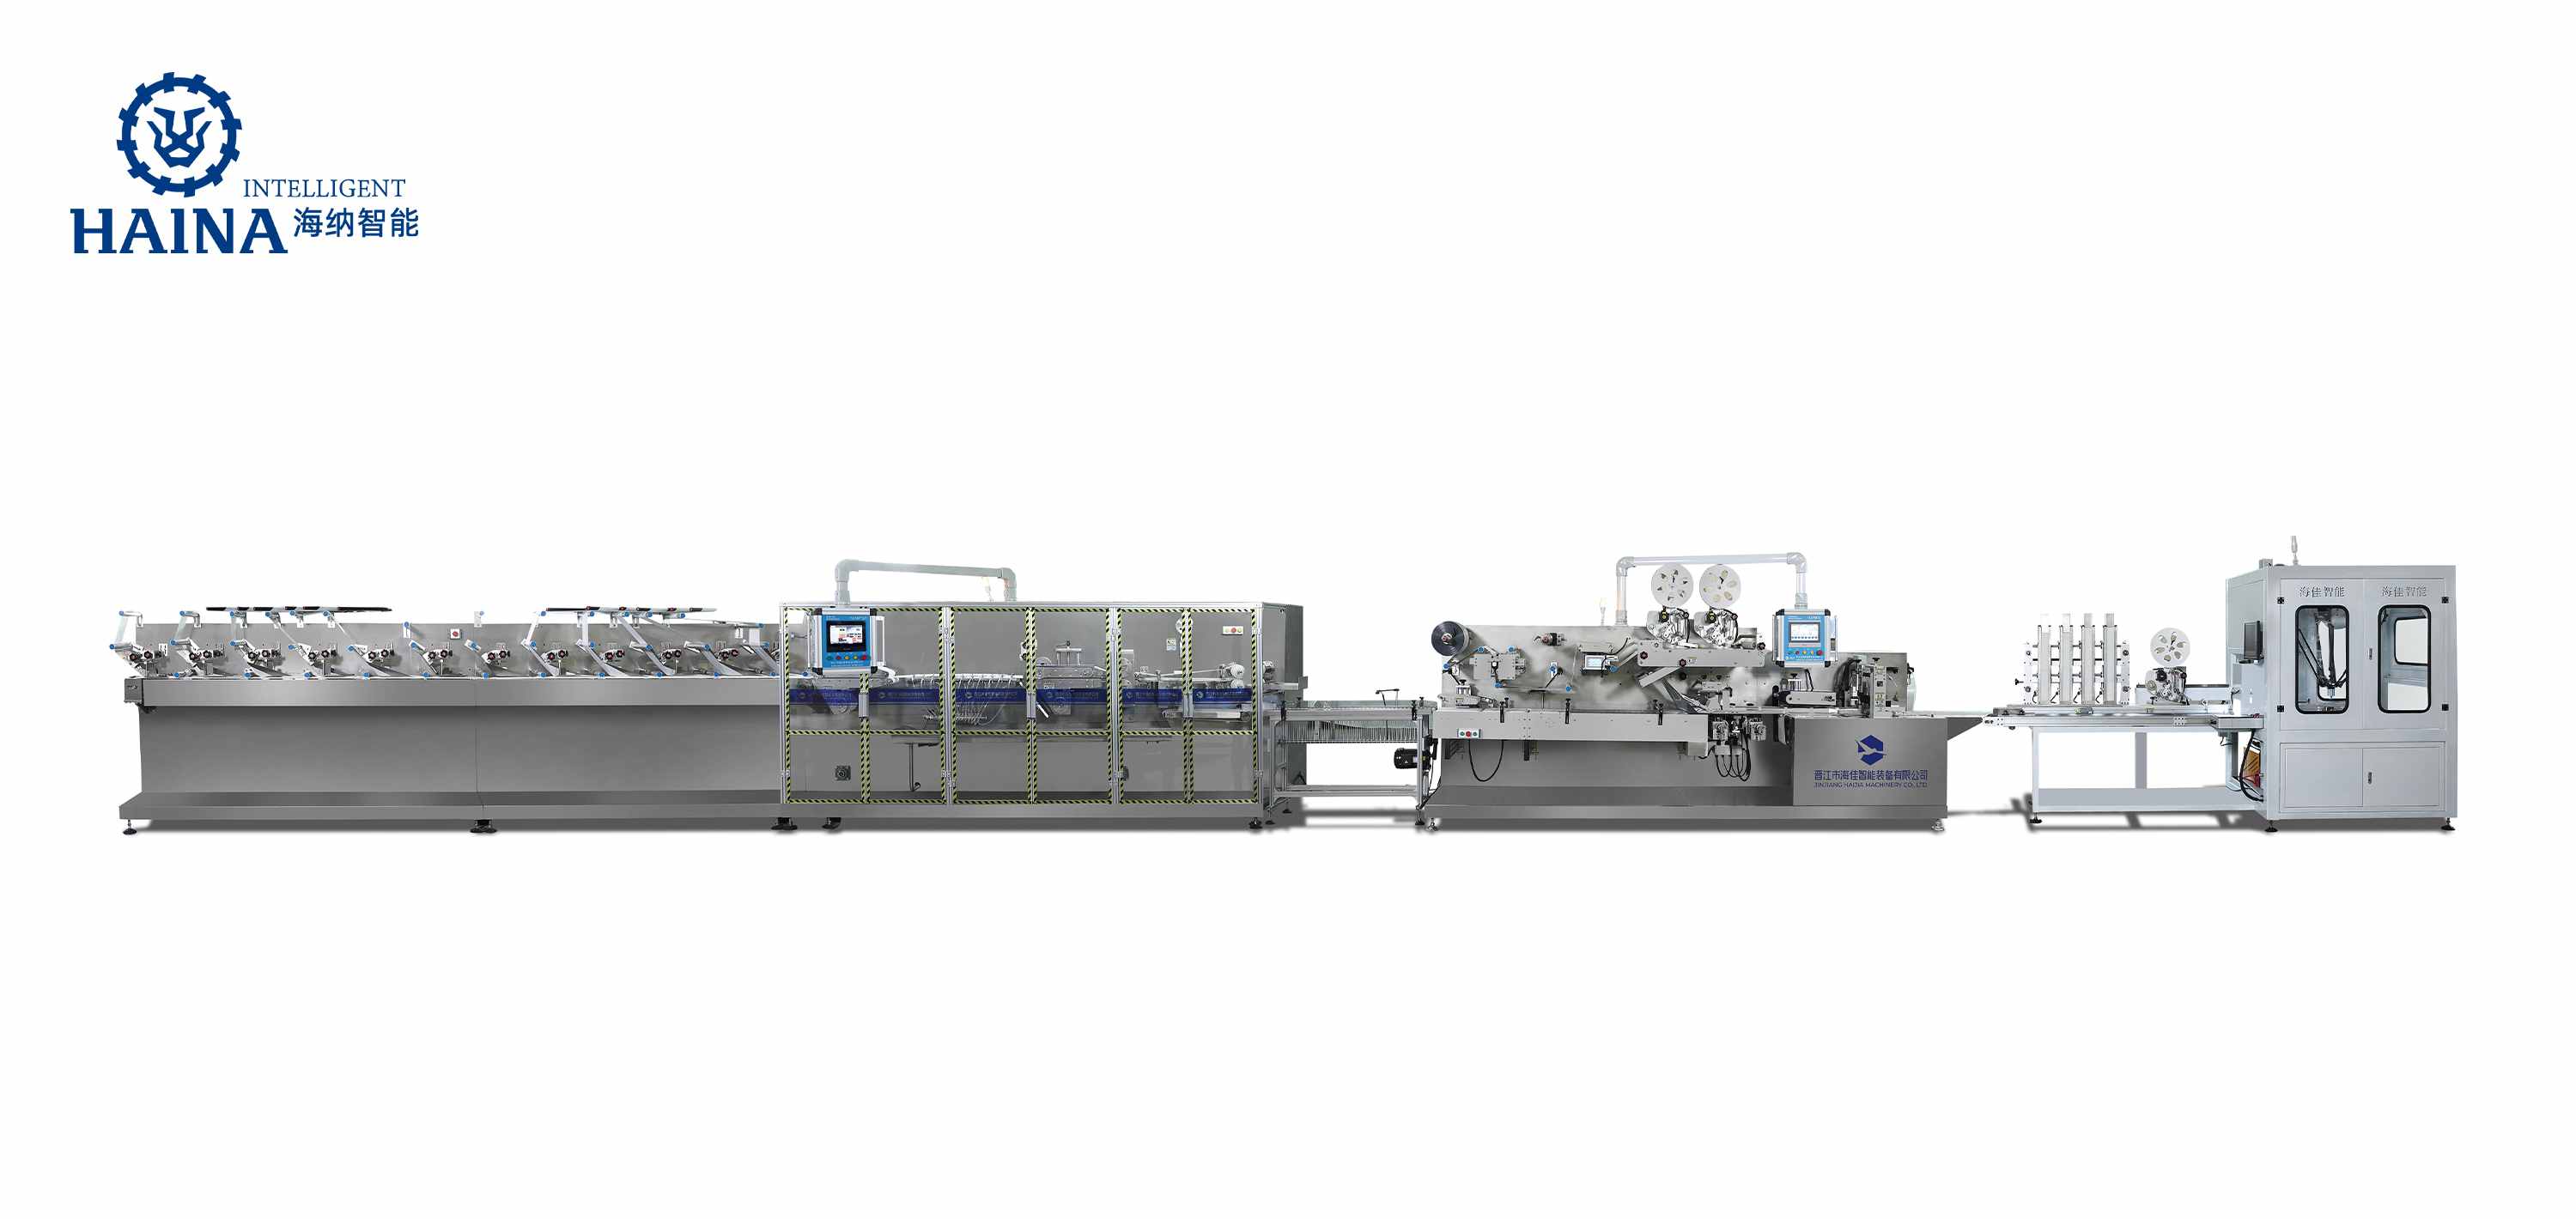
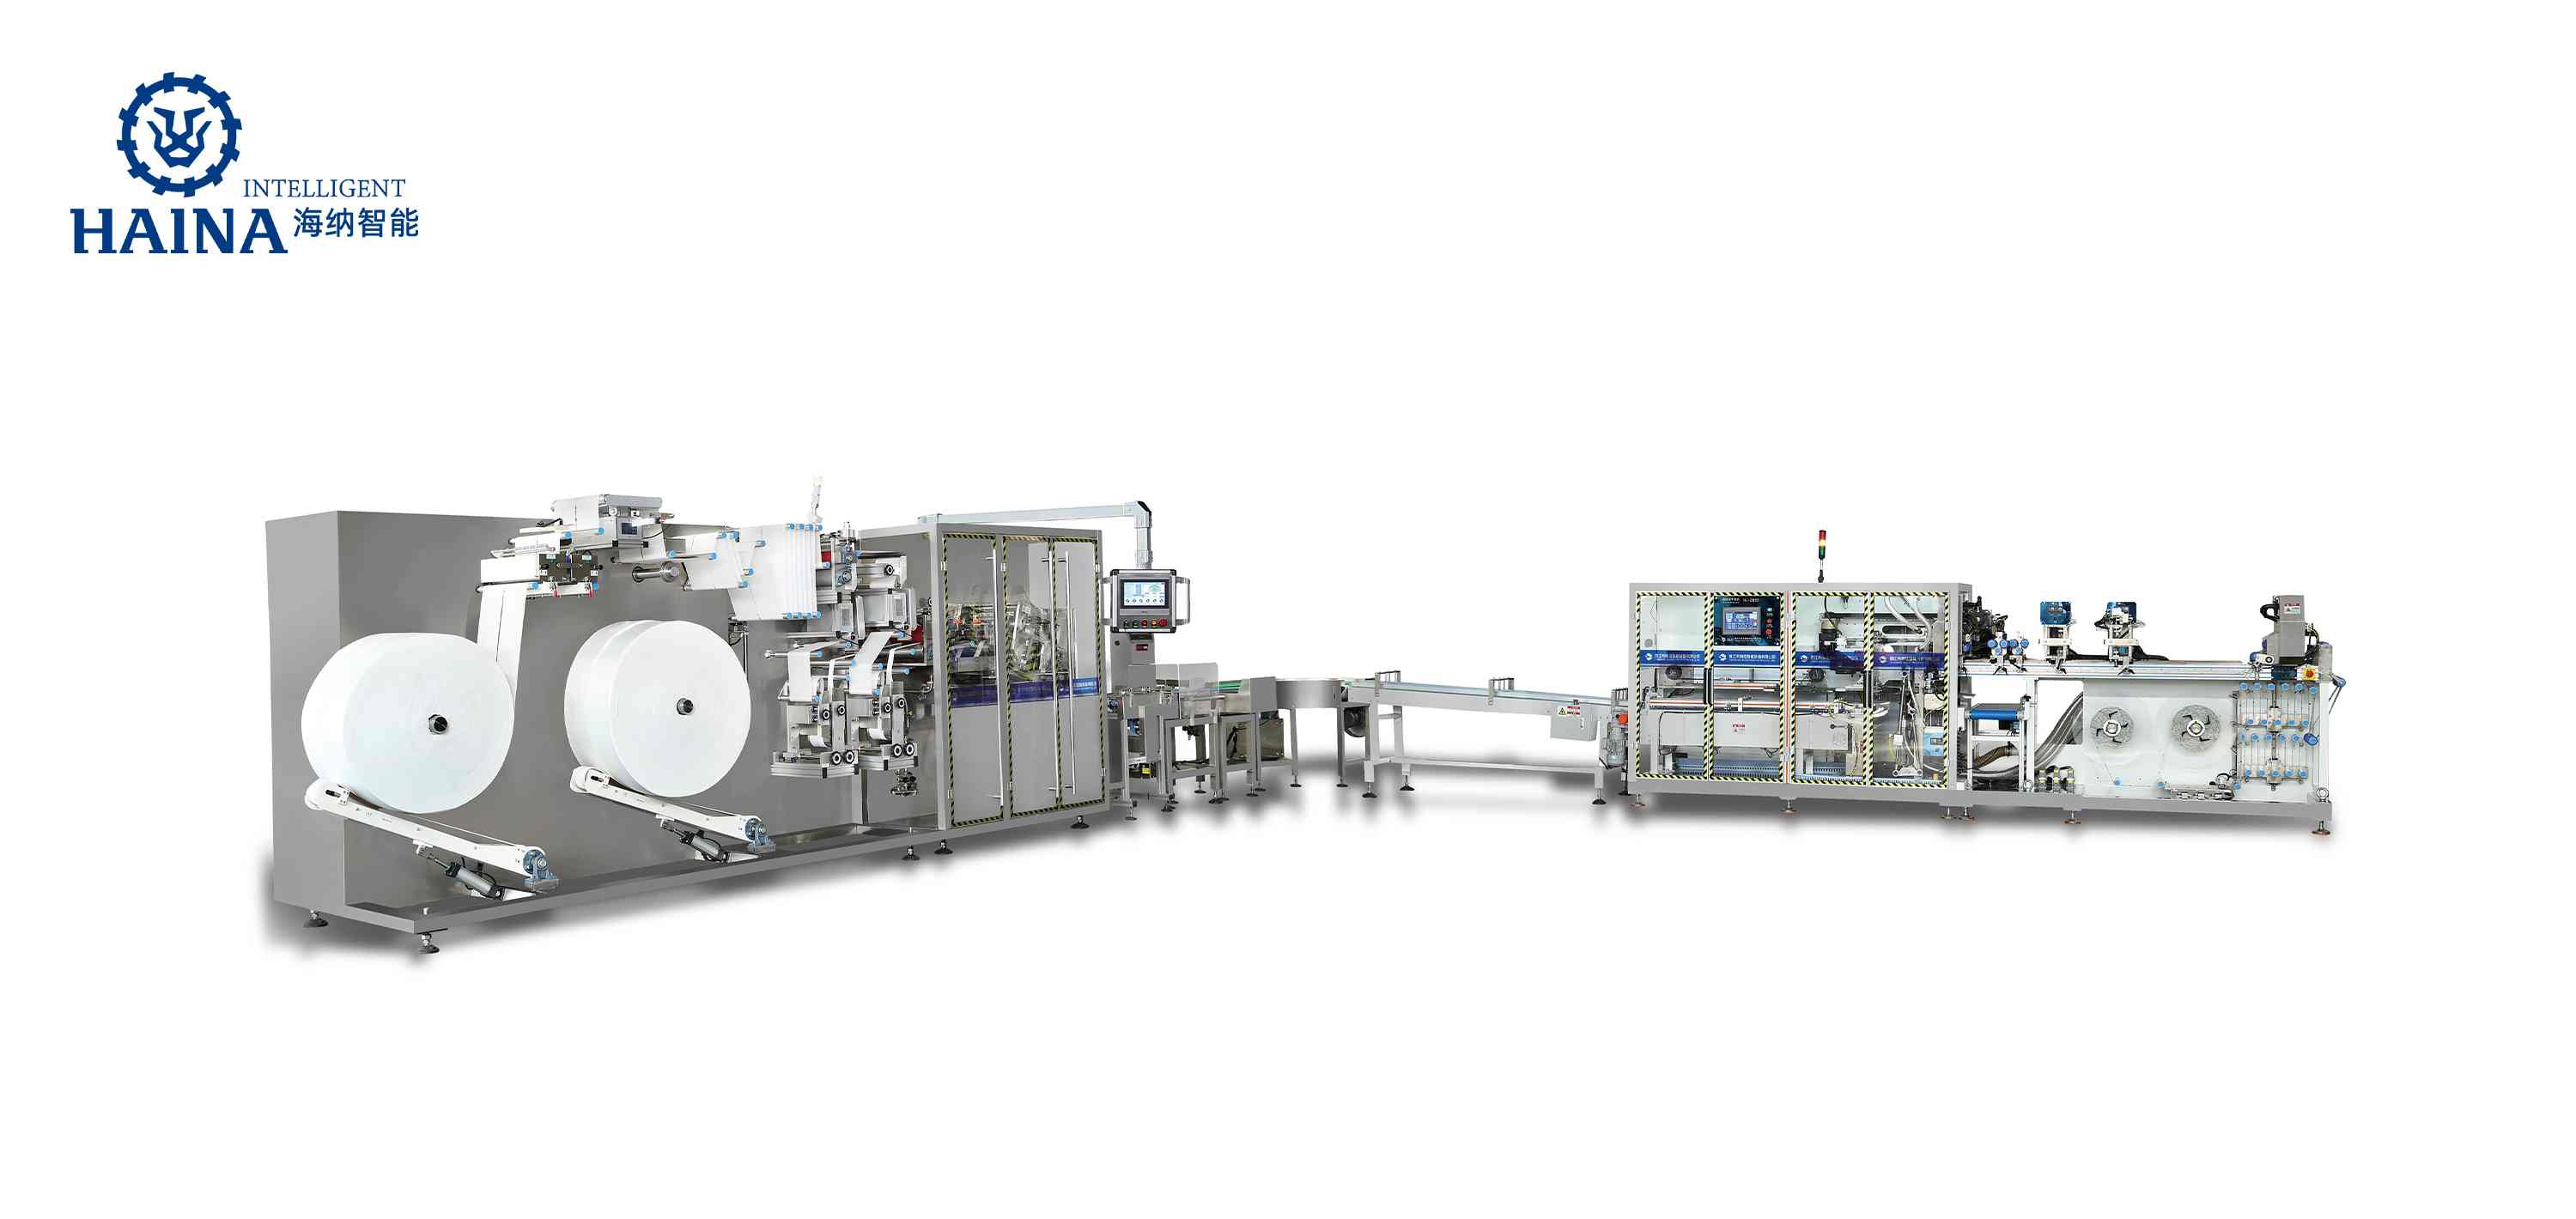
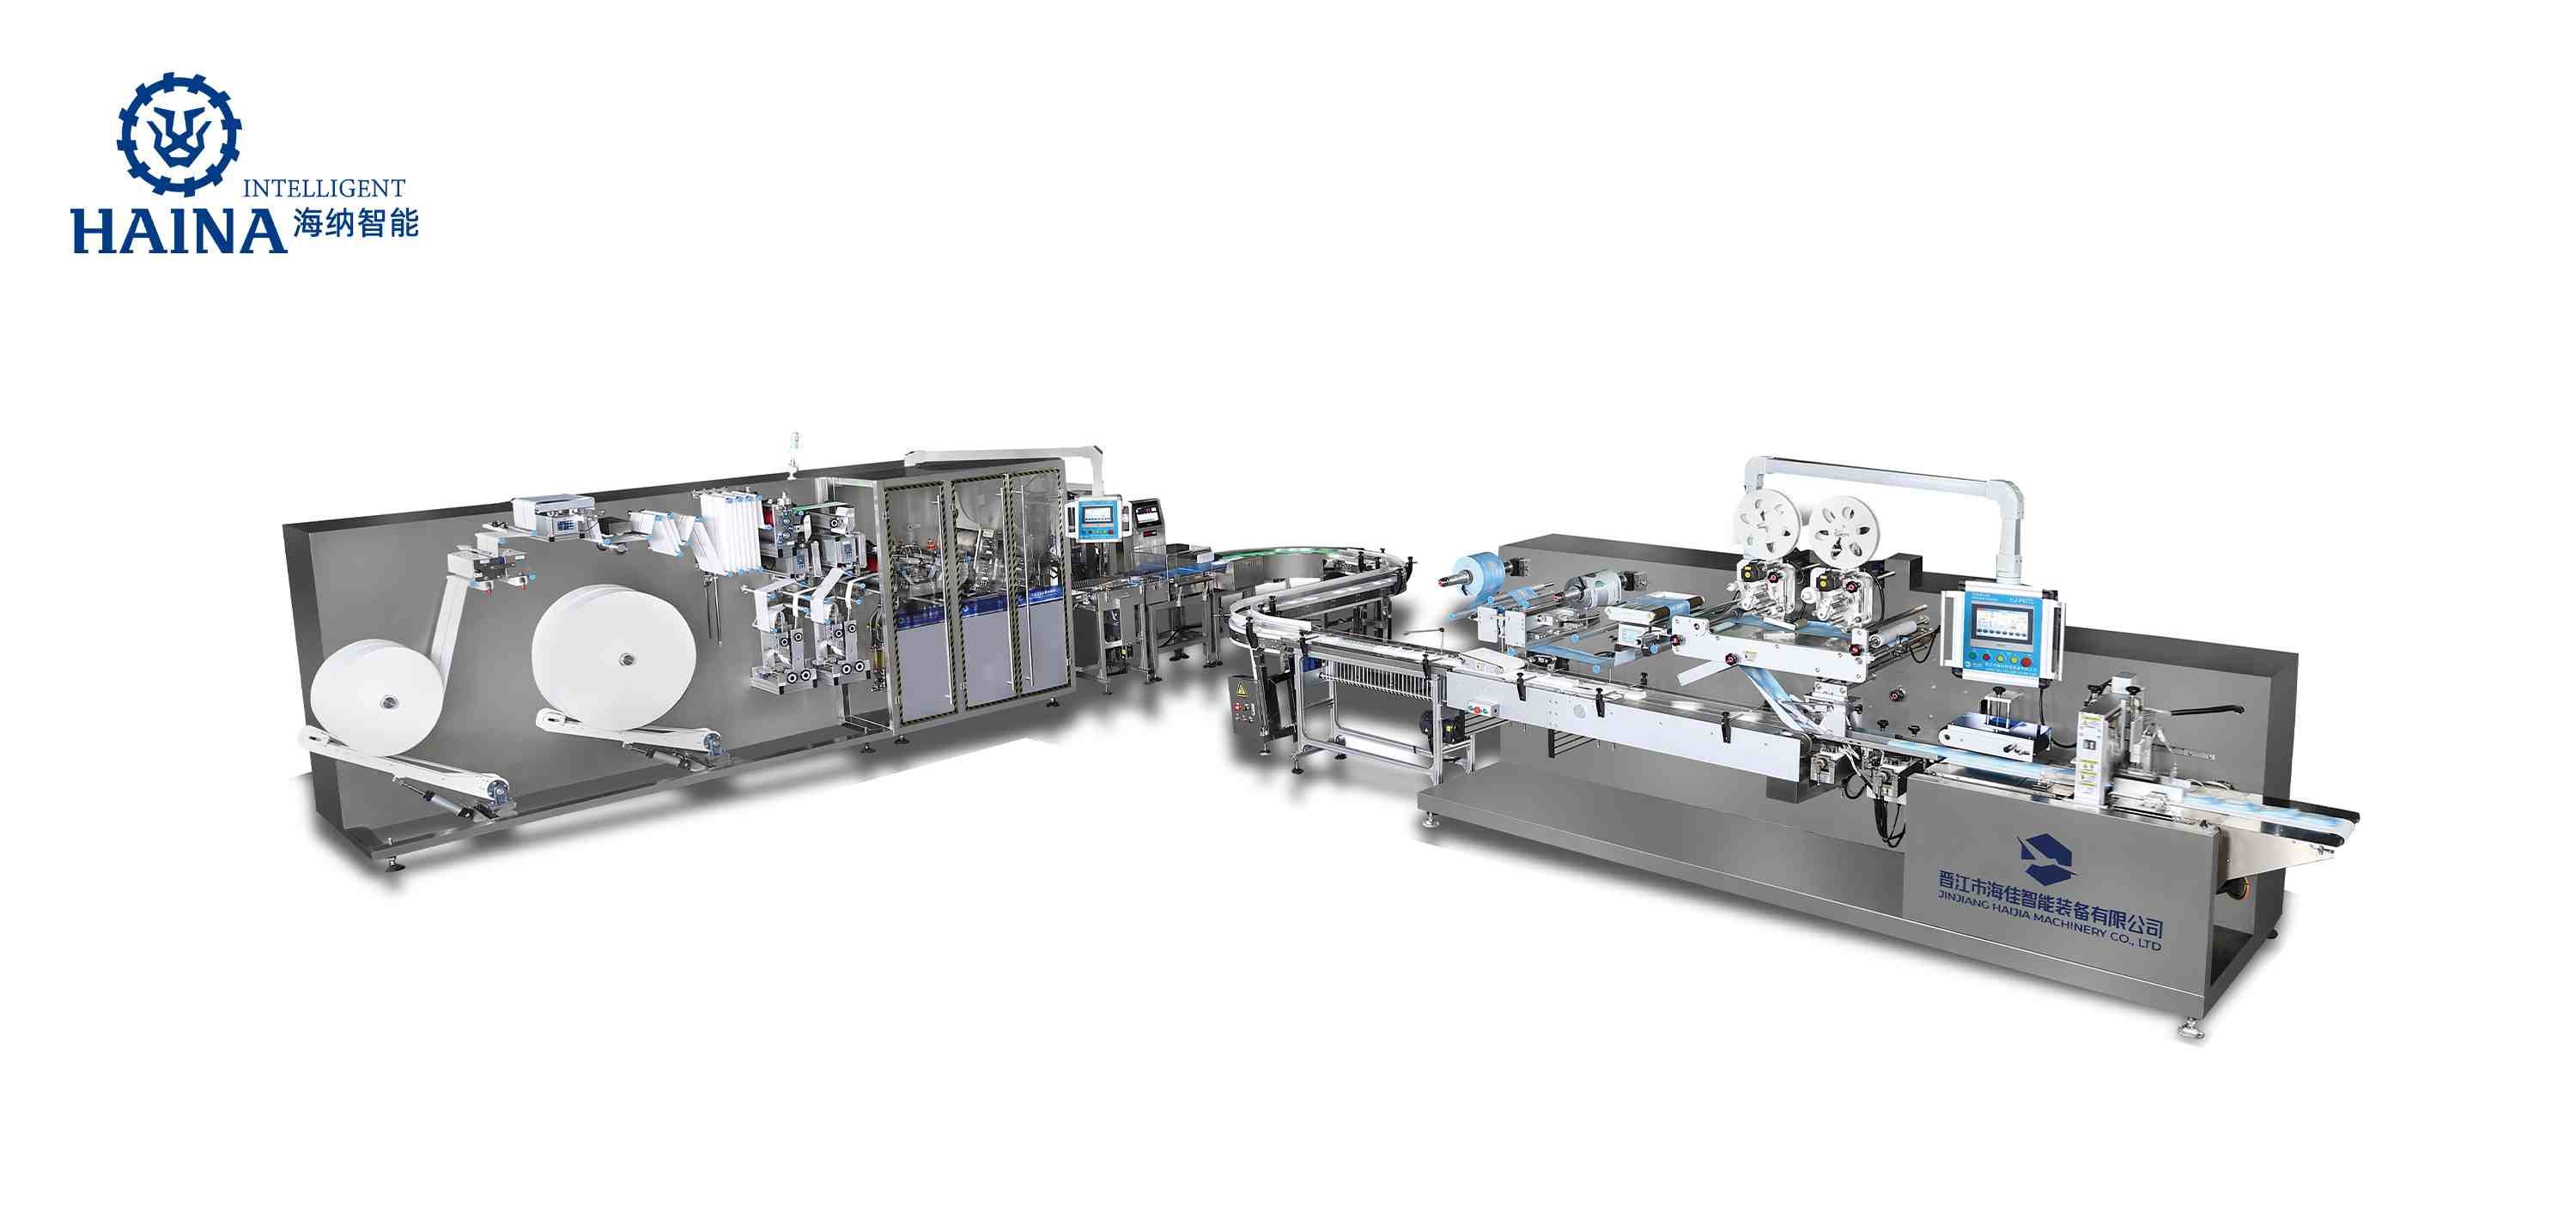
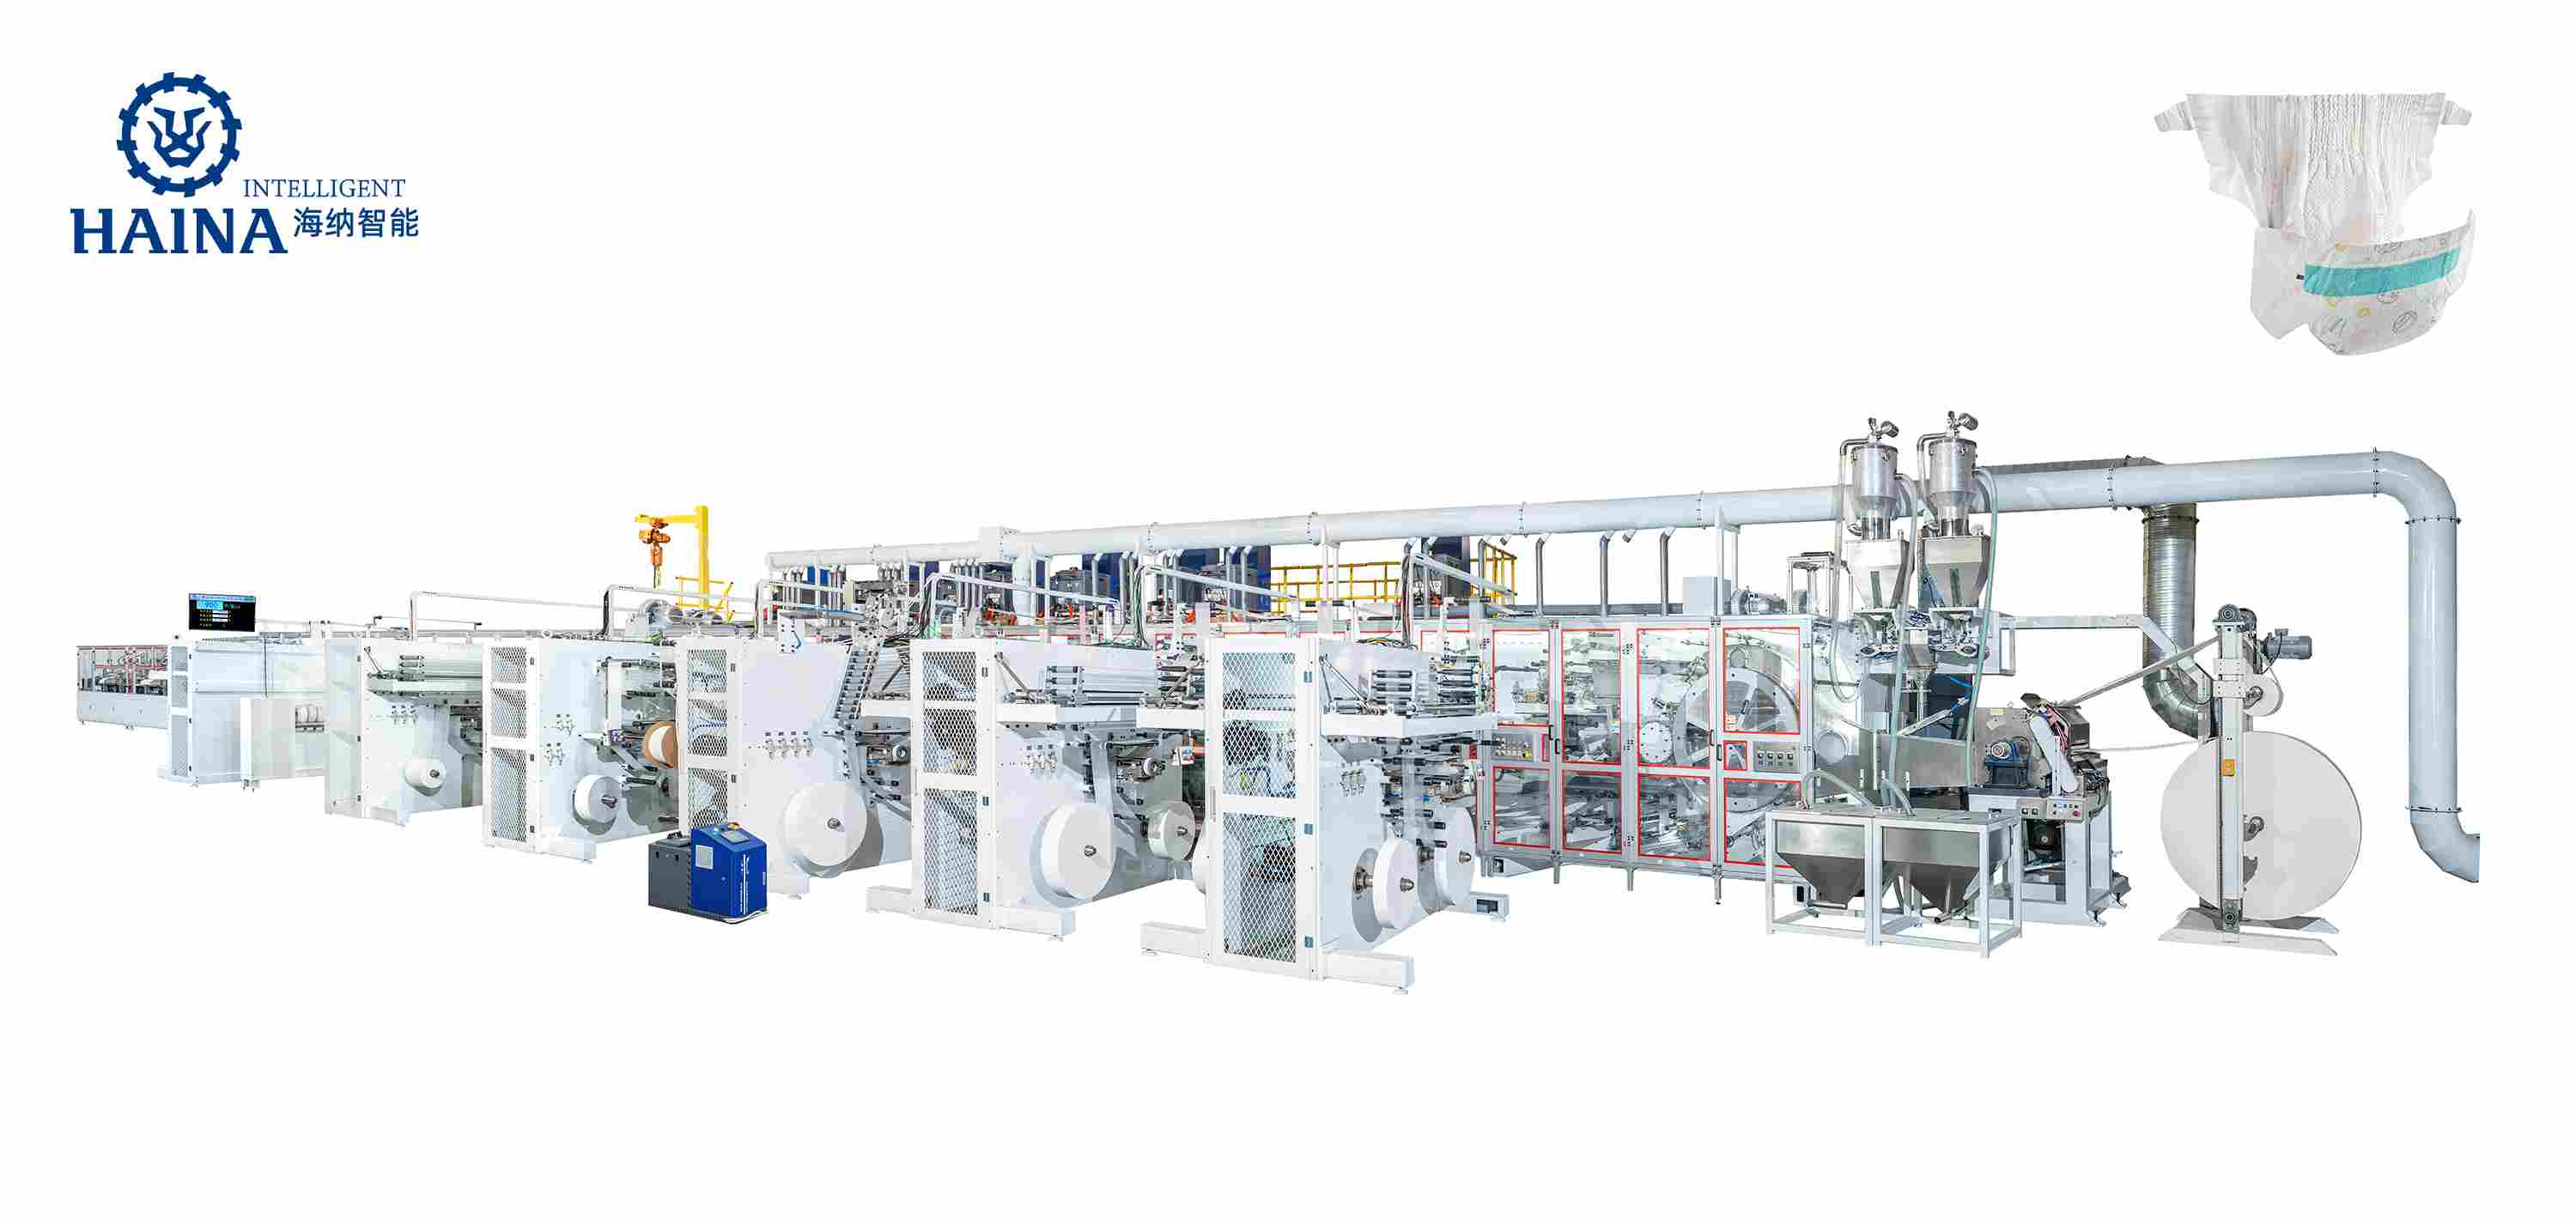
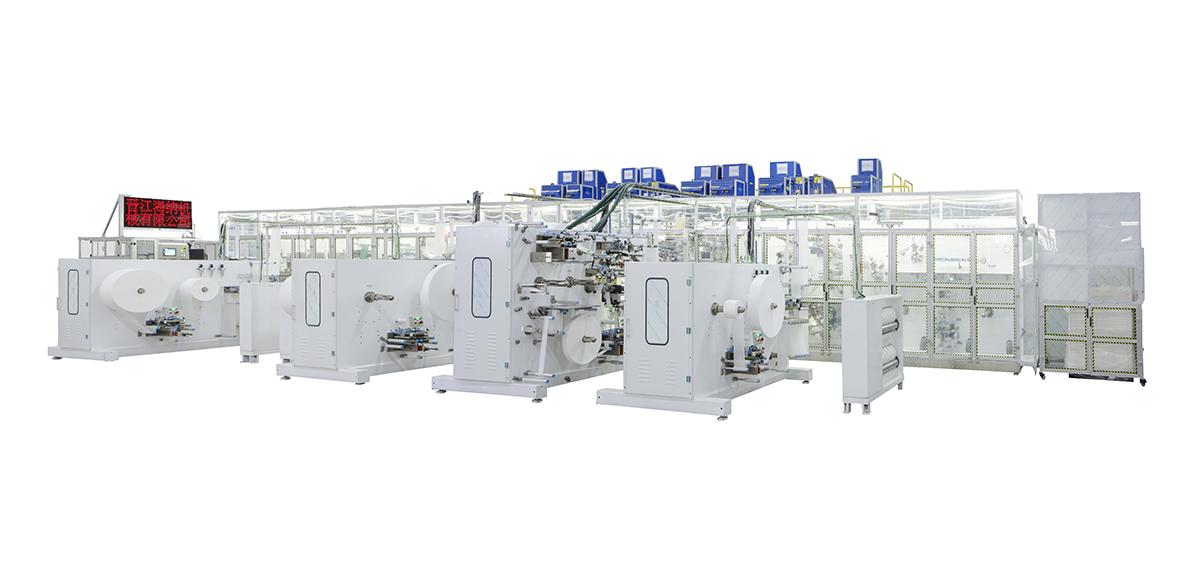
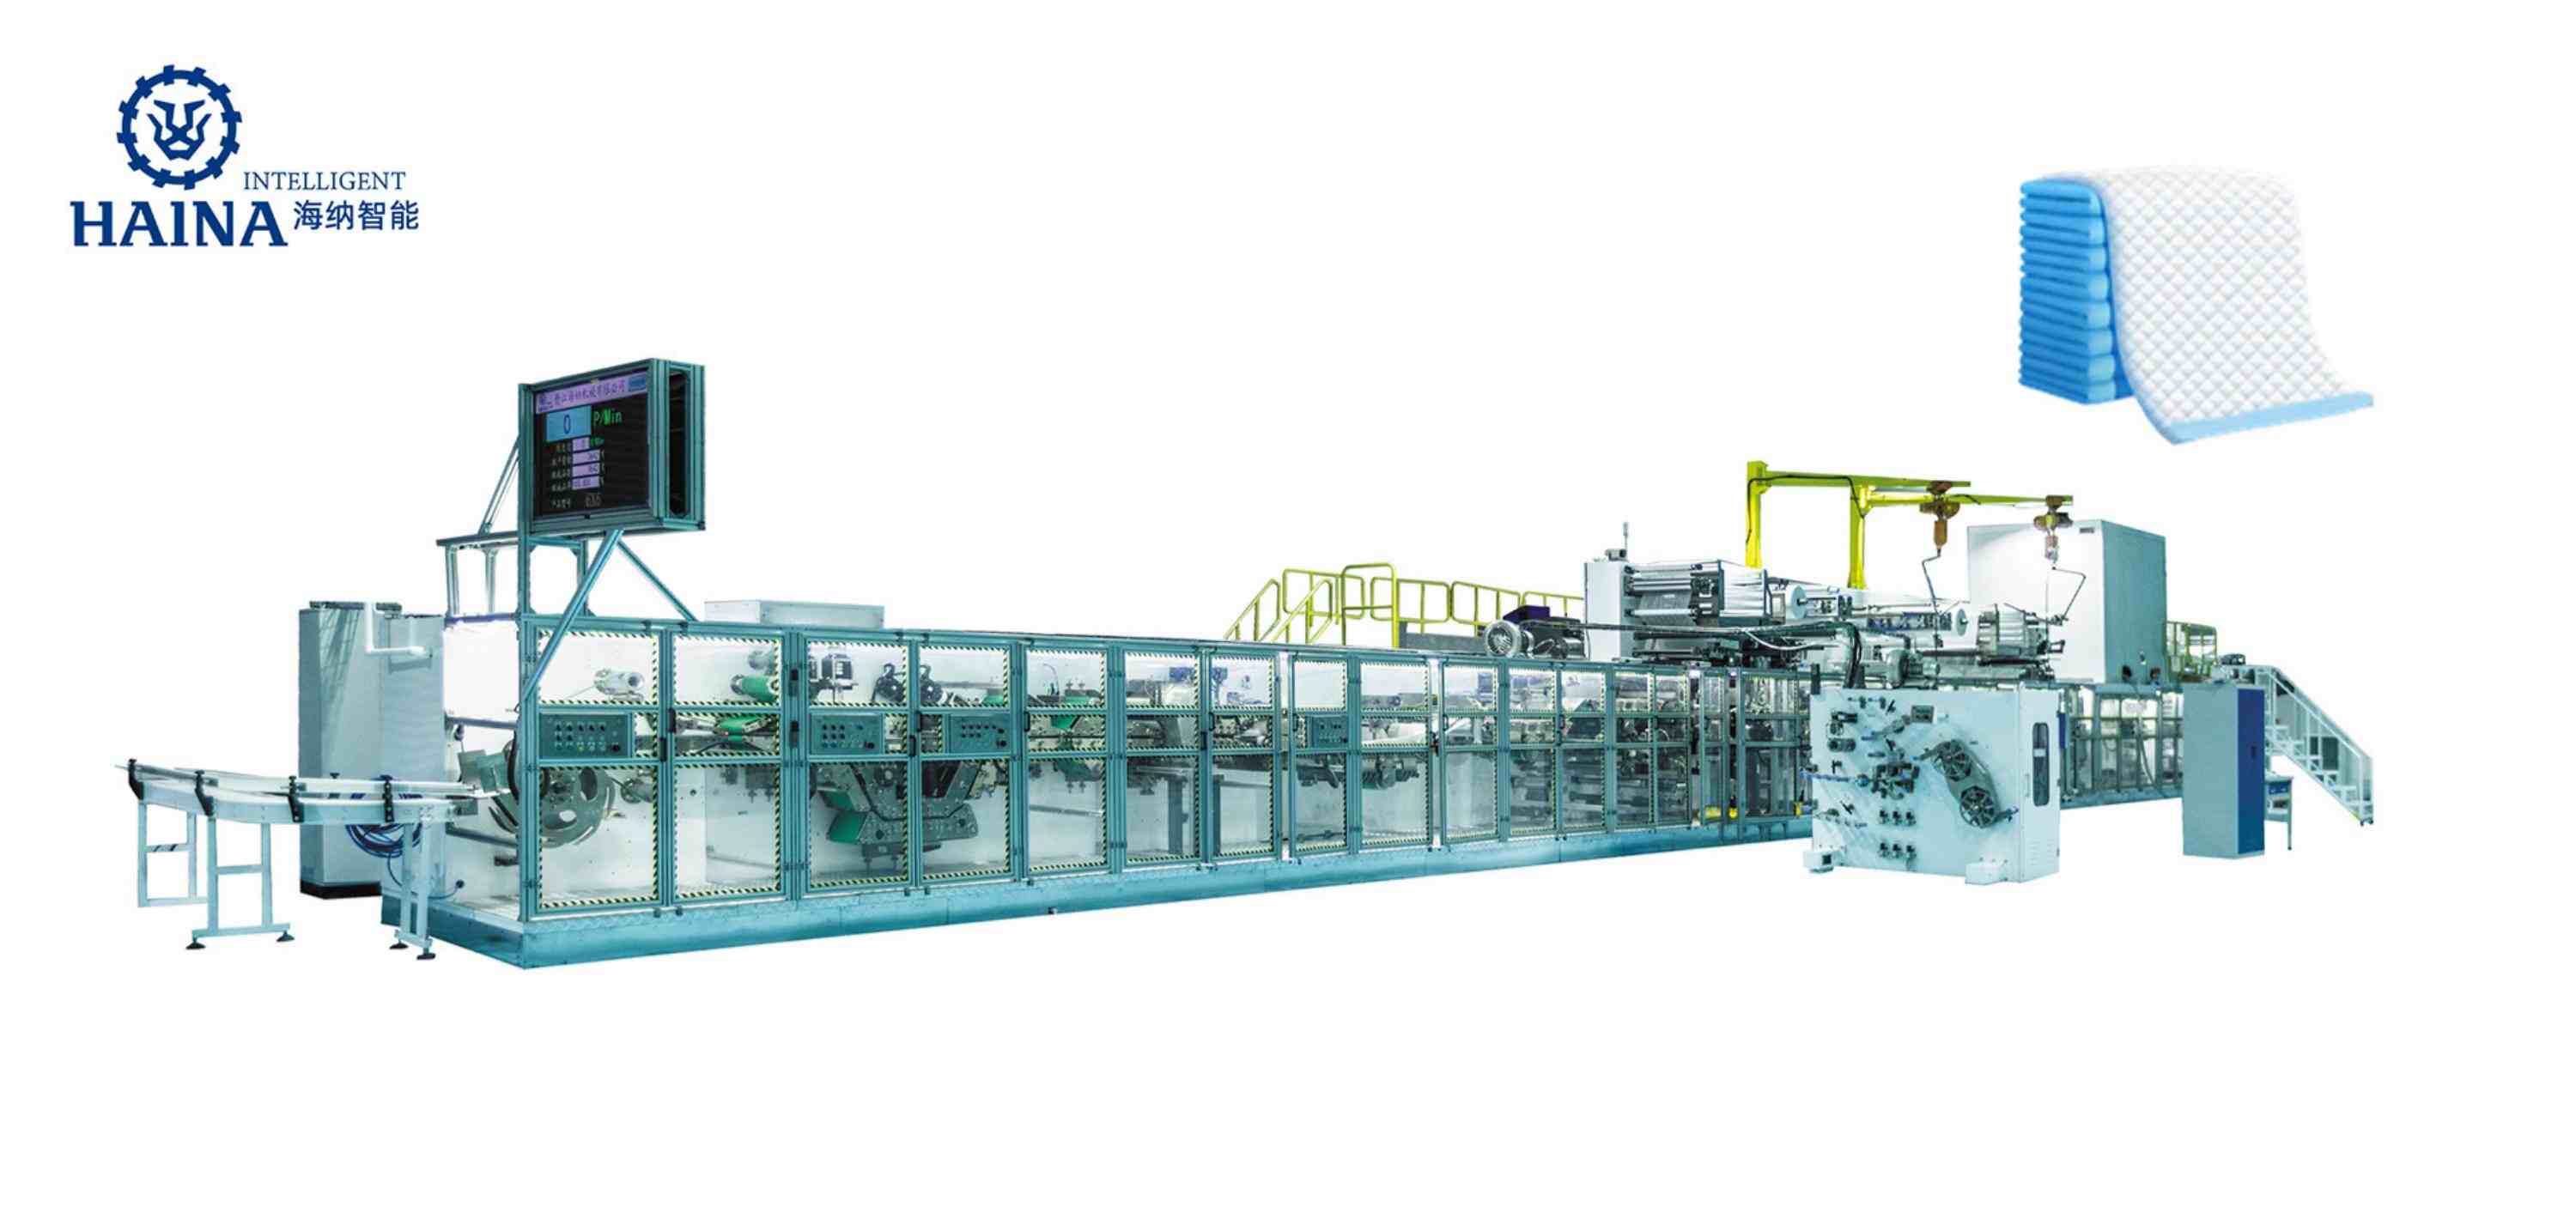
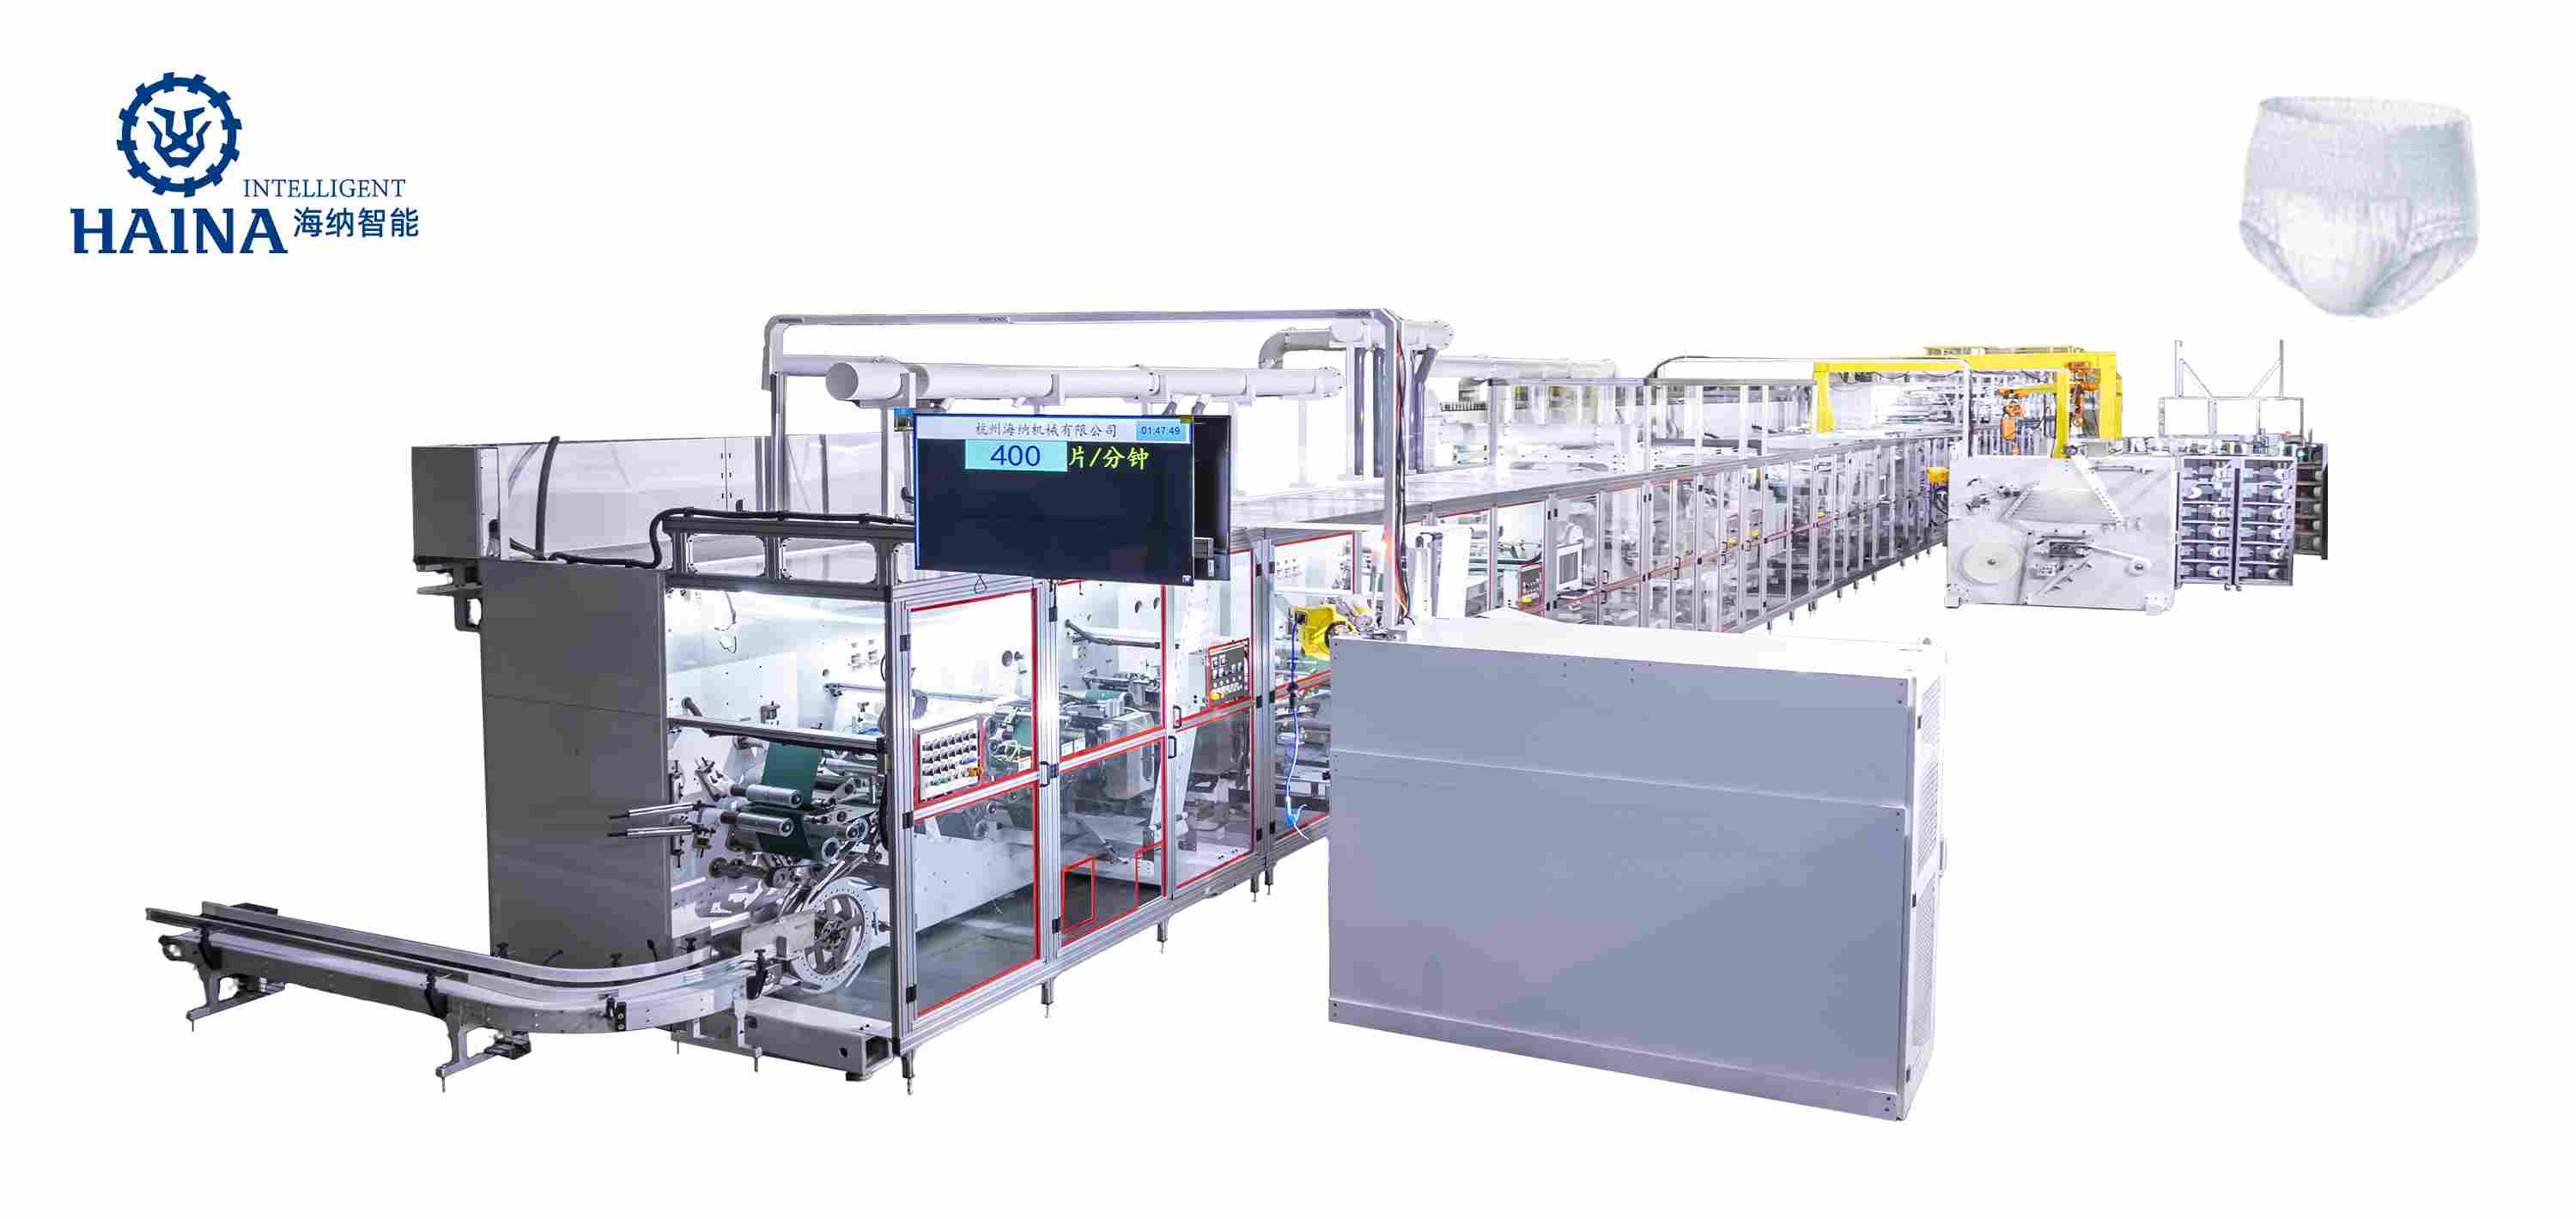
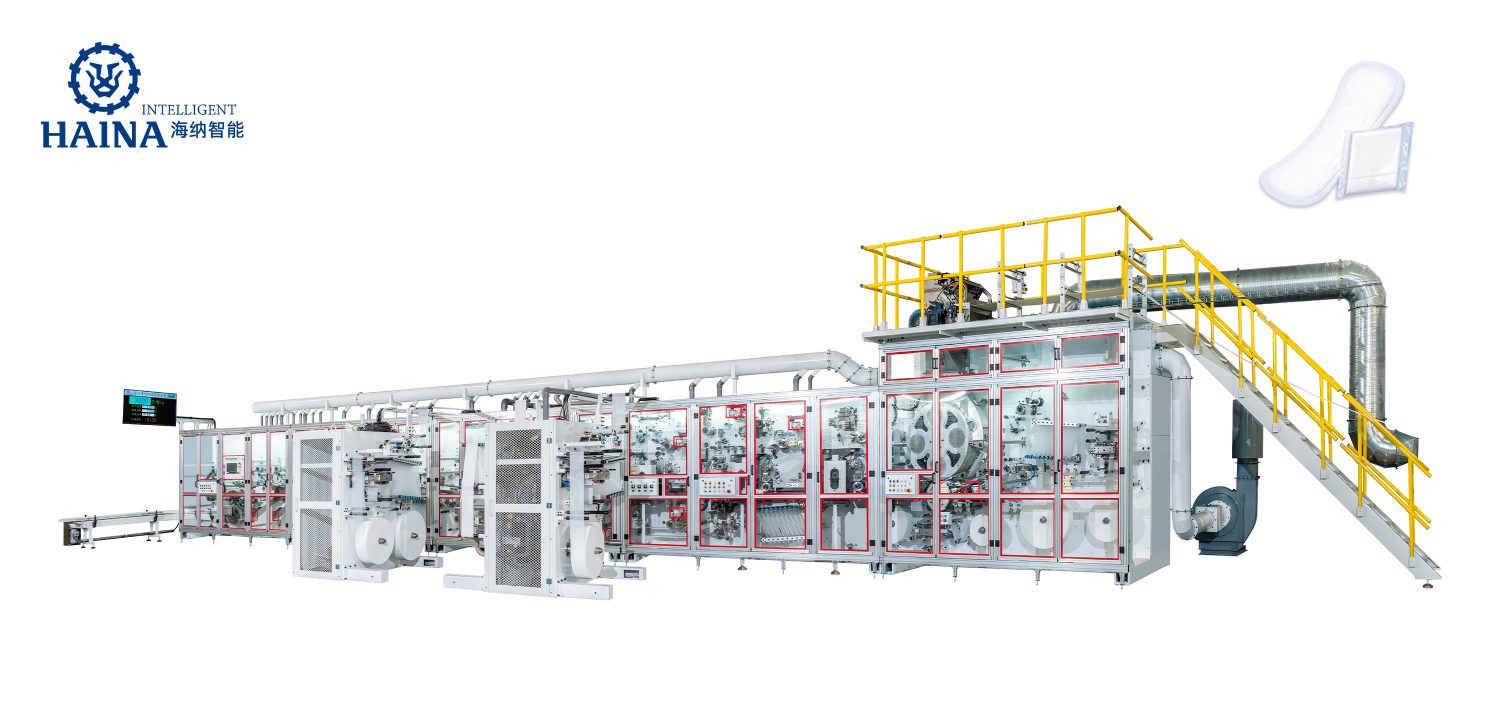
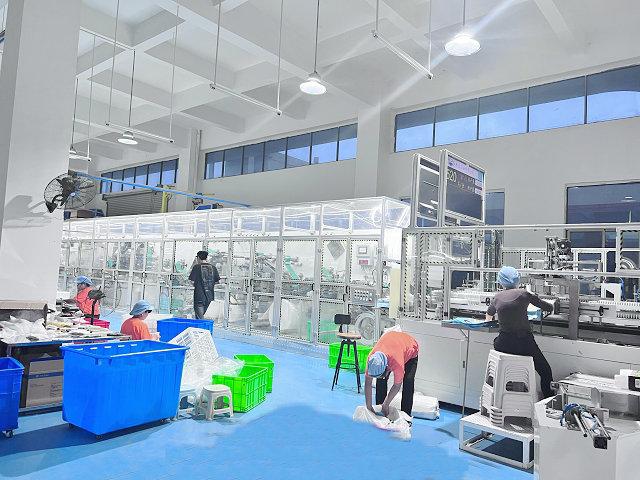
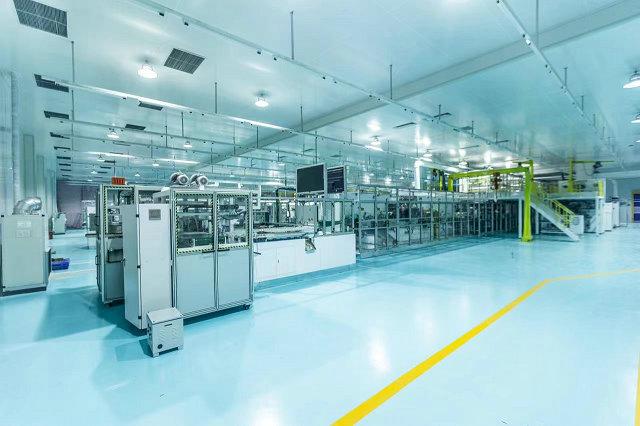
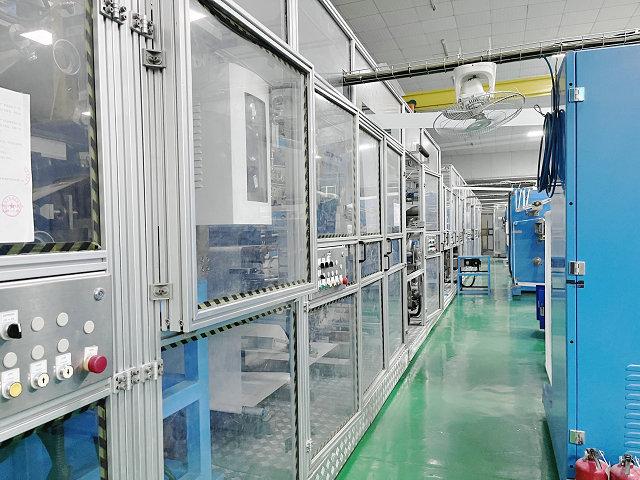
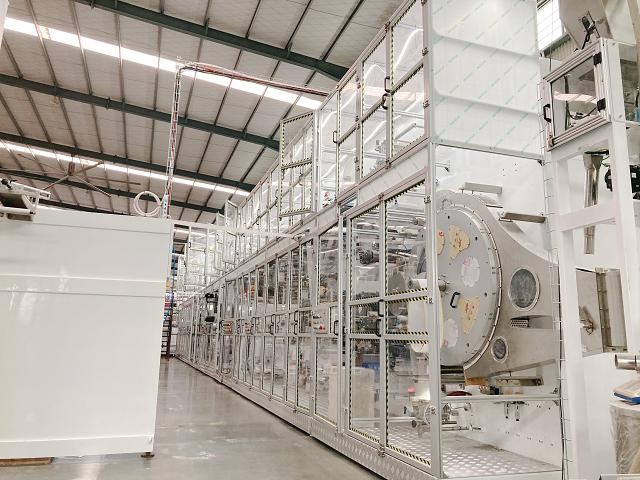
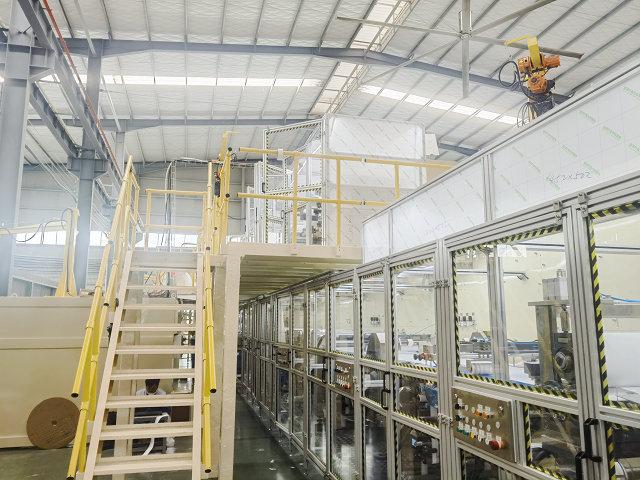
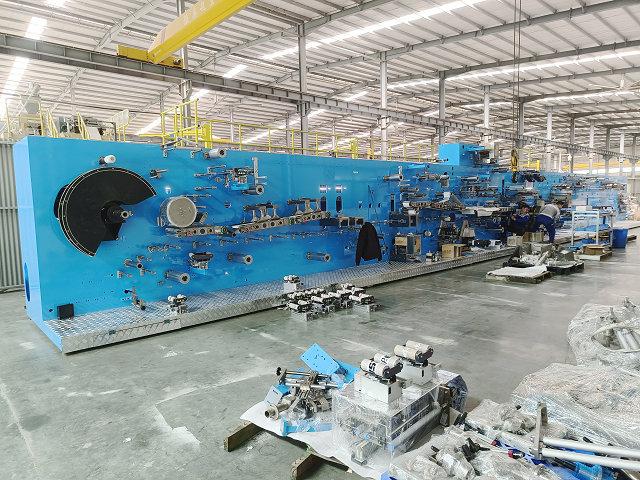
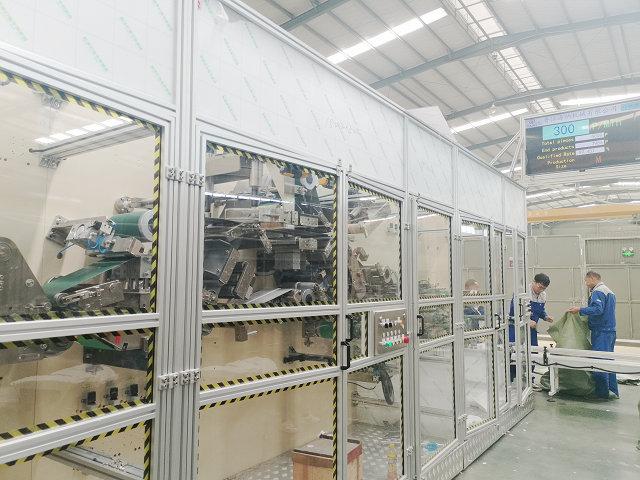
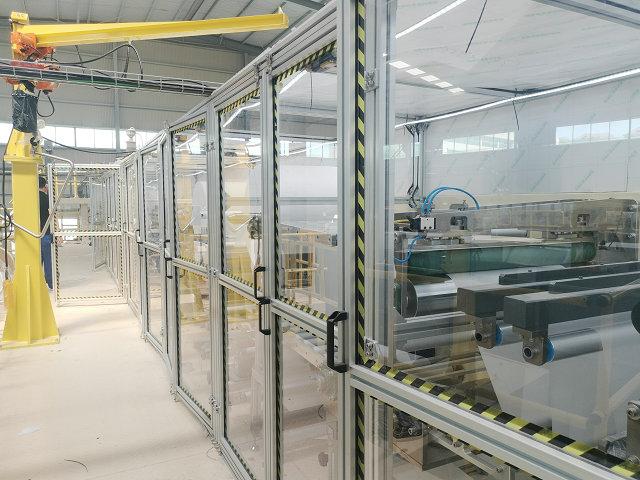
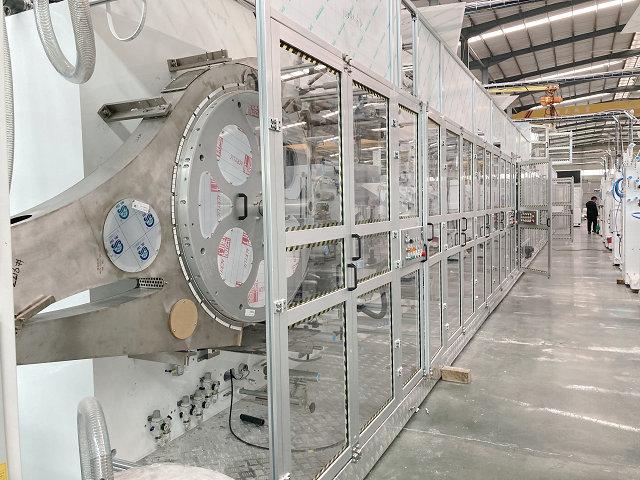
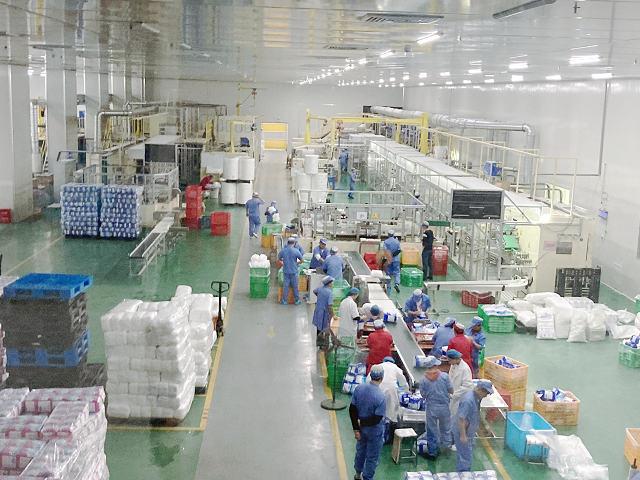
On the entry titled Fully Automatic Pantyliner Machine Video, watch the pantyliner route through two specific lenses: maker-to-packer handoff and controls and alarm response. The commercial lens is automation boundary. HAINA uses the entry to connect filmed movement with documents, material trials and measurable factory acceptance work.
Trace each observable action back to a drawing or acceptance item when studying the Fully Automatic Pantyliner Machine clip; keep open points beside the relevant delivery document.
Trace each visible action back to a drawing or acceptance item for Fully Automatic Pantyliner Machine
A restart is often more revealing than steady running because control loops must recover together. For this entry, follow the path from light-web unwinding to high-rate counting and packing. The material specialist should concentrate on grade, width, winding direction, splice preparation and storage while another reviewer notes every edit, intervention or hidden transfer.
Light-web unwindingFor Fully Automatic Pantyliner Machine, note the handoff toward thin-core lamination and link the observation to thin-core alignment.
Thin-core laminationFor Fully Automatic Pantyliner Machine, follow the handoff toward small-outline cutting and link the observation to cut edge.
Small-outline cuttingFor Fully Automatic Pantyliner Machine, check the handoff toward release-material application and link the observation to release-material position.
Release-material applicationFor Fully Automatic Pantyliner Machine, observe the handoff toward high-rate counting and packing and link the observation to pack count.
High-rate counting and packingFor Fully Automatic Pantyliner Machine, trace the handoff toward light-web unwinding and link the observation to liner length.
Primary evidence at maker-to-packer handoff
A line is only as productive as the transfer between the maker and the packer. Counting, accumulation and recovery should be reviewed as one process. Applied to Fully Automatic Pantyliner Machine, this means comparing the filmed condition with liner length and cut edge on samples from the same operating period.
At this point, assess maker discharge spacing and connect it to the finished-product finding for thin-core alignment on Fully Automatic Pantyliner Machine.
The team should compare counter response, then retain the corresponding Fully Automatic Pantyliner Machine sample used to assess cut edge.
For Fully Automatic Pantyliner Machine, review accumulation behavior before judging release-material position at the next sampling point.
Around restart after a downstream stop, trace the machine condition and the later pack count outcome instead of relying on appearance.
Evidence gap: The earlier text for Fully Automatic Pantyliner Machine did not provide a usable measured value. Ask for a timed run that identifies the SKU, agreed material lots, approved output, stops and rejects instead of inferring performance from screen speed.
Automation boundary for this project
Automation scope must identify the maker, stacker, bagger, inspection, rejection and case-handling boundaries one interface at a time. In the case of Fully Automatic Pantyliner Machine, request an interface matrix showing which modules communicate, accumulate, stop and restart together. Keep the answer separate from the clip so an optional module or untested value is not mistaken for approved scope.
Review layer
Entry-specific check
Film observation
Follow thin-core lamination and mark the transition into small-outline cutting for Fully Automatic Pantyliner Machine.
First measurement
At maker-to-packer handoff, check accumulation behavior against thin-core alignment.
Independent review
Have the material specialist examine controls and alarm response for grade, width, winding direction, splice preparation and storage.
Document request
Request an interface matrix showing which modules communicate, accumulate, stop and restart together and a wear-part list, change procedure and cut-quality samples for the Fully Automatic Pantyliner Machine delivery file.
Acceptance log
For Fully Automatic Pantyliner Machine, retain samples showing release-material position near maker-to-packer handoff and reconcile them with stops, splices and approved downstream output.
Second pass at controls and alarm response
An HMI can display settings and alarms, but the useful issue is what the operator does next and whether the correction is traceable. This second lens is deliberately different from maker-to-packer handoff: for Fully Automatic Pantyliner Machine, it should produce an alarm-response matrix and exported run history from the acceptance test, with the finding reviewed by the material specialist.
After a planned stop, inspect recipe identity and connect it to the finished-product finding for release-material position on Fully Automatic Pantyliner Machine.
The team should note alarm message, then retain the corresponding Fully Automatic Pantyliner Machine sample used to assess pack count.
For Fully Automatic Pantyliner Machine, check authorized adjustments before judging liner length at the next sampling point.
Around history retained after the event, examine the machine condition and the later thin-core alignment outcome instead of relying on appearance.
For Fully Automatic Pantyliner Machine, the material specialist should use cutting and wear-part access as a third cross-check after reviewing maker-to-packer handoff. A clean cut on screen does not show blade life or replacement time. Access, guarding and the wear-part plan matter over repeated shifts. Add a wear-part list, change procedure and cut-quality samples only when that responsibility is included in the proposed line.
Questions raised by the Fully Automatic Pantyliner Machine recording
What does the Fully Automatic Pantyliner Machine footage show well?
It helps locate light-web unwinding, maker-to-packer handoff and high-rate counting and packing. For this Fully Automatic Pantyliner Machine review, it does not by itself establish liner length over time or confirm the controls and alarm response responsibility outside the camera view.
Which follow-up matters most for Fully Automatic Pantyliner Machine?
Ask for approved packed output with maker and packer stops classified separately. Match that log to the same materials and SKU captured during the Fully Automatic Pantyliner Machine review so that the observation and finding describe one run.
How should a buyer use this pantyliner video?
Use it to prepare open points for controls and alarm response, automation boundary and liner length. Close those open points through drawings, retained samples and signed acceptance findings.
Close the review with traceable evidence
File this footage with the product sample, material list, process drawing, line layout, utility schedule and FAT method for Fully Automatic Pantyliner Machine. Number each open item under maker-to-packer handoff, controls and alarm response or automation boundary; assign an owner and the test documentation needed to close it.
Before the equipment scope is signed, HAINA can compare the filmed arrangement with the proposed module list for Fully Automatic Pantyliner Machine. Final acceptance should use agreed materials, agreed measurement methods and retained findings from the named test run, including any finding connected to cutting and wear-part access.