

Before production
Inspect guards, emergency stops, pull wires, roll seating, web paths, adhesive readiness and visible contamination. Confirm that the selected recipe matches the scheduled product.




Start with the location of the first abnormal product, then work backward through material, setting and mechanical causes. Do not compensate for an unknown fault by changing several values at once.
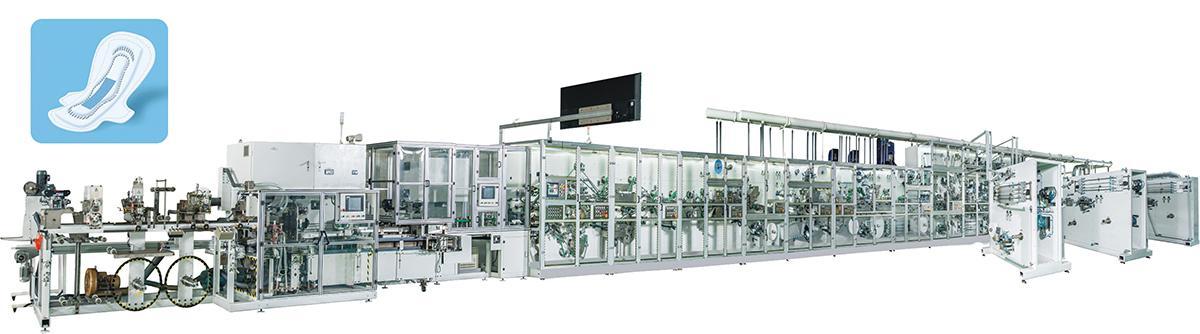
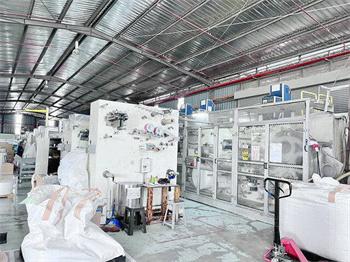
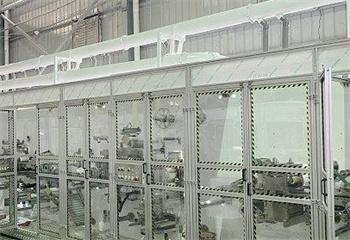
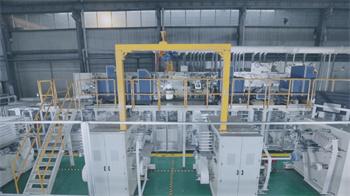
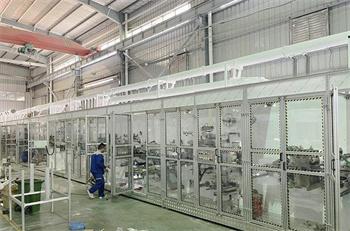
The HD1200 source records servo drive, HMI operation, tension control with a buffer, automatic web guiding, automatic counting and stacking, and safety devices. It also lists a 1,200 ppm design speed and 1,000 ppm stable working speed. These references help organize maintenance, but troubleshooting should be performed under the machine's approved safety procedure and with a known product recipe.
| Visible symptom | First process area to inspect | Evidence to compare |
|---|---|---|
| Web walks toward one edge | Unwind condition, tension path and web guiding | Roll alignment, sensor reference and tracking before the drift point |
| Core position varies | Fluff pulp and SAP feed, containment and transfer | Opened-pad samples and recipe values |
| Release paper shifts | Web tension, position-glue path and cut phase | Registration measurements from consecutive pads |
| Wrapper mark moves | Pouch-film unwind, print sensor and product handoff | Film specification and retained approved wrap |
| Stack count becomes irregular | Discharge timing, counting and downstream recovery | Alarm sequence and event immediately before the error |
Inspect guards, emergency stops, pull wires, roll seating, web paths, adhesive readiness and visible contamination. Confirm that the selected recipe matches the scheduled product.
Watch tracking, tension behavior, dust accumulation, glue placement, cut quality and wrapper registration. Trend recurring small corrections rather than waiting for a line stop.
Clean according to the equipment instructions, inspect wear areas, archive counters and note parts that require planned attention before the next format.
The recorded inputs include topsheet nonwoven, fluff pulp, SAP, backsheet, back release paper, pouch film, easy tape, airlaid paper, construction glue and position glue. A change in roll width, surface treatment, tensile behavior, release force, film print mark or adhesive condition can create a new symptom without a mechanical failure. Compare the incoming material specification and lot with the approved FAT material before altering servo phase or web-guiding settings.
These values are not maintenance intervals. Use the delivered manuals and component schedules to set inspection and replacement frequencies; no universal interval is documented in the archived page.
No. Verify the affected station at a controlled condition, inspect samples and then return through the approved startup procedure.
Keep the first abnormal sample, time, recipe, material lot, alarm sequence and single corrective action. That evidence makes repeated symptoms comparable.
No. Poor roll seating, tension-path issues, a splice or an upstream alignment change may create the drift. Trace the web before changing the guide reference.
Reliable maintenance on the HD1200 comes from preserving cause and effect. A fault history tied to product samples, material lots and exact corrections gives HAINA and the operating team a stronger basis for remote support, spare-part planning and future FAT comparison.
Best sanitary pad machine+Auto Bagger
|
Dimensions(L×W×H8) |
31m*4m*5m |
|
Design Speed: |
1200ppm |
|
Stable Working Speed: |
1000ppm |
|
Rejection Rate: |
≤3% |
|
Efficiency: |
≥85% |
|
Power Source: |
380V,50HZ |
|
Machine Capacity: |
290KW |
|
Air Pressure: |
0.6-0.8Mpa |
|
Machine Weight: |
50 tons |
Factors influencing the quality management of Best sanitary pad machine maintenance
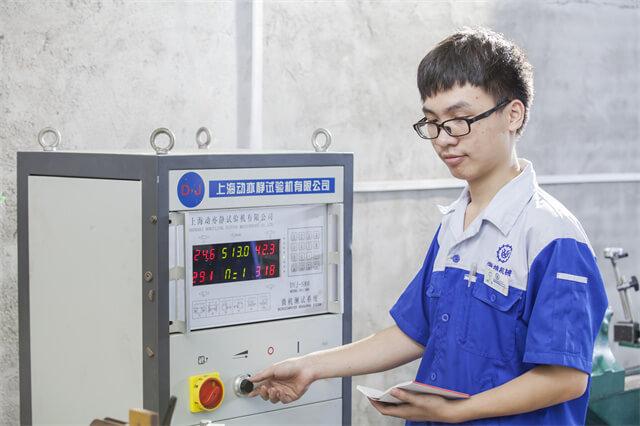
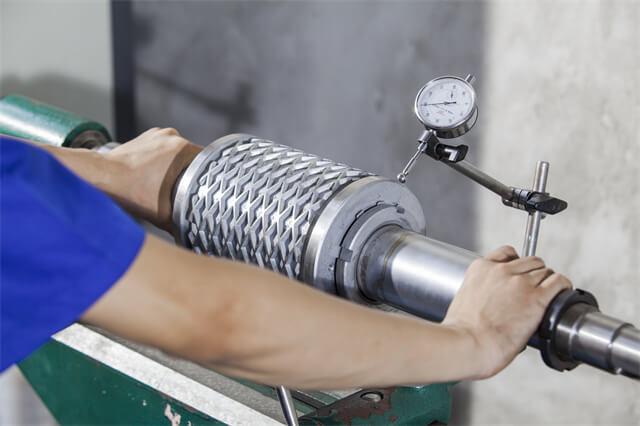
Due to the long-term operation of the Best sanitary pad machine, it is inevitable that various failures will occur. Through mechanical maintenance, defects are repaired, functions are improved, and normal operation is ensured. Maintenance quality management plays a decisive role in the operation status and economic benefits of equipment after maintenance. It is necessary to strengthen the quality management during maintenance, improve the maintenance level, and ensure the integrity rate of the equipment.
FULL Auto Best sanitary pad machine+Auto Bagger
| No. | Raw materials |
| 1 | Topsheet NW |
| 2 | Fluff pulp |
| 3 | SAP |
| 4 | Backsheet |
| 5 | Back release paper |
| 6 | Pouch film |
| 7 | Easy tape |
| 8 | Airlaid paper |
| 9 | Construction glue |
| 10 | Position glue |


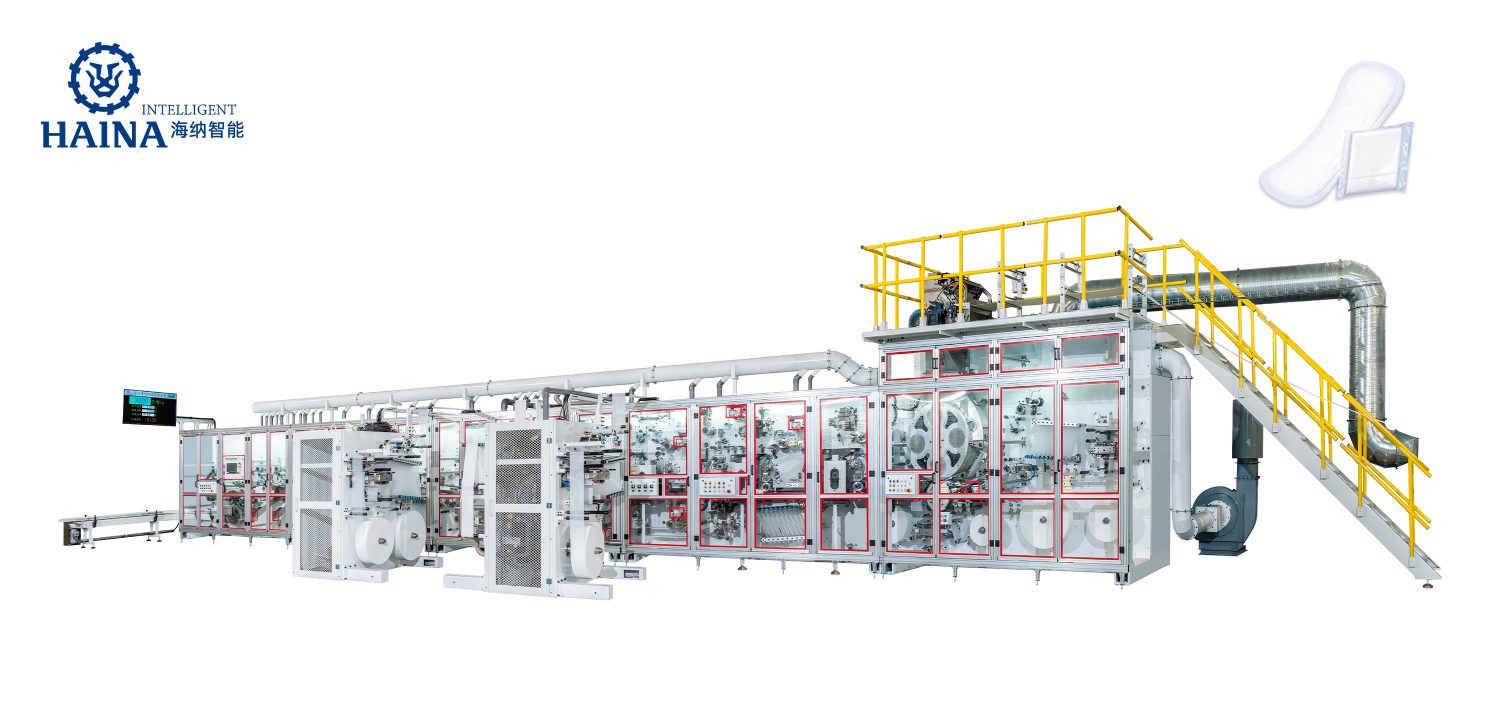
Plan HD3500 pantyliner line delivery through sample approval, scope freeze, engineering, FAT and handover while resolving legacy speed conflicts....
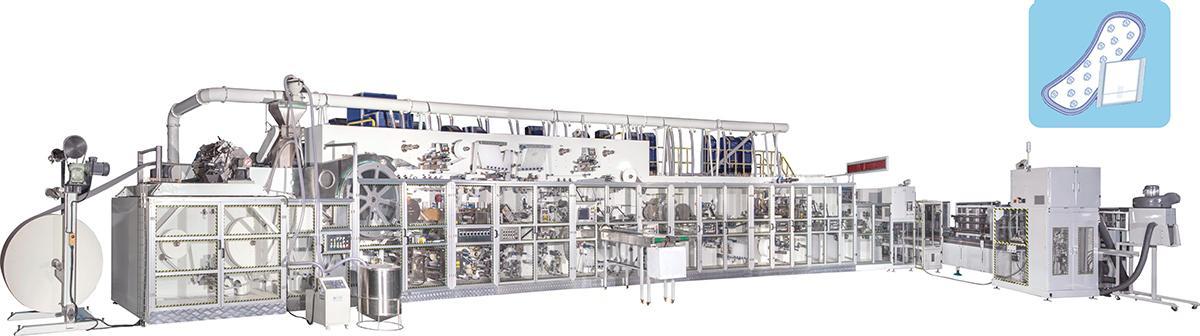
Plan WSJ1000 sanitary pad changeovers with controlled drawings, materials, tooling, recipes, wrapper checks and first-off approval....
Review the HD1200 sanitary pad machine nameplate, process controls, utilities, material inputs and specification questions before purchase....






The quality of the feminine napkins produced by this Feminine Napkin Machine is unmatched. Our customers have given us great feedback since we made the switchEmily T 2024-05-31
Our customers have noticed the difference in the quality of our feminine napkins since we started using this machine. Highly recommendedMegan H 2024-05-31
The support team behind the Feminine Napkin Machine is top-notch,They provided excellent training and assistance when we needed itLaura M 2024-05-31
The Feminine Napkin Machine is a game-changer for our business. It's efficient, reliable, and produces high-quality products consistentlyRachel W 2024-05-31