Adult & Baby Diaper Machine,Sanitary Napkins Production Line Blog
Plan repeatable M, L, and XL adult diaper machine changeovers with controlled parts, recipes, materials, line clearance, first-piece checks, and timing.
M, L, and XL changeovers on an adult diaper machine should be planned as controlled product conversions, not as a single recipe selection. The change may affect core length and width, web guides, elastic positions, tape placement, cutting phase, folding, stack count, and bag format. A reliable plan identifies which parts and settings change for each size, prepares tools and materials while the line is running, then gives one leader authority over shutdown, installation, verification, and first-good-product release. Success is measured by safe completion, documented settings, controlled waste, and repeatable accepted product, not by the shortest restart time alone.
Define the M L and XL Product Family
Start with controlled product drawings for all three sizes. Show finished dimensions, core geometry, material widths, cuff and elastic positions, fastening component locations, cut length, fold geometry, package count, and quality limits. A size name is a commercial label, not an engineering definition. One factory's L construction may not match another buyer's L.
Create a commonality review. Identify components that retain the same material and setting, components that use a wider or longer web, and features that need dedicated tooling. A product family designed around shared material widths and reference positions may support a simpler conversion, but product performance and market requirements remain the first constraints. Do not force commonality if it compromises the approved construction.
Determine the preferred sequence. Changing from M to L may require fewer adjustments than moving directly from M to XL, but this depends on machine design and product architecture. Production planning should consider order volume, material staging, cleaning, packaging formats, retained stock, and the risk of mixing sizes. The shortest mechanical change is not always the most efficient campaign sequence.
Assign a unique product code and approved recipe revision to each size. Labels on change parts, gauges, carts, raw materials, packaging supplies, samples, and records should use the same code. Visual similarity among parts can cause an incorrect assembly that remains unnoticed until quality checks fail.
Each size should be defined by drawings materials tooling recipes and quality limits.
Map Every Mechanical and Recipe Change Point
Walk from the first material feed to product discharge and list every size-dependent item. Possible points include pulp and SAP recipe, core forming or cutting geometry, tissue width, acquisition layer position, topsheet and backsheet guides, cuff width and location, leg and waist elastic paths, frontal tape, side tapes, cut phase, transfer timing, folding plates, compression, stack count, bag format, and inspection regions.
Classify each point as recipe only, mechanical adjustment, exchanged part, exchanged material, inspection setting, packaging change, or no change. For an adjustment, record the approved reference and measurement method. For an exchanged part, record identification, quantity, orientation, fastening, storage location, lifting need, and inspection. For a recipe, control access and revision so an operator cannot accidentally save trial settings over the approved baseline.
Mark dependencies. Moving an elastic guide may also require a sensor region and adhesive pattern change. A longer product affects cut timing, transfer pitch, fold position, stack dimensions, and bag length. Dependencies determine sequence and prevent one team from approving its zone while a downstream setting still belongs to the previous size.
Use photographs only as supporting aids. A photograph cannot replace a dimension, torque requirement where specified, gauge, part number, or machine reference. The best change sheet shows both the physical location and the controlled value needed for verification.
Change control note: If an operator needs an undocumented adjustment to obtain acceptable product, record it as a deviation and review the master recipe or setup standard after the run.
Separate External and Internal Changeover Work
External work can be completed while the line safely produces the current size. It includes confirming the schedule, checking the next product drawing, staging released materials, preparing the change-parts cart, checking tools and gauges, loading approved recipes without activating them, preparing packaging, reviewing open maintenance issues, and briefing the team.
Internal work requires the machine to be stopped or isolated. It includes removing and installing guarded parts, moving physical guides, changing cutters or forming components, threading different webs, cleaning exposed process areas, changing packaging format parts, and verifying safety restoration. Moving a task from internal to external is useful only when it remains safe and does not risk mixing or premature settings.
Assign roles before shutdown. One changeover leader controls the sequence and status board. Production handles material and approved operating settings. Maintenance performs authorized mechanical work and isolation. Quality manages line clearance, sample checks, and release. Packaging staff prepare the downstream format. No section should restart independently without the leader confirming that dependencies are complete.
External preparation reduces stopped work while controlled access protects internal change tasks.
Control Tools Parts and Incoming Materials
Use a dedicated cart or staged area for each size. Shadow locations or labeled trays help the team see whether a part has been removed or returned. Include all approved tooling, fasteners, spacers, guides, gauges, cleaning materials, lifting devices, and protective packaging. Inspect items before the planned stop so damage or missing parts do not become downtime.
Line clearance prevents product and material mixing. Remove previous-size rolls, partial webs, labels, bags, loose components, samples, and work instructions according to the factory procedure. Identify and protect usable partial rolls. Reconcile old packaging materials before bringing the next size to the line. Quality should verify clearance at defined points rather than relying on a general area check.
Incoming material status must be visible. Check product code, lot, width, winding direction, roll condition, splice, and staging position. The first roll for each feed should be accessible in the correct loading order. Wide adult product materials need enough lifting and maneuvering space; a rushed roll movement can damage an edge before the changeover trial begins.
Prepare first-piece inspection tools and approved reference samples before shutdown. If the measuring device, test method, or responsible approver is unavailable, the machine may restart but accepted production cannot begin. The changeover plan ends at quality release, not at the first movement of the line.
Execute a Safe Change Sequence
Stop and segregate: record the last accepted product, remove in-process material as required, identify suspect output, and complete line clearance.
Make safe: apply the approved isolation and stored-energy procedure for all internal work, including hot adhesive and pneumatic or rotating zones.
Change upstream references: install core, web, cuff, elastic, tape, and cutting settings in the controlled order shown on the change sheet.
Change downstream format: set transfer, fold, count, stack, bag, code, and discharge arrangements for the new product and pack specification.
Verify before motion: account for tools, inspect part identity and orientation, confirm fasteners, restore guards, and obtain section signoff.
Load the recipe: activate only the approved revision and verify critical values against the size master rather than trusting the recipe name.
Thread and start slowly: check tracking, tension, phase, cutting, adhesive, component placement, folding, and rejection under controlled conditions.
Release in stages: quarantine startup product, approve first pieces, raise speed through defined checks, and release normal production only after quality approval.
Approve the First Good Product
First-good-product approval needs a predefined sample plan. Check identity, dimensions, core location and condition, material orientation, cuff and elastic position, tape placement, cut quality, adhesive or bond condition, folds, appearance, package count, bag condition, code, and any product performance checks specified by the buyer. Use calibrated or otherwise controlled inspection tools according to factory practice.
Samples should come from more than one moment. Inspect initial setup pieces, products after critical adjustments, products at the intended stable condition, and products after a controlled stop and restart where required. One acceptable piece does not prove that the line is centered or that settings remain stable after acceleration.
Define the disposition boundary. Startup and adjustment products should remain separated until quality determines whether they are scrap, rework, training samples, or acceptable. The first accepted unit needs a time or count reference so production records, materials, and packaging can be reconciled.
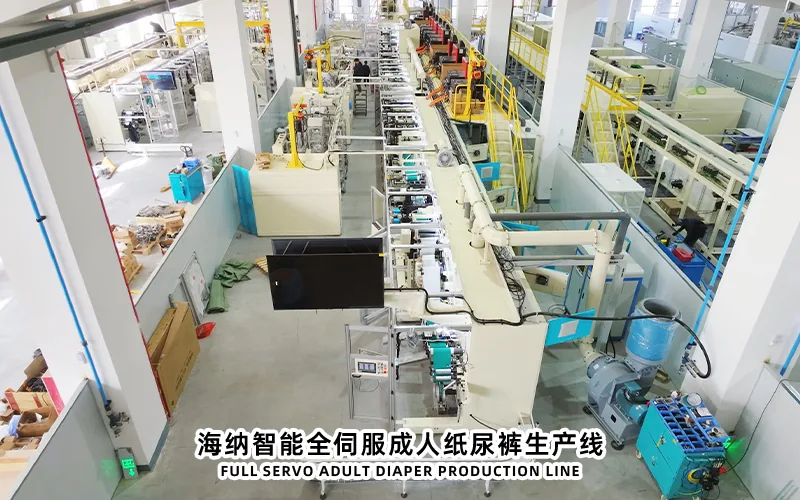
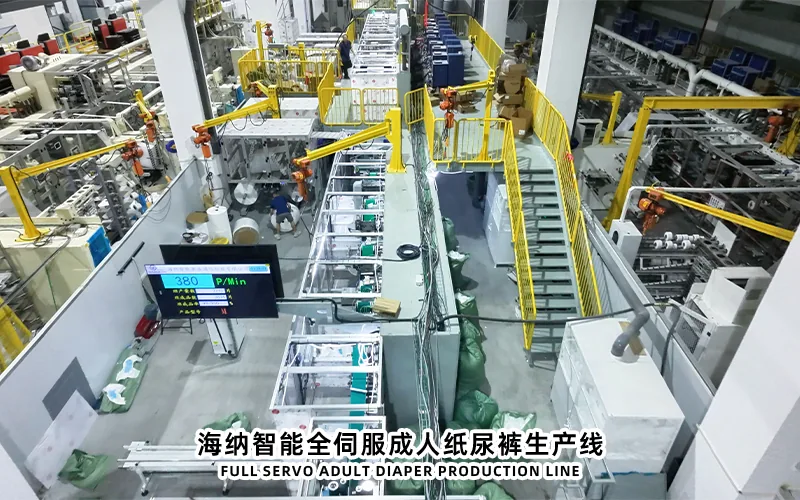
When reviewing a HAINA adult diaper machine project, buyers can ask for the size-part list, recipe structure, change sequence, sample plan, and operator training scope. Actual product dimensions and acceptance limits should follow the approved buyer documents.
First-product approval must include downstream folding stacking and packaging conditions.
Use a Size Change Matrix
Change point
M to L review
L to XL review
Release evidence
Core and absorbent recipe
Dimensions dosing and transfer reference
Largest format capacity and containment
Recipe revision mass and position samples
Web cuffs and elastics
Widths guide marks and component positions
Travel limits tension margin and roll handling
Installed material check and product measurements
Tapes cutting and phase
Placement pitch cutter and sensor regions
Timing range tooling identity and transfer
Part signoff challenge and retained pieces
Folding and stacking
Fold plates product orientation and count
Large-product stability and compression
Approved stack and repeated transfer
Bag and code format
Bag size count seal and printed identity
Pack dimensions handling and case fit
Complete accepted packs and line clearance
Ramp to stable output
Defined speed steps quality checks stop logging and accepted boundary
Signed startup record and good-product release
Populate the matrix with actual settings and part references; do not use it as a generic instruction at the machine. Some transitions may share tooling, while another product family may require more extensive exchange. Validate every row during commissioning and revise it through formal change control.
Improve Changeover Repeatability
Observe several changeovers before setting a target. Video or detailed task timing can reveal walking, searching, waiting, repeated measurement, unclear authority, and unnecessary adjustment, provided the site's privacy and safety rules allow it. Separate necessary process time from delays caused by missing materials, parts, approvals, or information.
Improve repeatability with fixed reference marks, error-proof part identification, preset assemblies, dedicated carts, controlled recipes, accessible gauges, standard tool locations, and parallel external preparation. Any modification to guards, safety functions, precision parts, or approved machine settings needs engineering review. Faster work must never depend on bypassing isolation or inspection.
After each conversion, hold a short review. Compare planned and actual task time, startup waste, adjustments, first-pass approval, stops during the following run, and part or material issues. Assign one improvement at a time and test it on the next relevant conversion. A stable median result is more valuable than one unusually fast event.
Repeatability is confirmed by accepted production after the team completes the documented conversion.
Size Changeover FAQ
Can M L and XL sizes be changed only through the HMI?
Usually not. A recipe may coordinate many settings, but material widths, guides, tooling, sensors, folding, stack, and packaging can also require physical verification or exchange.
Which changeover time should be reported?
Report clearly defined intervals, such as last accepted product to first accepted product, and break the total into tasks. This prevents quality waiting or preparation failures from being hidden.
Should the line jump directly to stable working speed after a size change?
No. Use controlled speed steps with product checks appropriate to the affected modules. Release normal output only after the line and downstream equipment are stable and quality approves the result.
How can size mixing be prevented?
Use line clearance, unique product codes, segregated rolls and bags, labeled change parts, controlled recipes, startup quarantine, reconciliation, and an identified first accepted product boundary.
Conclusion
Adult diaper machine changeover planning for M, L, and XL sizes starts with engineering definitions and ends with accepted packed product. Map recipe and physical changes, expose dependencies, move safe preparation outside stopped time, control parts and materials, and use one leader for execution. A size matrix, first-piece plan, and task-level time record make the result repeatable. Improvement should reduce searching, waiting, and adjustment while preserving isolation, line clearance, product verification, and traceability.