Place of Origin: CHINA
Brand Name: HAINA
Configuration: Confirmed per project
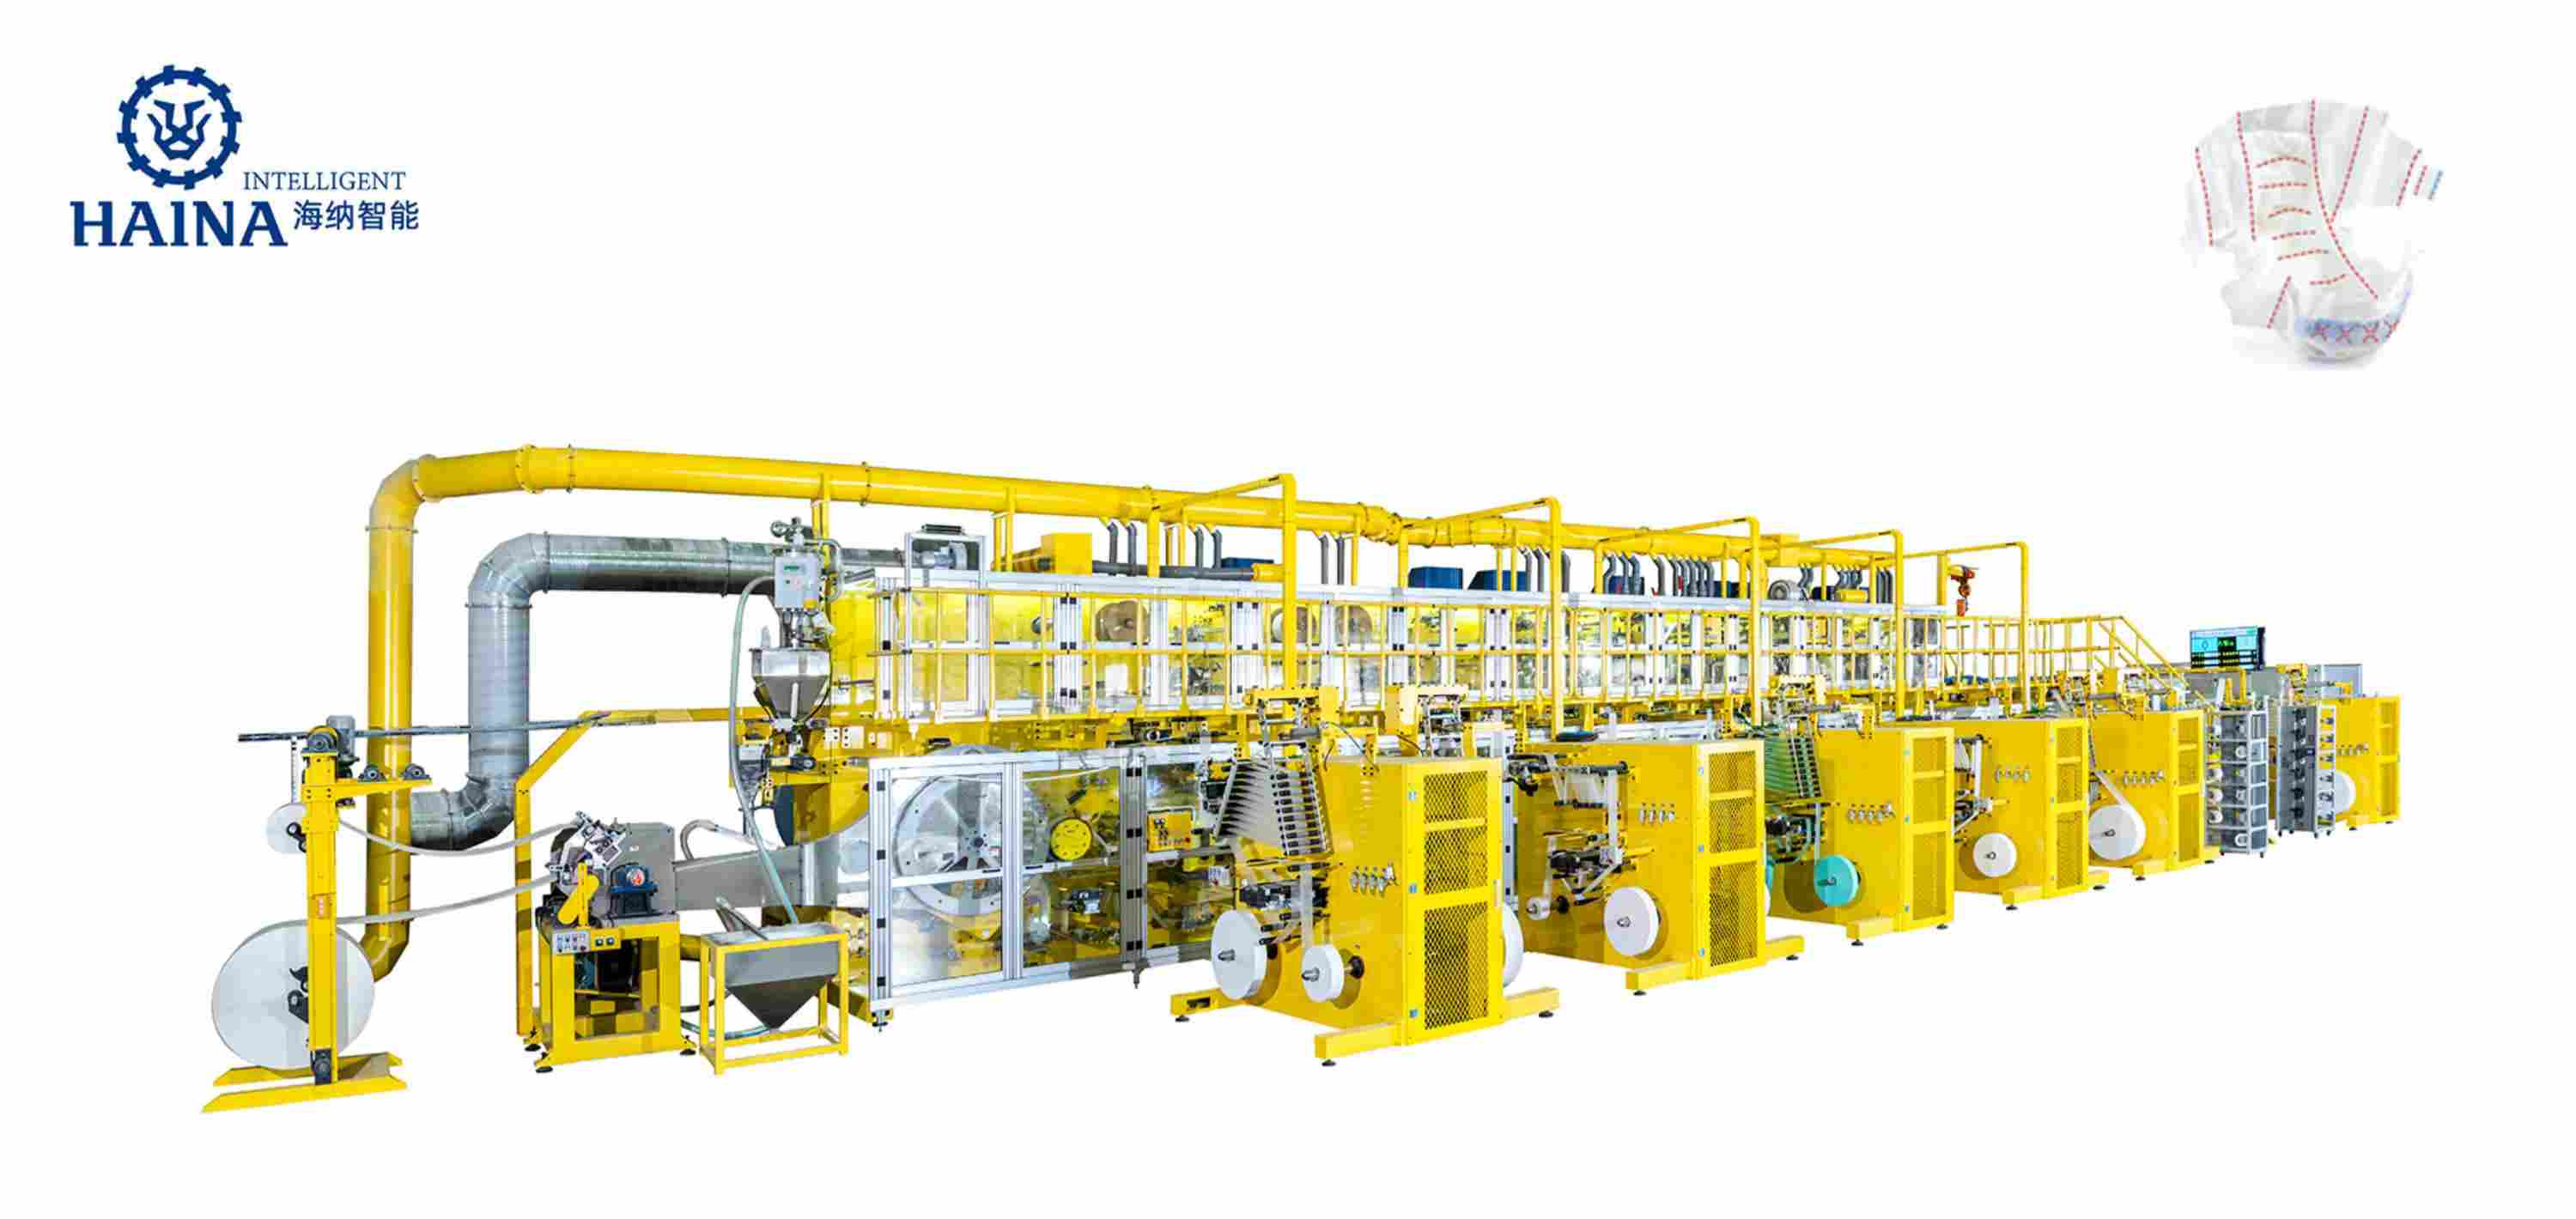
Model Number: TK500-fully automatic baby diaper machine
Payment & Shipping Terms:
Order Scope: Confirmed equipment modules
Quotation: Based on product and automation scope
Export Packing: Confirmed in offer
Lead Time: Confirmed in contract
Payment Terms: Confirmed in contract
Delivery Scope: Confirmed in technical agreement
The TK500 record provides enough data to prepare a serious factory acceptance test, but not enough to accept the line from a brochure alone. The buyer and HAINA should first lock one diaper construction, the trial materials, the counted output boundary and the downstream scope. The checklist below turns the legacy figures into observable evidence.
Freeze the witnessed product before the run
Sample
Approve the diaper size, T-shape ear geometry, core construction and finished fold that will be made during FAT.
Inputs
Record supplier, grade, roll width and lot for every material used in the witnessed run.
Counting point
State where a piece becomes accepted output and how start-up, splice and downstream rejects are classified.
Recorded TK500 envelope
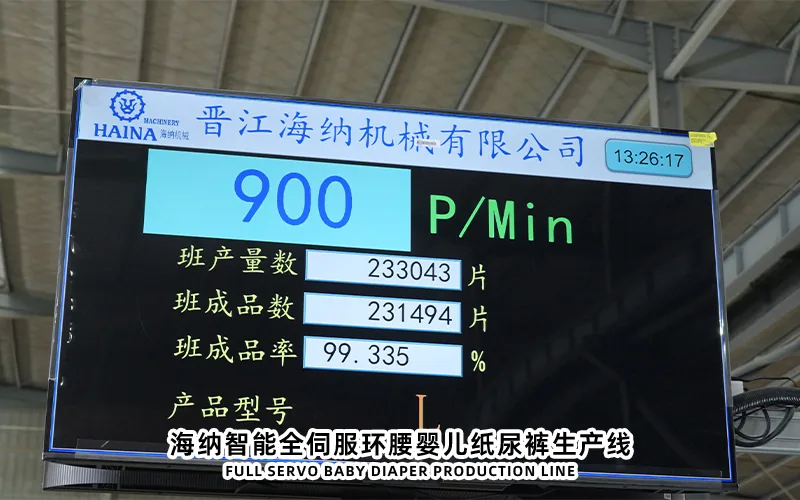
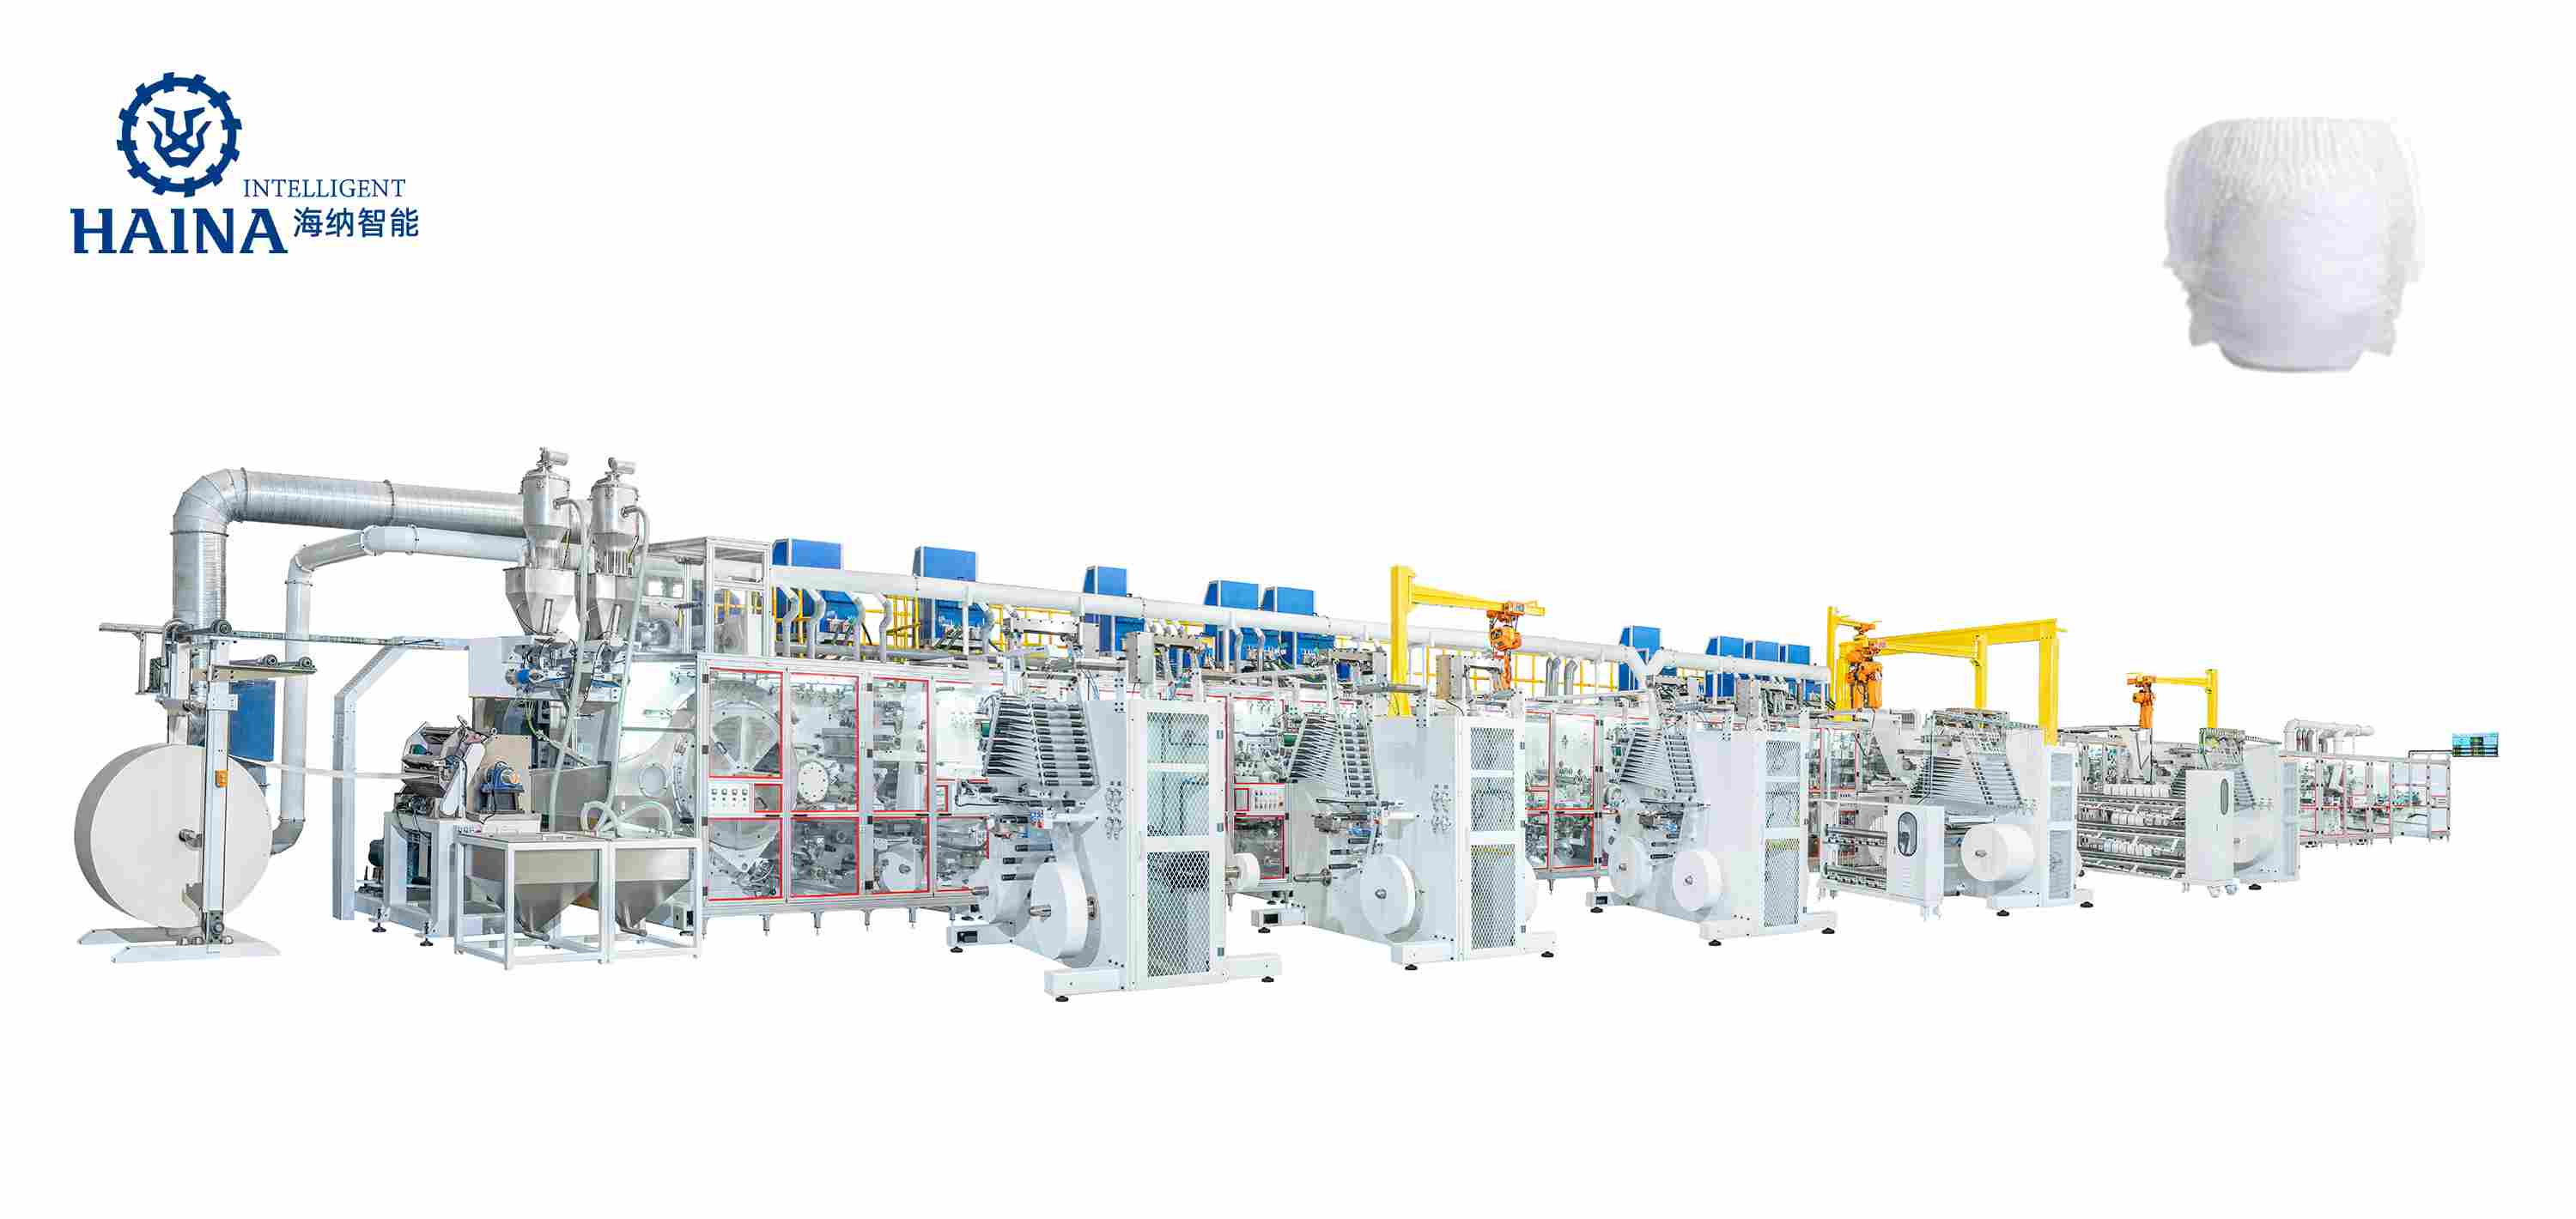
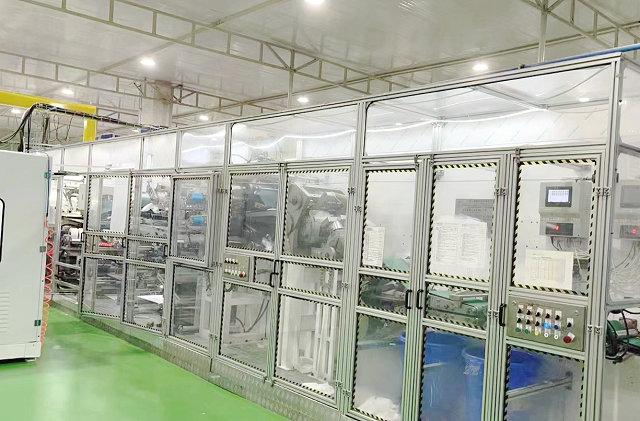
TK500 legacy dimensions are 30m*6m*3.8m. Design speed is 500ppm, while stable working speed is 400-450ppm. The recorded Rejection Rate is ≤4% and Efficiency is ≥85%. The utility record states Power Source 380V,50HZ and Air Pressure 0.6-0.8Mpa. It separately lists Machine Capacity 290KW and Machine Weight 75 tons.
Item
Legacy value
FAT confirmation
Design speed
500 ppm
Identify this as a design reference, not the acceptance output.
Stable working speed
400-450 ppm
Run the approved size and named material lots.
Rejection rate
Not more than 4%
Agree the reject categories and counting interval.
Efficiency
At least 85%
Define planned time, excluded stops and the calculation formula.
Machine size
30 m x 6 m x 3.8 m
Check final layout and service clearances.
Utilities
380 V, 50 Hz; 290 kW; 0.6-0.8 MPa air
Confirm destination supply and final connected load.
Weight
75 tons
Confirm foundation and lifting plan.
Witness the process, not only the counter
The earliest TK500 description names unwinding, tension control, embossing, perforation and folding under programmable logic control. During FAT, the team should observe material tracking and the finished diaper at each relevant transition. A speed display is useful only when retained samples show that core position, cuff formation, ear placement and fold remain within the signed product criteria.
01 Record start and stop times for the stable run.
02 Keep samples from start-up, steady running and every splice.
03 Separate process rejects from pack-handling losses.
04 Log alarms, operator action and recovery time.
Use the actual material set
The recorded bill of materials includes hydrophilic topsheet, hydrophobic leg-cuff nonwoven, leg-cuff elastic, ADL, fluff pulp, SAP, upper and lower tissue or nonwoven, PE film, laminating nonwoven, frontal tape, large-ear elastic nonwoven, small-ear nonwoven, magic side tape and three adhesive functions. FAT should use approved production grades or clearly document every substitute. A substitute lot can change tension, registration, bonding and waste behavior.
Test alarms and safe intervention
The legacy page states that the machine has an automatic alarm system. The acceptance script should therefore create agreed, safe fault conditions and record the alarm message, machine response, operator instruction and restart result. Safety checks must follow the signed machine documentation and must not require bypassing a guard or interlock.
Close FAT with a handover file
Acceptance evidence should include the signed product sample, material-lot list, recipe identity, speed and efficiency worksheet, reject log, alarm record, measured samples, open-item register and training attendance. Any optional packaging boundary should be written into the same file. This keeps later commissioning tied to what was actually witnessed.
TK500 FAT questions
Is 500 ppm the guaranteed production result?
No. The legacy data labels 500 ppm as design speed and 400-450 ppm as stable working speed. The signed FAT must define the accepted rate, product, materials, duration and downstream boundary.
Which materials should the supplier prepare?
Use the buyer-approved grades and lots for the recorded diaper construction. If a substitute is unavoidable, identify it in the report and do not treat its behavior as proof for an untested production material.
How should the 85% efficiency value be checked?
Write the formula before testing. Planned time, changeovers, material splices, supplier-caused stops, buyer-caused stops and rejected pieces need explicit treatment so both sides calculate the same result.
T-Shape Ear Type Baby Diaper Machine
Dimensions(L×W×H8)
30m*6m*3.8m
Design Speed:
500ppm
Stable Working Speed:
400-450ppm
Rejection Rate:
≤4%
Efficiency:
≥85%
Power Source:
380V,50HZ
Machine Capacity:
290KW
Air Pressure:
0.6-0.8Mpa
Machine Weight:
75 tons
Strengthen the ability and quality of the operators of Baby Diaper Machine
1. The technical level of maintenance personnel is an important factor affecting the maintenance efficiency of Baby Diaper Machine.
Having a high-quality workforce is the basis for promoting the continuous improvement of equipment maintenance efficiency.
2. The improvement of the technical level of the maintenance personnel of baby diaper Production Line can be carried out in the following ways:
First, take a combination of bringing in and sending out. Second, through internal training and learning, cultivate equipment management, use and maintenance personnel, and use business time to hold equipment use training activities to continuously improve the technical level of personnel. Third, strengthen the improvement of the employee assessment mechanism, increase the assessment of the survival of the fittest, stimulate the enthusiasm of the employees, and also promote the continuous learning of the employees, providing necessary guarantees for the use and maintenance of equipment.
We back our machines with acomprehensive 1-year warranty for your peace of mind.
Innovation
We continue improving and innovating, never stop.
TK500 fully automatic baby diaper machine Manufacturing Process
Designing a machine that meets your requirements.
The first phase for each project is designing the machine. During this period, our engineers and project manager will work with you closely, understanding the product specification, raw materials used, and the expected functions of the TK500 fully automatic baby diaper machine.
Purchasing parts and practising quality control.
After the machine design is confirmed with our client, our project manager will work with the procurement department for the purchase of parts and components used in the machine. All purchased components have to go through testings within the quality control department. Our staff make sure that each part is of the exact same quality and size as indicated on the machine design.
Assembling the whole machine
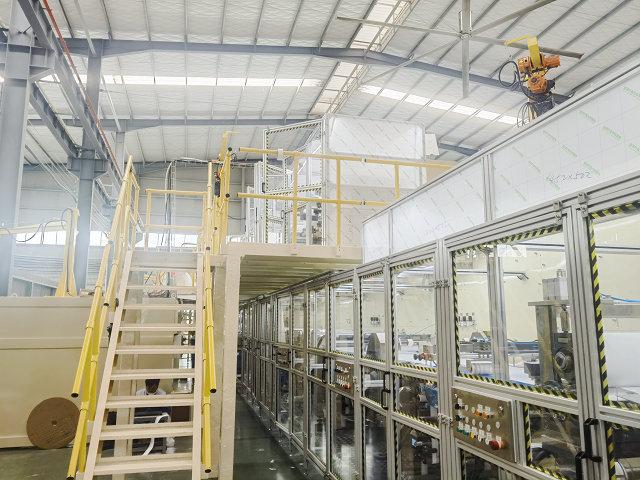
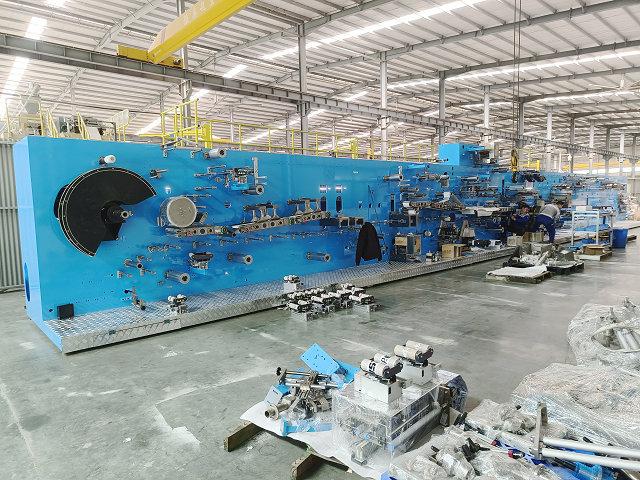
During this period, our staff at the assembly facility will assemble the TK500 fully automatic baby diaper machine according to machine drawing.
Calibrating the machine
After assemble of the whole machine, we will calibrate the TK500 fully automatic baby diaper machine and put it into trial operation. We start from setting standards of production speed,stability and product performance. Then we start the machine and test its actual performance. Our engineers and technicians will work together on the calibration and modification to meet our clients' demands.
Delivering the machine
After calibrating the machine inside our factory, we will then request the client in our facility to confirm the machine performance. Only when our client approves on the machine will we arrange the delivery.After the TK500 fully automatic baby diaper machine has reached the client's destination, technicians will be assigned on site, taking care of the assemble and calibration.
TK500 fully automatic baby diaper machine Related Services
Quality Guarantee
CNC finishing and work with famous brands.
Fast service
We concern what you concern.
One Year Warranty
We back our machines with acomprehensive 1-year warranty for your peace of mind.
Innovation
We continue improving and innovating, never stop.
1. Remote monitoring and diagnostics
With advanced technology, we offer remote monitoring and diagnostics services, allowing us to detect and resolve issues with your diaper machine remotely, saving you time and resources.
2. Efficiency analysis and improvement
We analyze your production process to identify bottlenecks and inefficiencies, providing recommendations for improvement to optimize your diaper machine's performance.
3. Preventive maintenance
Regular maintenance is crucial for the smooth operation of your diaper machine. Our service includes scheduled inspections and maintenance to prevent breakdowns.
The Baby Diaper machine's flexibility allows us to customize diaper designs according to market trends, giving us a competitive edge. Our customers appreciate the variety.
the efficiency of the Baby Diaper Machine
Matthew2024-05-30
Our operational costs have decreased significantly, thanks to the efficiency of the Baby Diaper Machine. It's a cost-effective solution for any diaper manufacturer.
using the Baby Diaper Machine
Liam2024-05-30
We've seen a significant improvement in production output and product quality since we started using the Baby Diaper Machine. Our customers love the result!
Baby Diaper machine softness and snug fit
Jack2024-05-30
We've received positive feedback from parents who love the softness and snug fit of the diapers produced by this Baby Diaper machine. It's a win-win for everyone.
Start Customizing Your Machines Now!
Contact US
Manufacturer Address:222 Qiantong Road, Anhai Town, Jinjiang City, Fujian Province, China
Sale Tel: +86-17750870135
MP/Whatapp: +86-17750870135
Email: marketing@fjhaina.com






The Baby Diaper machine's flexibility allows us to customize diaper designs according to market trends, giving us a competitive edge. Our customers appreciate the variety.Carter 2024-05-30
Our operational costs have decreased significantly, thanks to the efficiency of the Baby Diaper Machine. It's a cost-effective solution for any diaper manufacturer.Matthew 2024-05-30
We've seen a significant improvement in production output and product quality since we started using the Baby Diaper Machine. Our customers love the result!Liam 2024-05-30
We've received positive feedback from parents who love the softness and snug fit of the diapers produced by this Baby Diaper machine. It's a win-win for everyone.Jack 2024-05-30